Soil powder pneumatic conveying systems represent a sophisticated technology designed to transport dry powders, including soil and other fine particulate materials, through a pressurized or vacuum pipeline. The core principle of these systems involves the use of air or gas to move material from a source to a destination, eliminating the need for mechanical components like belts or buckets that are common in traditional bulk material handling. This method is particularly advantageous for materials that are dusty, hygroscopic, or require a dust-free environment during transport.
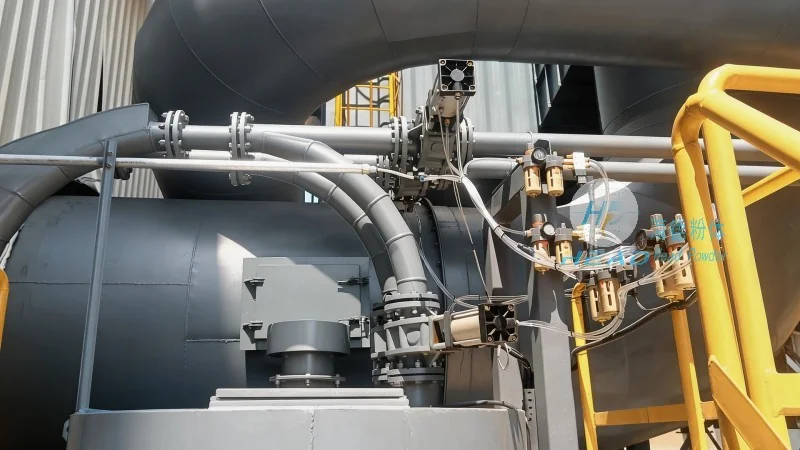
Key Working Principles of Pneumatic Conveying
The operation of a soil powder pneumatic conveying system is based on the fundamental physics of fluid dynamics. In a typical system, the material is introduced into a hopper or feeder, where it is then drawn into a pipeline by a fan or blower. The air flow, which can be either positive pressure (where air is forced into the system) or negative pressure (where air is drawn out), creates a flow that carries the powder particles along the pipeline. The velocity of the air must be sufficient to overcome the gravitational and frictional forces acting on the particles, ensuring stable and efficient transport. The system typically includes components such as a feeder, a pipeline network, a receiver, and a control unit to regulate the flow and pressure. The choice between positive and negative pressure systems depends on factors like the distance to be covered, the material characteristics, and the desired level of dust control.
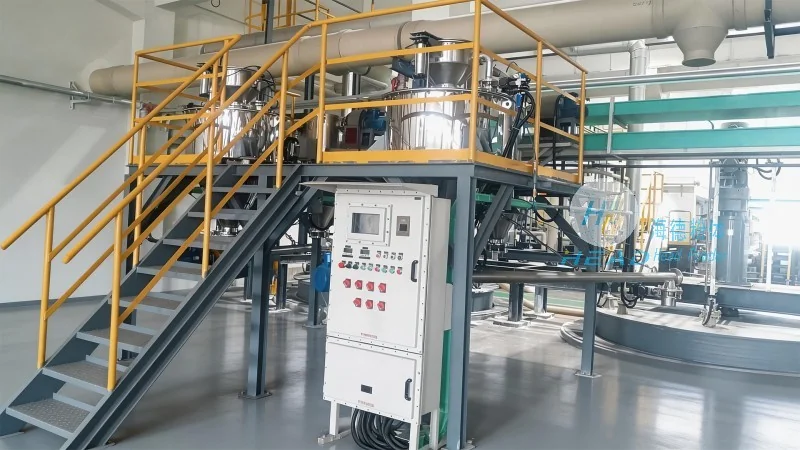
Advantages of Pneumatic Conveying for Soil Powder Handling
When applied to soil powder handling, pneumatic conveying systems offer several key advantages over alternative methods. Firstly, they provide a dust-free transport environment, which is critical for maintaining material quality and ensuring compliance with environmental regulations. Unlike mechanical systems that can generate significant dust, pneumatic conveyors keep the material enclosed within the pipeline, reducing airborne particulate emissions. Secondly, these systems are highly flexible, allowing for the integration of multiple feeding and receiving points. This flexibility is particularly beneficial in construction and mining sites where materials need to be transported between various locations. Thirdly, pneumatic conveying can handle a wide range of particle sizes and moisture contents, making it suitable for diverse soil types. The system's ability to operate under both positive and negative pressure also provides adaptability for different application scenarios, such as transporting soil from a storage silo to a processing plant or from a construction site to a disposal area.
Typical Working Scenarios and Applications
Soil powder pneumatic conveying systems are widely used in various industrial and construction applications. One common scenario is in the construction industry, where soil is transported from excavation sites to processing facilities or disposal areas. The ability to handle large volumes of soil efficiently and with minimal labor makes this system ideal for large-scale construction projects. Another application is in the mining sector, where soil and other fine minerals are conveyed from processing plants to storage or shipping locations. The system's capacity to operate in harsh environments, such as those with high dust levels or extreme temperatures, further enhances its suitability for mining operations. Additionally, in environmental remediation projects, pneumatic conveying is used to transport contaminated soil to treatment facilities, ensuring that the material is handled safely and without contaminating the surrounding area. The versatility of these systems also makes them applicable in agricultural settings, where soil samples or fertilizer powders are transported between fields and processing units.
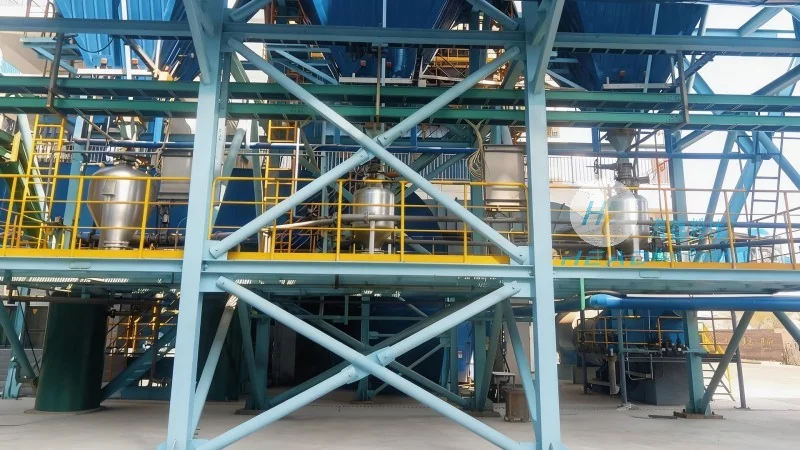
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the professional provider of soil powder pneumatic conveying solutions, is a leading company based in Shandong, China. With a strong commitment to innovation and quality, HeadPowder specializes in designing, manufacturing, and installing advanced pneumatic conveying systems tailored to the specific needs of soil and powder handling industries. The company's expertise lies in understanding the unique challenges of soil transport, such as material variability, dust control, and operational efficiency. By leveraging cutting-edge technology and extensive industry experience, HeadPowder delivers systems that meet the highest standards of performance and reliability. The company's team of engineers and technicians work closely with clients to develop customized solutions that optimize material flow, reduce operational costs, and enhance overall productivity. HeadPowder's dedication to customer satisfaction and technical excellence has established it as a trusted partner in the global market for soil powder handling equipment.




