Guargum powder, a vital industrial material utilized across food, pharmaceutical, and chemical sectors, demands efficient and reliable handling to preserve its quality and prevent contamination. Pneumatic conveying machines have become the preferred solution for transporting guargum powder due to their capability to handle fine powders with minimal product degradation. This article delves into the fundamental principles of guargum powder pneumatic conveying systems and highlights the specific working scene characteristics that make them suitable for diverse industrial applications.
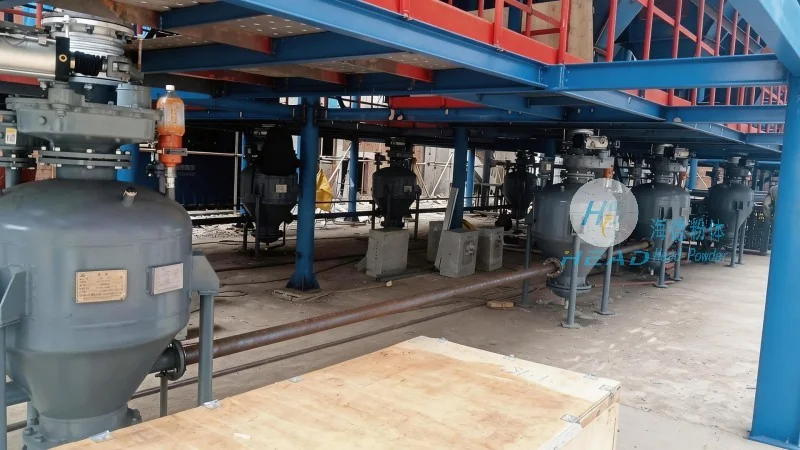
Principle of Pneumatic Conveying for Guargum Powder
The core principle of pneumatic conveying involves utilizing air or gas to transport solid materials through a pipeline. For guargum powder, which is typically fine and hygroscopic, the system must be engineered to minimize particle agglomeration and maintain consistent flow. Two primary types of pneumatic conveying systems exist: positive pressure and negative pressure. Positive pressure systems employ a blower to push air and material through the pipeline, while negative pressure systems use a vacuum to draw material into the system. Both systems are tailored to handle the unique properties of guargum powder, such as its low bulk density and tendency to form dust clouds. The design of the conveying line—including pipe diameter, material, and inlet/outlet placement—is critical to ensuring efficient and safe operation. For instance, the use of flexible hoses or rigid pipes with smooth interiors reduces friction and prevents material buildup, which is essential for maintaining the quality of guargum powder during transport.
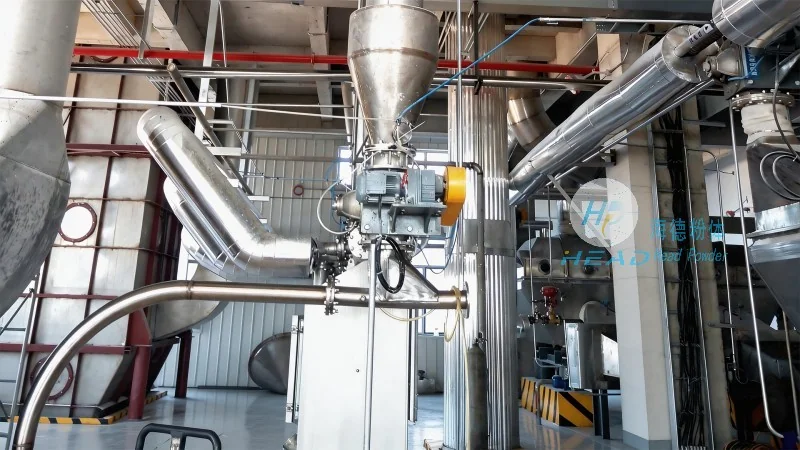
Working Scene Characteristics of Guargum Powder Pneumatic Conveying Machines
The working scene characteristics of guargum powder pneumatic conveying machines are customized to the specific needs of industrial environments where guargum powder is processed. These characteristics include high material transfer efficiency, low maintenance requirements, and the ability to handle large volumes with minimal human intervention. In food processing facilities, for example, the system must adhere to sanitary standards and be easy to clean to prevent cross-contamination. The use of stainless steel components and sealed systems ensures guargum powder remains free from contaminants, crucial for product safety. In chemical manufacturing plants, the system may need to handle more aggressive materials or higher temperatures, requiring specialized materials of construction and temperature-resistant components. The flexibility of pneumatic conveying systems also allows integration into existing production lines, reducing the need for major infrastructure changes. This adaptability makes them suitable for both new installations and retrofitting in existing facilities.
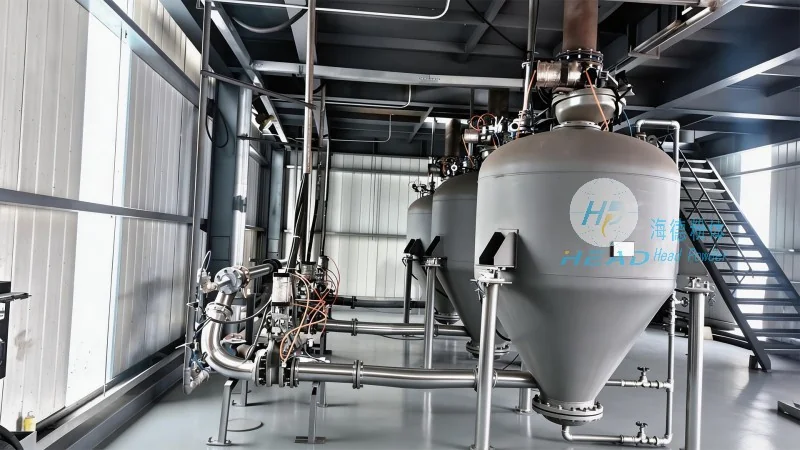
Application Scenarios and Operational Benefits
Guargum powder pneumatic conveying machines are deployed in various working scenes, each offering distinct operational benefits. In the food industry, these systems transport guargum powder from storage silos to mixing equipment, ensuring consistent feed rates and preventing clogging in downstream processes. Precise flow rate control helps maintain desired product consistency, vital for quality control. In the pharmaceutical industry, the sanitary design of the conveying system is paramount, as it must meet stringent regulatory requirements for product purity. Positive pressure systems with sealed containers prevent airborne contaminant ingress, ensuring guargum powder remains sterile and safe for drug formulations. In chemical applications, the system’s ability to handle abrasive or corrosive materials is advantageous, reducing equipment wear and extending component lifespan. Additionally, pneumatic conveying systems offer higher energy efficiency compared to traditional methods like bucket elevators or belt conveyors, making them a cost-effective solution for long-distance material transport.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading manufacturer of pneumatic conveying equipment specializing in solutions for handling fine powders such as guargum. With a focus on innovation and quality, the company designs and manufactures systems that meet the unique requirements of various industries. Headpowder’s facilities are located in Shandong, China, where the company leverages advanced engineering and manufacturing capabilities to produce reliable and efficient pneumatic conveying machines. The company’s commitment to customer satisfaction and product excellence has made it a trusted partner for businesses in the food, pharmaceutical, and chemical sectors, providing tailored solutions that enhance operational efficiency and product quality.




