HeadPowder, a leading manufacturer based in Shandong, China, specializes in industrial equipment designed for efficient material handling. Among their product lineup is the cocoa powder pneumatic conveying machine, a critical solution for processing and transporting cocoa powder in various industrial applications. This article explores the fundamental principles behind this technology and highlights the key working scene characteristics that make it an ideal choice for cocoa powder handling operations.
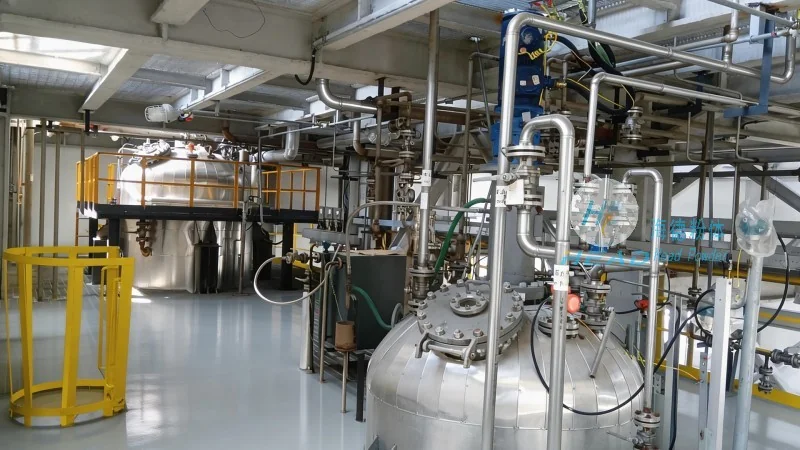
The Core Principle of Pneumatic Conveying for Cocoa Powder
The pneumatic conveying machine operates on the principle of using compressed air to transport solid materials like cocoa powder through a pipeline system. Unlike traditional mechanical conveyors, this method eliminates the need for moving parts in contact with the material, reducing wear and tear and minimizing the risk of contamination. The process typically involves a hopper where cocoa powder is stored, a blower or compressor that generates the air flow, and a pipeline network that directs the material to its destination. As the air flows through the pipeline, it creates a low-pressure zone that draws the cocoa powder particles into the stream, allowing them to be carried to the desired location. This mechanism ensures a consistent and controlled flow of cocoa powder, which is essential for maintaining product quality and preventing caking or agglomeration.
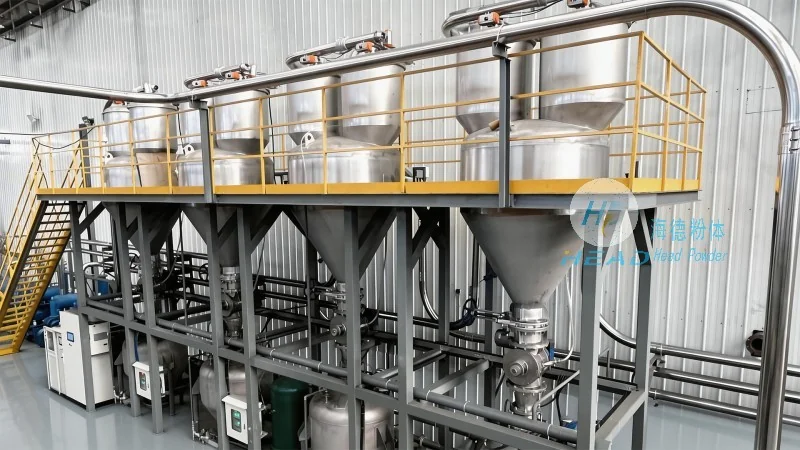
Key Working Scene Characteristics of Cocoa Powder Pneumatic Conveying Machines
When considering the application of a cocoa powder pneumatic conveying machine, several working scene characteristics are crucial for optimizing performance and ensuring operational efficiency. First, the system's ability to handle fine powders without clogging is a significant advantage. Cocoa powder is a fine, particulate material that can easily block traditional conveyors, but the pneumatic system's air flow design prevents such issues, ensuring continuous operation. Second, the machine's flexibility in terms of layout and integration is another key characteristic. It can be easily adapted to existing production lines, allowing for modular installation and expansion as production needs change. Third, the hygienic design of the equipment is vital in food processing industries, where cocoa powder is often used in confectionery and beverage production. The smooth, non-porous surfaces and easy-to-clean components of the pneumatic conveying machine meet stringent hygiene standards, reducing the risk of microbial contamination and ensuring compliance with food safety regulations. Additionally, the system's energy efficiency is a notable characteristic, as it uses compressed air to transport materials with minimal energy consumption compared to other methods like belt conveyors or bucket elevators.
Applications and Operational Scenarios
The working scene characteristics of cocoa powder pneumatic conveying machines make them suitable for a wide range of operational scenarios. In chocolate manufacturing plants, for example, these machines are used to transport cocoa powder from storage silos to mixing and processing areas. The consistent flow and hygienic design ensure that the cocoa powder remains in optimal condition, preserving its flavor and texture. In food processing facilities, the system can be integrated into automated production lines, where it works in conjunction with other equipment like mixers and extruders to streamline the production process. The flexibility of the pipeline network allows for the conveyance of cocoa powder to multiple destinations, such as packaging lines or quality control stations, without the need for manual handling. Furthermore, in research and development laboratories, the pneumatic conveying machine is used to transport small quantities of cocoa powder for testing and analysis, providing a precise and controlled method for material handling. These operational scenarios demonstrate the versatility and reliability of the cocoa powder pneumatic conveying machine in various industrial settings.
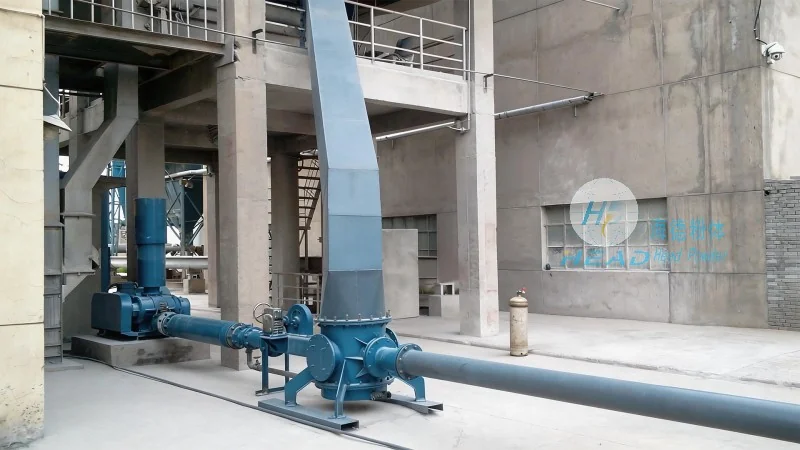
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers advanced pneumatic conveying solutions tailored to the specific needs of cocoa powder handling. By leveraging the core principles of pneumatic transport and incorporating key working scene characteristics, their machines provide efficient, hygienic, and reliable material handling for cocoa powder applications. The company's commitment to quality and innovation ensures that their products meet the highest standards in the industry, making them a trusted partner for businesses in the food processing sector. Whether for large-scale production or laboratory use, the cocoa powder pneumatic conveying machine from HeadPowder is designed to enhance operational efficiency and maintain product quality, supporting the success of industrial operations worldwide.




