For industrial applications involving the handling of coal ash particles, efficient and reliable material transport is crucial. This is where the coal ash particle pneumatic conveying system comes into play, offering a solution that combines technology and engineering to ensure smooth material movement. In this article, we will explore what this system entails and delve into its design principles, providing a comprehensive understanding of its functionality and importance in modern industrial processes.
Understanding the Coal Ash Particle Pneumatic Conveying System
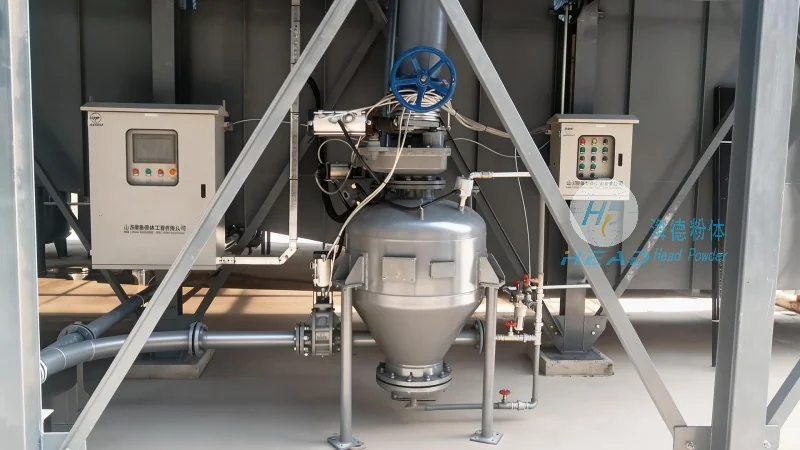
The coal ash particle pneumatic conveying system is a specialized equipment designed to transport coal ash particles through a pipeline using air as the conveying medium. This method is widely adopted in various industrial sectors due to its ability to handle bulk materials with minimal human intervention and reduced risk of contamination. The system operates by creating a pressure differential within the pipeline, which propels the coal ash particles along the path of least resistance, ensuring efficient and continuous material transport from the source to the destination.
Design Principles of the Coal Ash Particle Pneumatic Conveying System
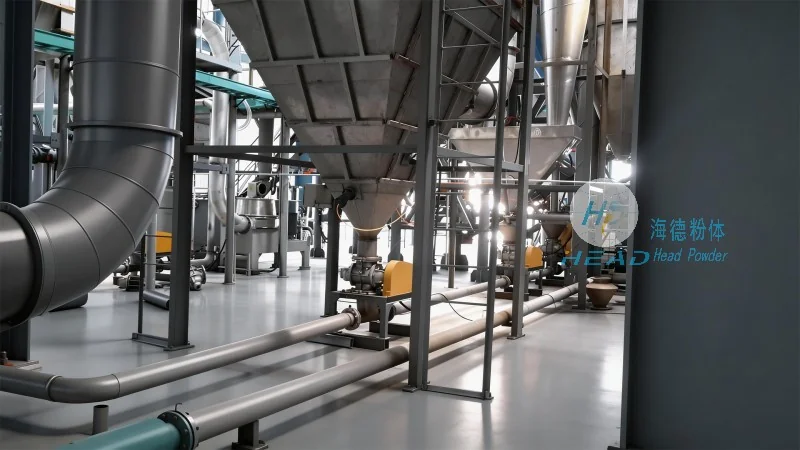
The design of a coal ash particle pneumatic conveying system is based on several key principles that ensure optimal performance and reliability. These principles include the selection of appropriate air flow rates, pipeline dimensions, and material handling capabilities. Engineers must consider factors such as particle size, density, and moisture content of the coal ash, as these characteristics directly impact the system's efficiency. The system typically consists of a blower or compressor to generate the necessary air pressure, a hopper to store the coal ash, and a pipeline network that connects the source to the processing or disposal site. The design also incorporates features like air locks and cyclones to separate the coal ash from the air stream, ensuring that the material is delivered to the target location without loss or contamination.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of industrial conveying solutions. With a focus on innovation and customer satisfaction, the company specializes in designing and manufacturing pneumatic conveying systems tailored to the unique needs of various industries. HeadPowder's expertise lies in understanding the specific requirements of materials like coal ash, ensuring that their systems are optimized for efficiency, durability, and safety. The company's headquarters is located in Shandong, China, where it leverages advanced technology and engineering expertise to deliver high-quality solutions to clients worldwide.
Benefits and Applications of the Coal Ash Particle Pneumatic Conveying System
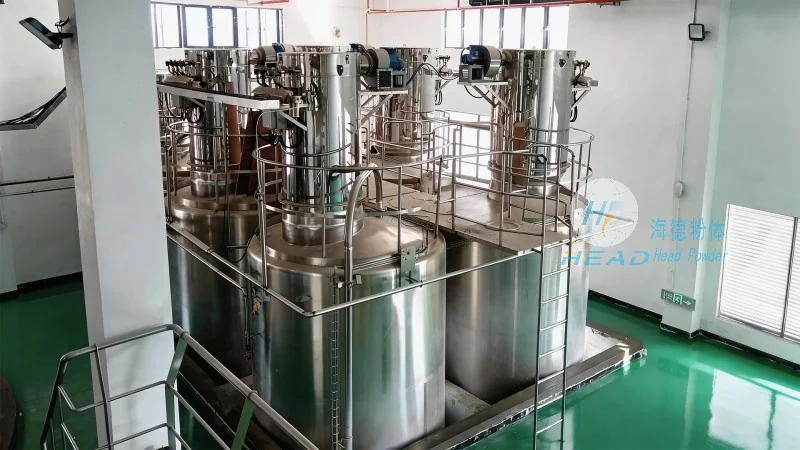
The coal ash particle pneumatic conveying system offers numerous benefits that make it an ideal choice for industrial applications. These benefits include reduced labor costs, minimized material handling time, and improved safety by eliminating the need for manual handling of bulk materials. The system is also highly adaptable, capable of handling a wide range of particle sizes and material types. Its applications span across various industries, including power generation, cement production, and waste management, where the efficient transport of coal ash is essential for operational efficiency and environmental compliance. By leveraging the design principles and advanced technology, the system ensures consistent performance and reliability, contributing to the overall productivity and sustainability of industrial processes.




