Phosphate rock powder, as a key raw material in the fertilizer and chemical industries, often presents unique handling challenges due to its fine particle size and potential for dust generation. Traditional bulk material handling methods may struggle with the efficiency, safety, and environmental compliance required for modern production lines. This is where a specialized solution—phosphate rock powder pneumatic conveying systems—comes into play, offering a reliable and efficient means to transport these materials over long distances and within complex industrial setups.
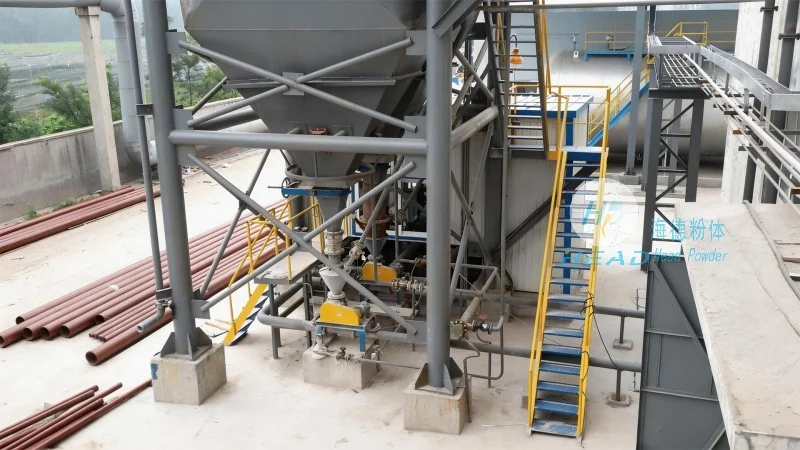
Understanding the Phosphate Rock Powder Pneumatic Conveying System
At its core, a phosphate rock powder pneumatic conveying system is a technology designed to transport dry, fine powders like phosphate rock through a pipeline using air or gas as the conveying medium. Unlike mechanical conveyors that rely on physical components like belts or screws, pneumatic systems utilize the kinetic energy of the moving air to carry the powder particles. This method is particularly advantageous for materials that are prone to caking, agglomeration, or are sensitive to moisture, as it minimizes direct contact with equipment and reduces the risk of material degradation.
The Fundamental Design Principles of the System
The design of a phosphate rock powder pneumatic conveying system is governed by several key principles that ensure optimal performance, efficiency, and safety. The primary principle is the selection of the appropriate conveying method—either positive pressure (where air is blown into the system to push the material) or negative pressure (where air is drawn out to pull the material). The choice between these two depends on factors such as the distance of transport, the volume of material, and the need for dust control. For long-distance or high-volume applications, positive pressure systems are often preferred due to their ability to maintain consistent flow rates and handle larger quantities of material.
A critical component of the system is the feed mechanism, which ensures that the phosphate rock powder is introduced into the pipeline without causing blockages or uneven flow. This typically involves a hopper with a rotary valve or a screw feeder that can control the flow rate precisely. The feeder must be designed to handle the specific characteristics of the powder, such as its bulk density and flowability, to prevent issues like bridging or segregation.
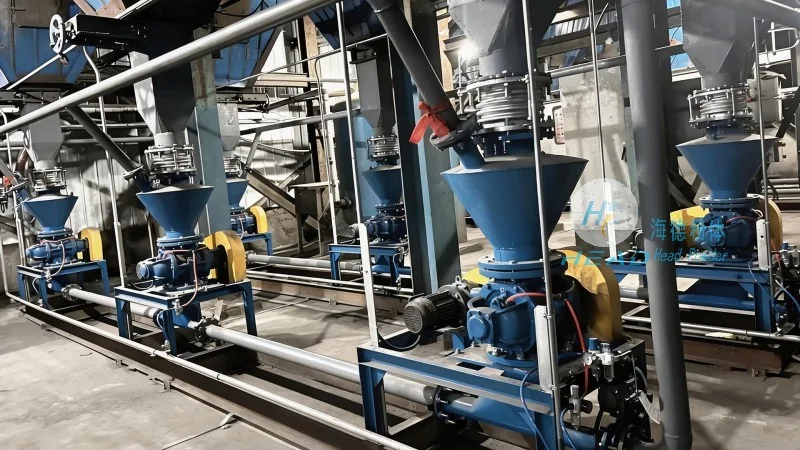
The pipeline itself is another key design element. It must be constructed from materials that are resistant to corrosion and abrasion, as phosphate rock powder can be chemically aggressive and abrasive over time. Stainless steel or special alloys are commonly used for this purpose. The pipeline layout is also carefully planned to minimize pressure drops and ensure smooth material flow. Elbows, bends, and other fittings are strategically placed to maintain the air-powder mixture's velocity and prevent settling or clogging.
Downstream of the pipeline, the system includes separation and collection equipment. This typically involves a cyclone separator, which uses centrifugal force to separate the powder from the air stream. The separated powder is then collected in a hopper or silo, while the cleaned air is either vented to the atmosphere or recirculated back into the system to improve energy efficiency. The design of the separator must be optimized for the specific particle size and density of the phosphate rock powder to achieve high separation efficiency and minimize dust emissions.
Key Features and Benefits of the System
Implementing a phosphate rock powder pneumatic conveying system offers several significant advantages for industrial operations. First and foremost, it enhances safety by eliminating the need for manual handling of powders, reducing the risk of dust explosions and respiratory hazards. The enclosed system also minimizes environmental impact by containing dust and preventing it from escaping into the workplace or the surrounding environment.
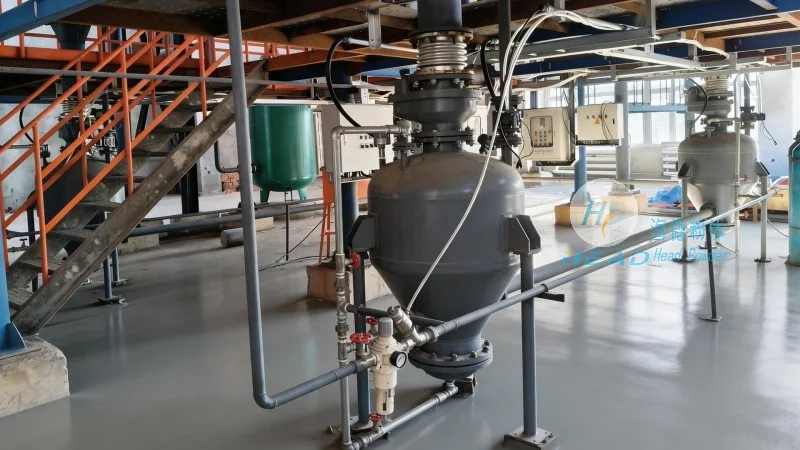
From an operational perspective, pneumatic conveying systems provide high efficiency and flexibility. They can transport materials over long distances (up to several kilometers) and through complex layouts, including vertical lifts and multiple branches, without the need for additional mechanical components. This flexibility allows for integration into existing production lines or the design of new facilities with optimal material flow paths.
Energy efficiency is another key benefit. By recycling the air used in the conveying process, systems can reduce energy consumption compared to traditional methods. Additionally, the absence of moving parts in the pipeline (except for the feed mechanism) reduces maintenance requirements and extends the lifespan of the equipment. This leads to lower operational costs and increased reliability over time.
Application in the Phosphate Industry
Phosphate rock is a fundamental component in the production of fertilizers, particularly phosphates like DAP (diammonium phosphate) and MAP (mon ammonium phosphate). The efficient handling of phosphate rock powder is critical to the overall productivity of these processes. A well-designed pneumatic conveying system ensures that raw materials are delivered to processing units in a consistent and controlled manner, which is essential for maintaining product quality and production rates.
In addition to fertilizer production, phosphate rock powder is also used in other industries, such as animal feed and specialty chemicals. The versatility of pneumatic conveying systems makes them suitable for a wide range of applications, from small-scale processing plants to large-scale industrial facilities. The ability to handle varying material characteristics and flow rates makes these systems adaptable to different production needs.
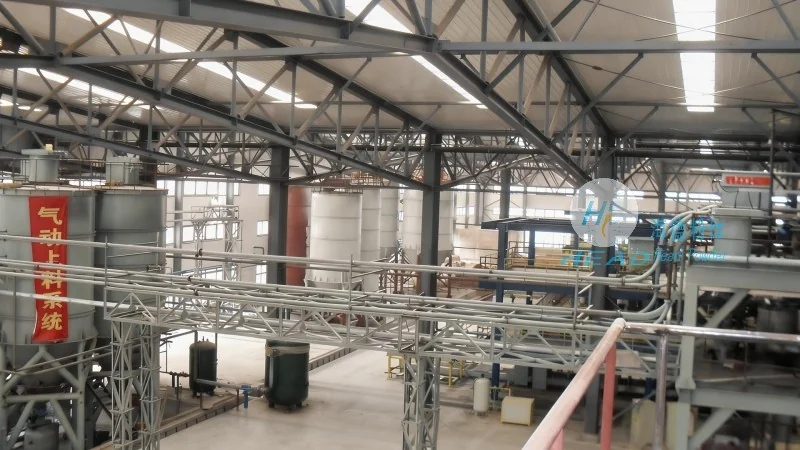
Case Study: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing phosphate rock powder pneumatic conveying systems tailored to the specific needs of the fertilizer and chemical industries. With a focus on innovation and customer satisfaction, the company has developed advanced systems that incorporate the latest technology in pneumatic conveying, ensuring optimal performance and reliability.
The company’s expertise lies in understanding the unique challenges of handling phosphate rock powder and translating them into effective solutions. By leveraging years of experience and a deep understanding of material science, HeadPowder engineers design systems that are not only efficient but also safe and environmentally friendly. Their systems are built to meet the highest standards of quality and durability, with components selected to withstand the corrosive and abrasive nature of the material.
HeadPowder’s commitment to customer service extends beyond the initial design and installation. The company provides comprehensive support, including maintenance, troubleshooting, and technical assistance, to ensure that the systems operate at peak performance throughout their lifecycle. This approach has earned the company a reputation for excellence in the industry, with clients relying on their expertise to enhance their production processes and improve overall efficiency.




