

Airborne Conveying Systems Effectively Resolve Quartz Powder Conveying Challenges
When it comes to transporting quartz powder, traditional methods often face significant challenges such as dust pollution, material loss, and operational inefficiencies. The quartz powder industry requires reliable and efficient material handling solutions to maintain production quality and operational safety. Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized engineering solutions, has developed advanced airborne conveying systems tailored to address these specific challenges in quartz powder handling.
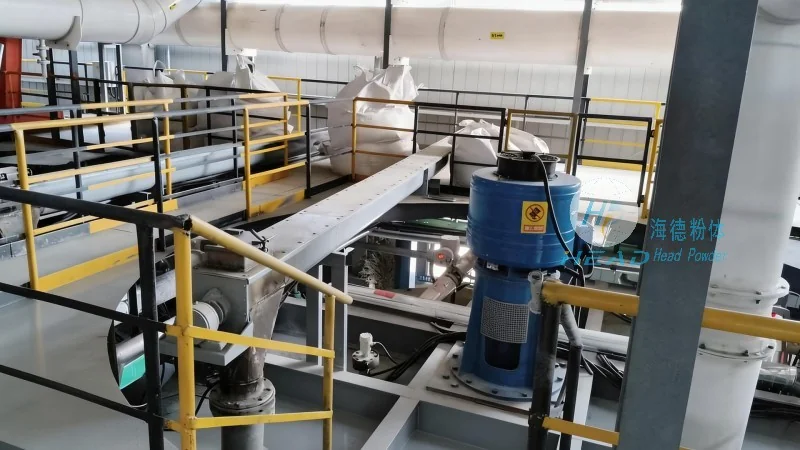
Understanding the Unique Requirements of Quartz Powder Conveying
Quartz powder, with its fine particle size and abrasive properties, demands specialized handling equipment that can minimize material degradation and ensure consistent flow. Conventional conveyor systems may struggle with the high dust generation and potential blockages that quartz powder presents. The airborne conveying technology, also known as pneumatic conveying, offers a superior alternative by utilizing air pressure to transport materials in a closed system, effectively controlling dust and maintaining material integrity throughout the process.
Key Features of HeadPowder's Airborne Conveying Systems
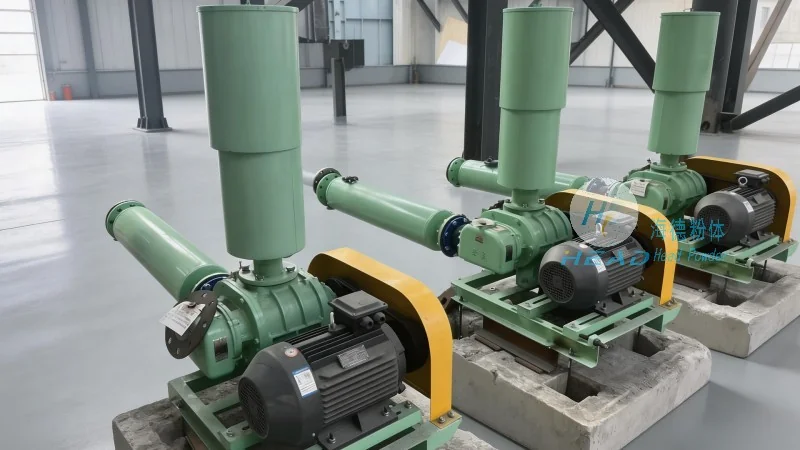
HeadPowder's airborne conveying systems are engineered with precision to meet the demanding requirements of quartz powder transportation. The systems incorporate advanced components including high-efficiency blowers, specialized pipelines, and intelligent control systems that ensure smooth and continuous material flow. Key features include: high material transport capacity, minimal dust emission, low maintenance requirements, and versatile system configurations that can be customized to fit specific production layouts. The use of durable materials in construction ensures long-term reliability even under harsh operating conditions typical of quartz powder processing facilities.
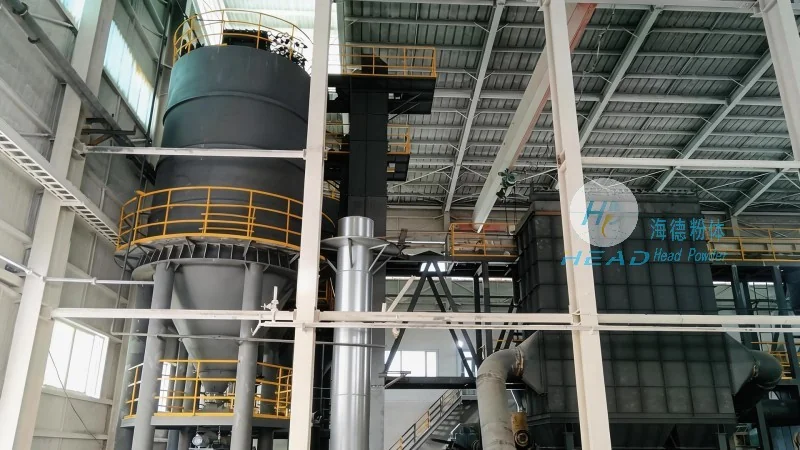
How the System Improves Production Efficiency and Safety
The implementation of airborne conveying systems in quartz powder production lines leads to substantial improvements in both operational efficiency and workplace safety. By eliminating the need for manual handling and open-air transport, the systems significantly reduce the risk of dust-related health hazards and material spillage. The automated control features allow for precise material dosing and flow regulation, minimizing waste and optimizing production output. Additionally, the closed-loop design prevents environmental contamination, aligning with modern industrial standards for sustainable operations. These benefits translate into lower operational costs and enhanced overall productivity for quartz powder manufacturers.
Customization and Integration Capabilities
Recognizing that each quartz powder production facility has unique operational needs, HeadPowder offers comprehensive customization and integration services for its airborne conveying systems. The company works closely with clients to design systems that seamlessly integrate with existing production lines, ensuring minimal disruption during installation and operation. Whether for bulk material transport between processing stages or precise feeding into downstream equipment, the systems can be configured to handle varying particle sizes and flow rates. The modular design allows for easy expansion or modification as production scales up, providing long-term investment value. Technical support and after-sales service are also provided to ensure optimal system performance and quick resolution of any operational issues.
Case Studies and Industry Validation
HeadPowder's airborne conveying systems have been successfully implemented in numerous quartz powder processing plants across China and other regions. These real-world applications have demonstrated consistent performance in improving material handling efficiency and reducing operational risks. Clients have reported significant reductions in dust emissions, lower material loss rates, and increased production throughput after adopting the systems. The positive feedback from industry partners underscores the effectiveness of HeadPowder's engineering solutions in addressing the specific challenges of quartz powder transportation. The company's commitment to continuous improvement and customer satisfaction has established it as a trusted partner in the quartz powder processing industry.
Conclusion: Choosing the Right Solution for Quartz Powder Handling
For quartz powder manufacturers seeking reliable and efficient material handling solutions, the airborne conveying systems from Shandong HeadPowder Engineering Co., Ltd. represent a superior choice. By combining advanced technology with practical engineering expertise, these systems provide the performance and reliability needed to enhance production efficiency and ensure workplace safety. With a focus on customization and long-term partnership, HeadPowder is positioned to deliver tailored solutions that meet the evolving needs of the quartz powder industry. The adoption of such systems not only addresses current operational challenges but also supports sustainable and competitive manufacturing practices in the global market.