At Shandong HeadPowder Engineering Co., Ltd., we specialize in industrial equipment designed for efficient material handling. One of our key products is the diatomite mineral powder pneumatic conveyor, a system engineered to transport fine powders like diatomite with precision and reliability. This article explores the functionality and design principles behind this advanced pneumatic conveying system.
Understanding Pneumatic Conveying Technology
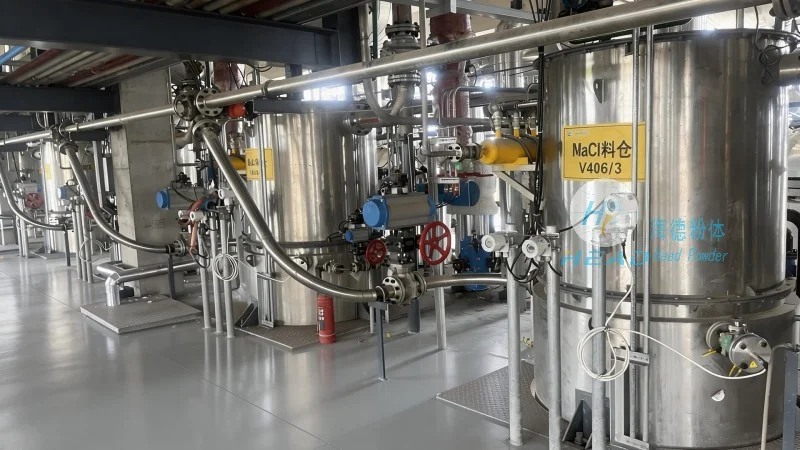
Pneumatic conveying is a method of transporting bulk materials through a pipeline using air or other gases. Unlike mechanical systems that rely on belts or screws, pneumatic conveyors use pressure differentials to move powders, making them ideal for handling delicate materials such as diatomite. The diatomite mineral powder pneumatic conveyor, in particular, is optimized for the unique properties of diatomite, which is a lightweight, porous sedimentary rock commonly used in filtration, insulation, and other industrial applications.
Key Design Principles of the Conveyor System
The design of a diatomite mineral powder pneumatic conveyor involves several critical principles to ensure optimal performance. First, the system must maintain consistent air pressure and flow rates to prevent material degradation or blockages. The pipeline design, including the use of smooth, corrosion-resistant materials, minimizes friction and ensures that diatomite particles move smoothly without clogging. Additionally, the system incorporates features like airlocks and cyclones to separate the conveyed material from the air stream, ensuring efficient collection and minimal loss.
Components and Operational Mechanism
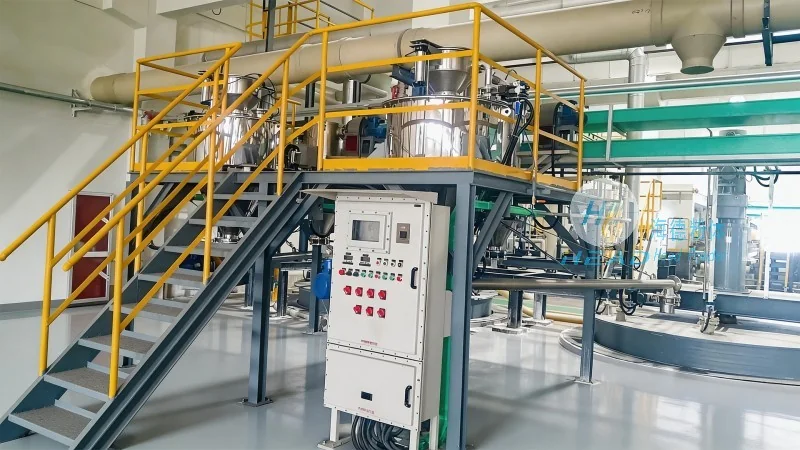
The diatomite mineral powder pneumatic conveyor consists of several key components, each playing a vital role in the overall operation. The feed hopper is responsible for introducing the diatomite powder into the system, while the air compressor generates the necessary pressure to move the material through the pipeline. The pipeline itself is typically made of stainless steel or other durable materials to withstand the abrasive nature of diatomite particles. At the discharge end, a separator or filter removes the powder from the air, allowing the air to be recirculated or vented safely. The entire system is controlled by a programmable logic controller (PLC), which monitors pressure, flow, and other parameters to maintain consistent performance.
Advantages of Using a Diatomite Mineral Powder Pneumatic Conveyor
Implementing a diatomite mineral powder pneumatic conveyor offers several advantages over traditional mechanical conveying methods. First, it eliminates the need for moving parts in the conveying line, reducing maintenance requirements and extending the system's lifespan. The system is also highly flexible, allowing for changes in material flow rates or pipeline layout without major modifications. Additionally, pneumatic conveyors are more hygienic and easier to clean, making them suitable for applications where material purity is critical, such as in food or pharmaceutical processing. For diatomite, which is often used in filtration applications, maintaining a clean and dust-free environment is essential, and the pneumatic conveyor helps achieve this by minimizing particle dispersion.
Applications and Industry Use Cases
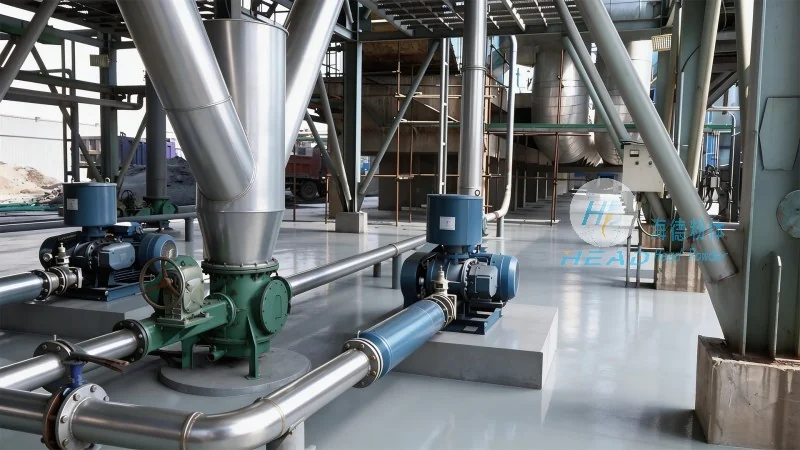
Diatomite mineral powder pneumatic conveyors are widely used in various industries where diatomite is processed or utilized. In the filtration industry, for example, these systems transport diatomite to filter beds or storage tanks, ensuring a consistent supply of material for water treatment or industrial filtration processes. In the construction industry, diatomite is used as an insulating material, and the pneumatic conveyor facilitates its transport from storage to mixing or application sites. Additionally, in the chemical and pharmaceutical sectors, diatomite is used as a filler or absorbent, and the conveyor system ensures that the material is handled safely and efficiently, minimizing dust exposure and improving workplace safety.
Conclusion and Company Expertise
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of diatomite mineral powder pneumatic conveyors, leveraging years of experience in industrial material handling to design and produce high-quality equipment. Our systems are engineered to meet the specific needs of diatomite processing, combining advanced pneumatic technology with robust design to ensure reliable and efficient operation. Whether for filtration, insulation, or other applications, our diatomite mineral powder pneumatic conveyors provide a cost-effective and sustainable solution for transporting fine powders. With our commitment to quality and customer satisfaction, we continue to be a trusted partner for businesses seeking efficient material handling solutions.




