Gray bin pneumatic conveying systems are advanced industrial solutions designed to efficiently transport bulk materials, such as powders and granules, from one location to another. These systems are widely used in various industries, including chemical, pharmaceutical, food processing, and mining, due to their flexibility, reliability, and ability to handle a wide range of material properties. The core of such a system is the gray bin, which serves as a storage and feeding unit, and the pneumatic conveying mechanism that moves the material through a network of pipes.
Introduction to Gray Bin Pneumatic Conveying Systems
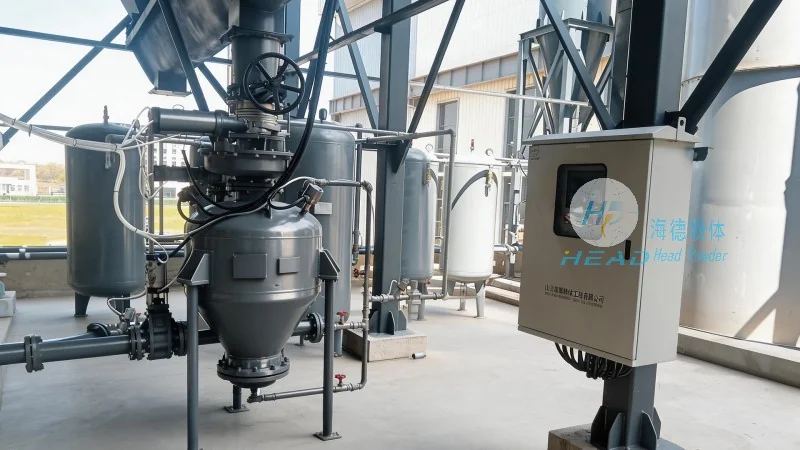
A gray bin pneumatic conveying system combines a storage bin with a pneumatic conveying unit to create a seamless material handling process. The system typically includes a hopper or bin for material storage, a feeder to control the flow of material into the conveying line, a series of pipes or ducts for transporting the material, and a separation or collection unit at the destination. The "gray bin" refers to the storage container, often made of metal or other durable materials, which is integrated with the conveying system to ensure a continuous and controlled flow of material.
Design Principles of Gray Bin Pneumatic Conveying Systems
The design of a gray bin pneumatic conveying system is based on several key principles to ensure optimal performance and efficiency. First, the system must match the specific characteristics of the material being conveyed, such as particle size, density, moisture content, and flowability. This involves selecting the appropriate type of feeder (e.g., rotary valve, star feeder) and conveying method (e.g., pressure or vacuum system). Second, the system's layout and components are designed to minimize pressure drop and energy consumption. This includes optimizing pipe diameters, using efficient fittings, and selecting the right blower or vacuum pump to maintain the required air velocity. Third, the system must ensure safety and compliance with industrial standards, including proper dust collection, explosion-proof features, and material containment to prevent leaks or spills.
Key Components and Their Functions
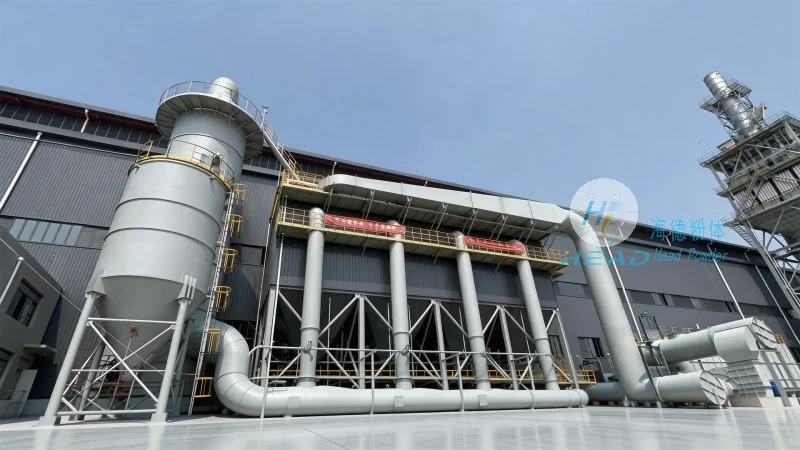
Several critical components make up a gray bin pneumatic conveying system, each playing a vital role in the overall operation. The gray bin itself is the primary storage unit, often equipped with a hopper design to facilitate material flow and prevent clogging. The feeder, typically a rotary valve or star feeder, controls the rate at which material is fed into the conveying line, ensuring a consistent and controlled flow. The conveying line consists of pipes or ducts that transport the material and air mixture. The blower or vacuum pump provides the necessary pressure or suction to move the material through the system. The separation or collection unit, such as a cyclone or baghouse, separates the material from the air at the end of the line, allowing the material to be deposited in the desired location while the air is filtered and discharged. Finally, the control system manages all aspects of the operation, including feeder speed, blower speed, and system pressure, to maintain optimal performance.
Advantages of Gray Bin Pneumatic Conveying Systems
Gray bin pneumatic conveying systems offer numerous advantages over traditional mechanical conveying methods. One of the main benefits is their ability to handle a wide variety of materials, including fine powders, sticky substances, and abrasive particles, without causing damage or contamination. The enclosed system also prevents dust and material from escaping into the environment, improving workplace safety and compliance with environmental regulations. Additionally, these systems are highly flexible, allowing for easy reconfiguration or expansion as production needs change. They also reduce the need for manual handling, minimizing labor costs and the risk of human error. Furthermore, modern systems are equipped with advanced controls and monitoring features, enabling real-time performance tracking and predictive maintenance to enhance efficiency and reduce downtime.
Applications and Industries
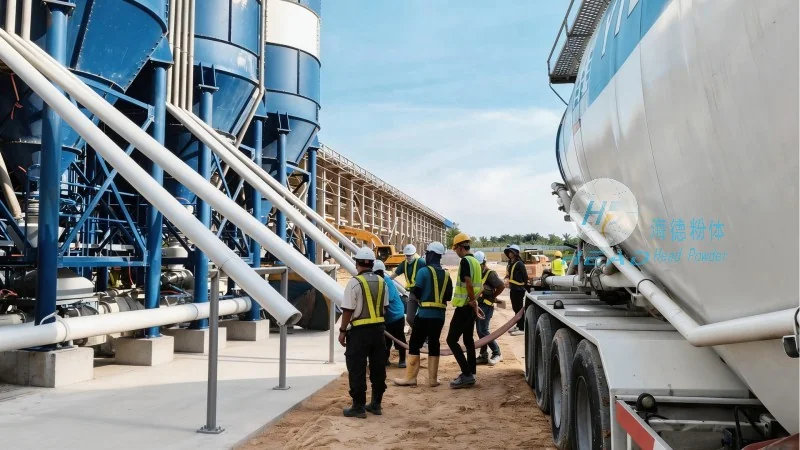
Gray bin pneumatic conveying systems are used in a wide range of industries due to their versatility and efficiency. In the chemical industry, they are used to transport powders like cement, plastics, and pigments. In the pharmaceutical industry, they handle sensitive materials like active pharmaceutical ingredients (APIs) and excipients, ensuring contamination-free transport. The food processing industry uses them to convey ingredients like flour, sugar, and spices, maintaining hygiene and preventing cross-contamination. In the mining and minerals sector, they transport ores and concentrates, often over long distances with high efficiency. Other applications include the handling of agricultural products, such as grains and seeds, and industrial waste materials.
Conclusion
Gray bin pneumatic conveying systems are sophisticated industrial solutions that combine storage, feeding, and pneumatic transport to efficiently handle bulk materials. The design principles, components, and advantages of these systems make them a preferred choice in many industries. As a leading manufacturer, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality gray bin pneumatic conveying systems tailored to the specific needs of clients. With a focus on efficiency, reliability, and safety, these systems provide a cost-effective and sustainable solution for material handling challenges. Whether for new installations or system upgrades, the expertise and products offered by HeadPowder ensure optimal performance and long-term value for industrial operations.




