For industrial operations dealing with bulk salt handling, understanding the salt material handling system is crucial. This system is engineered to efficiently transport, store, and manage salt, ensuring smooth workflow in various industrial processes. The design principles behind such systems are rooted in optimizing efficiency, safety, and reliability, tailored to meet the specific demands of salt processing and distribution.
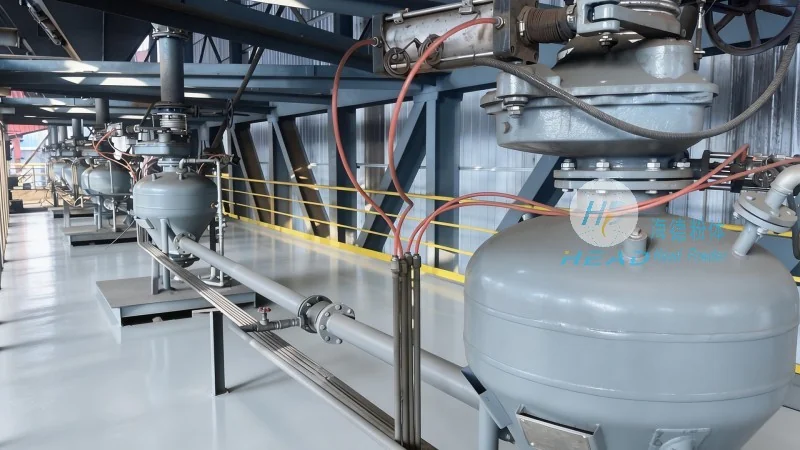
HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing advanced material handling solutions. With a strong commitment to innovation and quality, the company has established itself as a trusted provider of salt handling systems, catering to diverse industrial needs worldwide.
Design Principles of Salt Material Handling Systems
The design of a salt material handling system follows several key principles to ensure optimal performance. First, it prioritizes material flow efficiency, minimizing bottlenecks and reducing downtime. The system is engineered to handle the unique properties of salt, such as its granular nature and potential for dust generation, through specialized components like conveyor belts, hoppers, and dust control mechanisms. Second, safety is a paramount consideration. The design incorporates features like enclosed structures, proper ventilation, and protective guarding to prevent accidents and protect personnel. Third, durability and longevity are achieved through the use of corrosion-resistant materials, as salt environments can be harsh on equipment. Finally, flexibility is integrated into the design, allowing for easy integration with existing industrial setups and scalability to accommodate future growth.
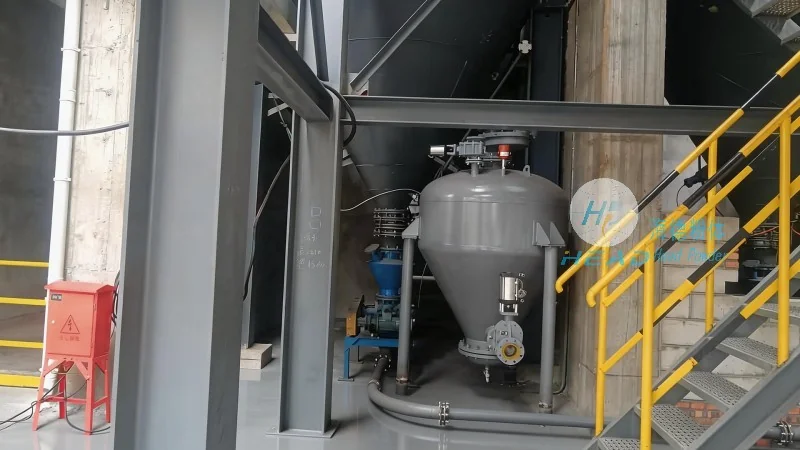
Key Components of the Salt Material Handling System
A typical salt material handling system consists of several interconnected components. The primary components include feeders, which evenly distribute salt into the system, and conveyors, such as belt conveyors or screw conveyors, that transport the material through the process. Hoppers and storage silos are used for bulk storage, ensuring a steady supply of salt. The system may also include elevators to move salt vertically, and screening or sorting equipment to separate impurities. Additionally, dust collection systems are essential to maintain air quality and comply with environmental regulations. Each component is carefully selected and integrated to work in harmony, ensuring seamless operation from raw material intake to final product delivery.
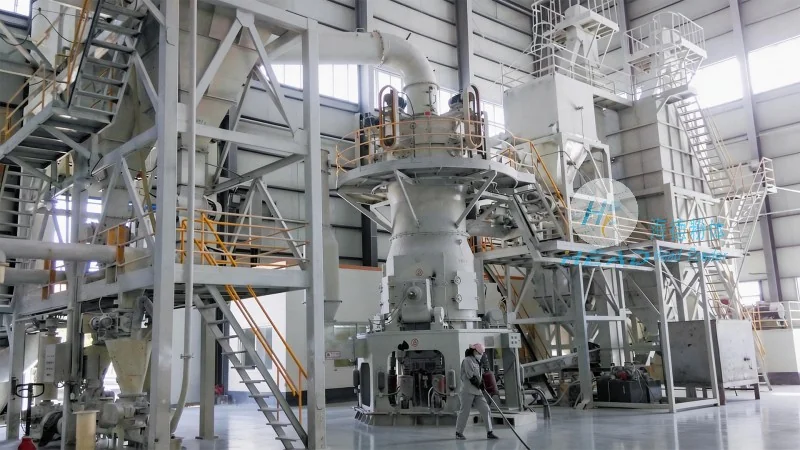
Applications in Industrial Salt Processing
Salt material handling systems are widely used in various industrial applications. In the food industry, they facilitate the processing of salt for food products, ensuring consistent quality and safety. In the chemical industry, salt is used as a raw material for manufacturing, and the system helps in transporting it to production lines. The mining and mining-related industries also rely on these systems for extracting and transporting salt from mines. Furthermore, in the water treatment sector, salt is used for desalination and purification processes, where the system ensures efficient handling of salt for brine management. The versatility of the salt material handling system makes it indispensable across multiple sectors, enhancing operational efficiency and reducing costs.
Conclusion
HeadPowder's expertise in designing and manufacturing salt material handling systems reflects a deep understanding of the industry's needs. By adhering to robust design principles and utilizing high-quality components, the company delivers systems that are efficient, safe, and durable. The integration of advanced technology and careful engineering ensures that these systems meet the demands of modern industrial operations, providing reliable solutions for salt handling challenges. With a strong presence in Shandong, China, HeadPowder continues to innovate and provide tailored solutions to clients worldwide, solidifying its position as a leader in the material handling sector.




