For industries dealing with powdered electrolytes, an efficient and reliable material handling system is crucial for maintaining production efficiency and product quality. The powdered electrolyte material handling system, as developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized solution designed to address the unique challenges of transporting and managing these materials. This system combines advanced engineering principles with practical application, ensuring safe and effective material flow in various industrial settings.
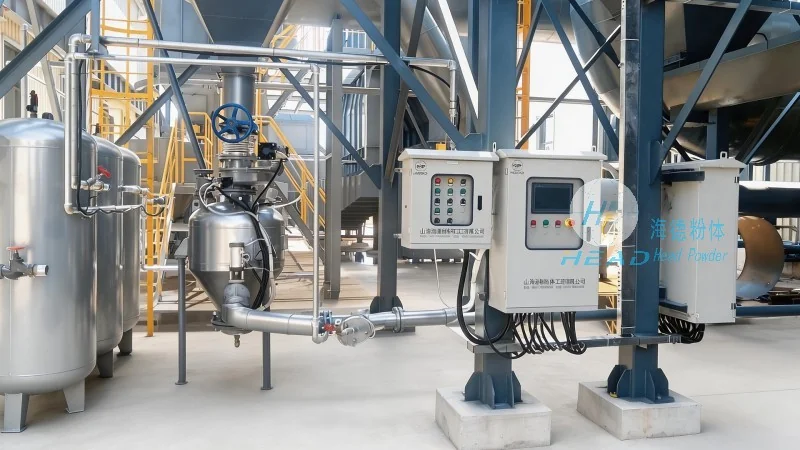
Powdered Electrolyte Material Handling System: Core Components and Functionality
The core of the system consists of several key components that work in tandem to facilitate the movement of powdered electrolytes. These components include feeders, conveyors, and control systems, each playing a vital role in the overall operation. The feeders are responsible for accurately measuring and dispensing the powder, ensuring consistent material flow. The conveyors, which can be of various types such as screw conveyors, pneumatic conveyors, or belt conveyors, transport the material from one location to another. Control systems, often integrated with sensors and automation technology, monitor the process and adjust parameters as needed to maintain optimal performance.
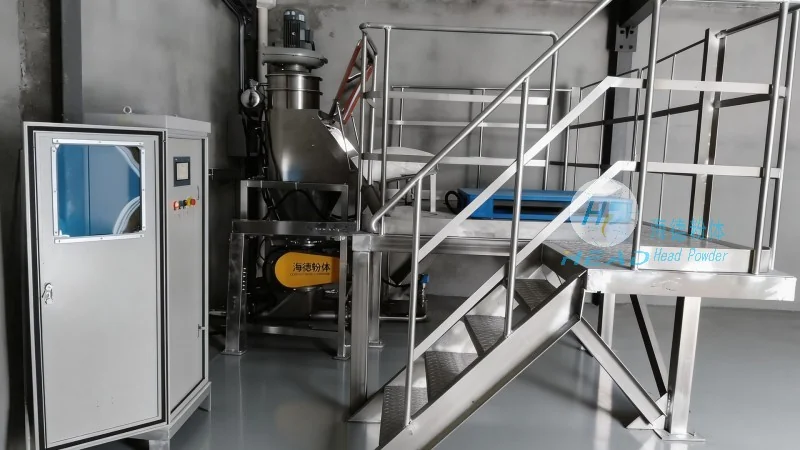
Design Principles Behind the Powdered Electrolyte Material Handling System
The design principles of the system are centered on several key factors, including material properties, operational requirements, and safety considerations. The system is engineered to handle the specific characteristics of powdered electrolytes, such as their particle size, density, and flowability. Engineers at Shandong HeadPowder Engineering Co., Ltd. carefully analyze these properties to select the appropriate equipment and materials for construction. Operational requirements, such as production capacity, space constraints, and integration with existing facilities, are also considered during the design phase. Safety is a paramount concern, with the system incorporating features like dust suppression, explosion-proof designs, and emergency stop mechanisms to protect personnel and equipment.
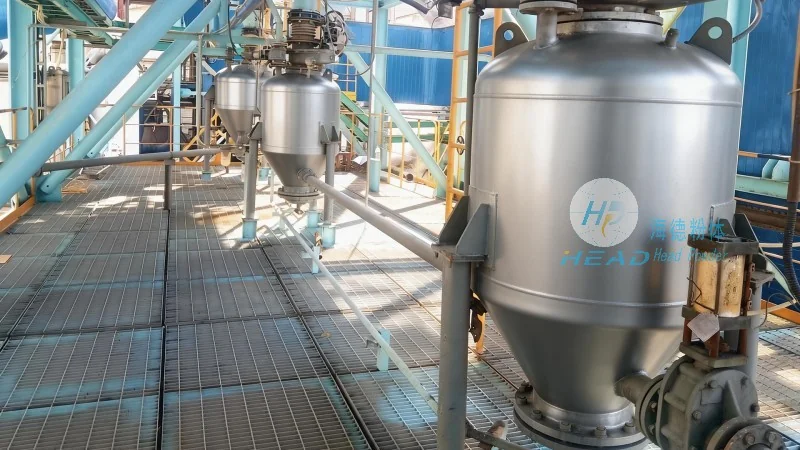
Advantages of the Powdered Electrolyte Material Handling System
Implementing a specialized material handling system for powdered electrolytes offers numerous advantages for industrial operations. One of the primary benefits is improved efficiency, as the system minimizes material loss and reduces downtime through precise control and automation. The consistent flow of material also enhances product quality by preventing segregation and contamination. Additionally, the system's design allows for easy integration with other production processes, streamlining the overall workflow. The use of advanced materials and engineering techniques ensures durability and long-term reliability, reducing maintenance costs and extending the system's lifespan.
Application Scenarios and Customization Options
The powdered electrolyte material handling system is versatile and can be applied in various industries, including battery manufacturing, chemical processing, and pharmaceuticals. The system can be customized to meet the specific needs of different applications, with options for different conveyor types, feeder capacities, and control systems. For example, in battery production, the system may be used to transport lithium carbonate or other electrolyte powders to the cell formation stage. In chemical processing, it can handle various powdered chemicals, ensuring safe and efficient material transfer. The flexibility of the system allows it to adapt to changing production demands and evolving industry standards.
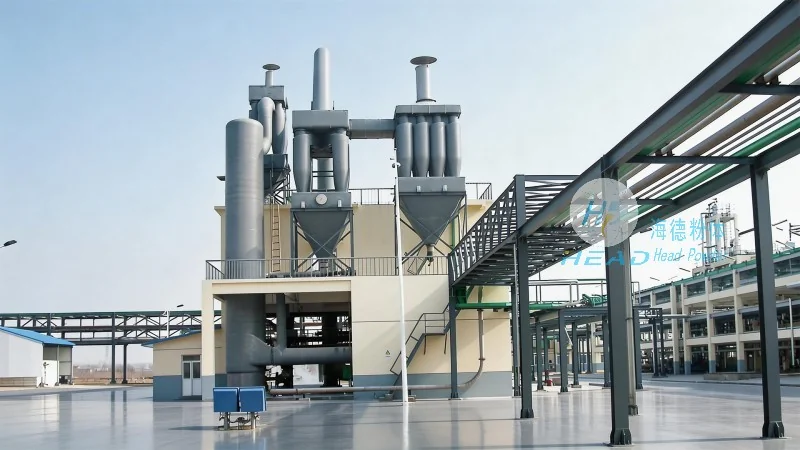
Conclusion: The Role of Shandong HeadPowder Engineering Co., Ltd. in Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd. plays a crucial role in providing advanced material handling solutions for industries dealing with powdered electrolytes. By combining expertise in engineering, material science, and industrial processes, the company develops systems that are tailored to the unique requirements of each client. The design principles and components of the powdered electrolyte material handling system reflect a commitment to quality, safety, and efficiency. As industries continue to evolve and demand higher standards of production, such specialized systems will remain essential for maintaining competitiveness and ensuring product excellence. The system not only addresses current material handling challenges but also supports future growth and innovation in the field.




