

Working Principle and Features of Glutinous Rice Powder Pneumatic Conveying Equipment
Glutinous rice powder is a critical raw material in the food and pharmaceutical sectors, demanding efficient and hygienic handling solutions. Pneumatic conveying equipment, specifically engineered for such powders, serves as a vital component in material transfer processes. This article delves into the working principle and distinctive characteristics of the glutinous rice powder pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd., a prominent manufacturer based in China.
Working Principle of Glutinous Rice Powder Pneumatic Conveying Equipment
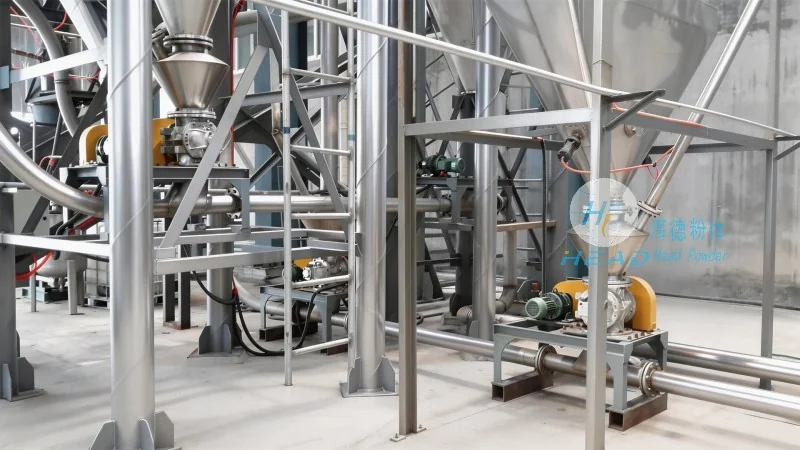
The fundamental operation of the pneumatic conveying system relies on air as the transport medium to move solid particles. For glutinous rice powder, the equipment typically operates on either suction or pressure principles. The suction system draws material from a hopper into a pipeline by creating a vacuum with a fan or blower, making it suitable for moving material from lower or remote locations to processing units. Conversely, the pressure system forces air and material through a pipeline using a positive pressure fan, ideal for longer distance transport or against gravity.
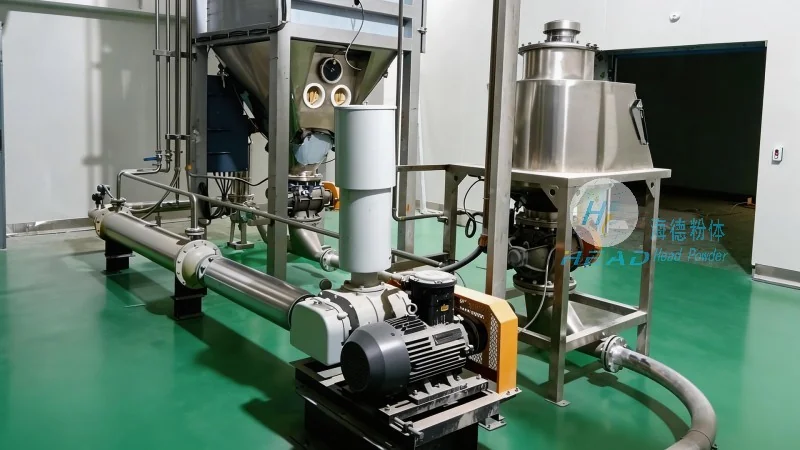
Key components of the system include a hopper for material storage, a rotary valve or feeder to regulate flow rate, a fan or blower to generate air flow, and a pipeline network for material transport. The system also incorporates a dust separator or cyclone at the receiving end to separate powder from air, ensuring clean and dry material collection. The entire process is automated, with sensors and controls monitoring flow rate, pressure, and air quality to maintain optimal performance.
Key Features of Glutinous Rice Powder Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd. offers pneumatic conveying equipment with several advantages tailored for glutinous rice powder handling. Firstly, the equipment minimizes product contamination and degradation by maintaining a sealed system, preventing exposure to air, moisture, and external contaminants—critical for food and pharmaceutical powders. Secondly, the system provides high efficiency and flexibility, accommodating a wide range of particle sizes and moisture contents, suitable for various processing stages from raw material transport to final product packaging.
Another notable feature is energy efficiency, with modern designs incorporating advanced fans and blowers that optimize air usage, reducing operational costs while sustaining performance. The equipment also facilitates easy maintenance and cleaning, with components that can be disassembled and sanitized to meet industry hygiene standards, particularly important in regulated sectors like food and pharmaceuticals.
Application and Benefits in the Industry
The pneumatic conveying equipment from HeadPowder is widely utilized in glutinous rice powder processing for applications such as food manufacturing (e.g., rice cakes, sweet rice products) and pharmaceuticals (powdered ingredients for tablets/capsules). Its ability to handle fine powders without clogging or agglomerating is a significant benefit, as these issues can cause production delays and material loss. Additionally, the system enhances workplace safety by eliminating manual powder handling, reducing dust inhalation and cross-contamination risks. The sealed design also minimizes particle spread, improving air quality and compliance with occupational health regulations.
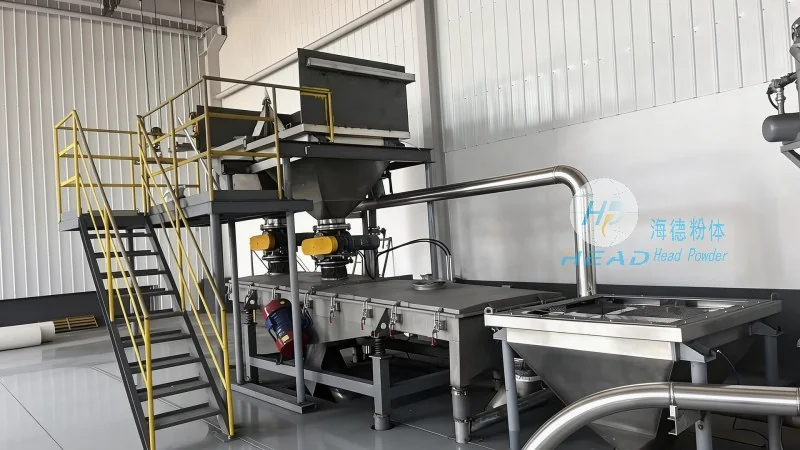
For companies in the glutinous rice powder processing industry, investing in this equipment from HeadPowder leads to improved productivity, reduced operational costs, and enhanced product quality. The system’s reliability and adaptability make it a cost-effective solution for meeting industry standards and customer demands.
Conclusion
In conclusion, the glutinous rice powder pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. integrates advanced technology with practical design to address the unique challenges of handling fine, sensitive powders. Its working principle, based on efficient air flow and sealed systems, ensures reliable and hygienic material transfer. The key features—including contamination control, energy efficiency, and ease of maintenance—make it an ideal solution for industries requiring high product quality and operational performance. As a leading manufacturer based in China, HeadPowder continues to innovate, providing tailored solutions that meet the evolving needs of the glutinous rice powder processing sector.