Working Principle and Features of Granular Fertilizer Pneumatic Conveying System Equipment
Release time:2026-09-17 08:01:23
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Granular fertilizer pneumatic conveying systems are advanced industrial equipment designed to efficiently transport bulk granular materials, such as fertilizers, over long distances or within complex processing facilities. These systems play a crucial role in modern agricultural and chemical industries by ensuring reliable, low-cost, and environmentally friendly material handling. The following sections will explore the working principle and key features of such systems, providing a comprehensive understanding of their functionality and benefits.
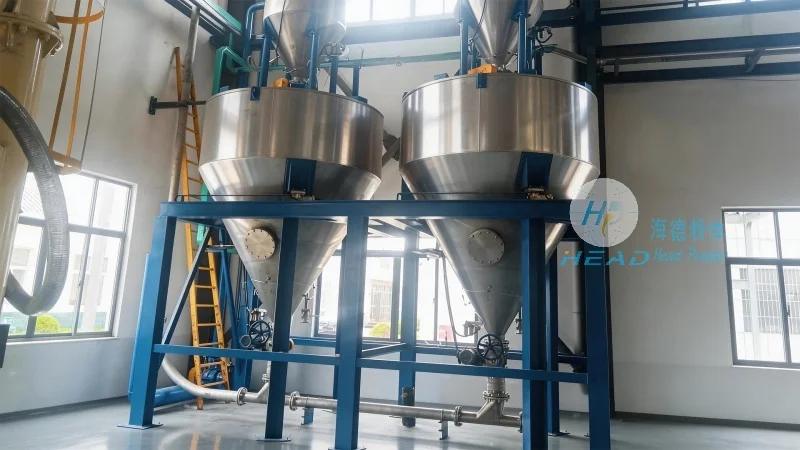
Working Principle of Granular Fertilizer Pneumatic Conveying Systems
The core mechanism of a granular fertilizer pneumatic conveying system relies on the use of compressed air to move material particles through a pipeline network. The system typically consists of a hopper for material storage, a blower or compressor to generate the necessary air pressure, and a series of pipes with inlets and outlets. When the system is activated, the compressed air is introduced into the hopper, creating a low-pressure zone that draws the granular fertilizer into the air stream. The air and material mixture then travels through the pipeline to the discharge point, where the air is separated from the material and either vented or recirculated. This process allows for continuous, automated material transport without the need for mechanical components like belts or buckets, reducing maintenance and operational costs.
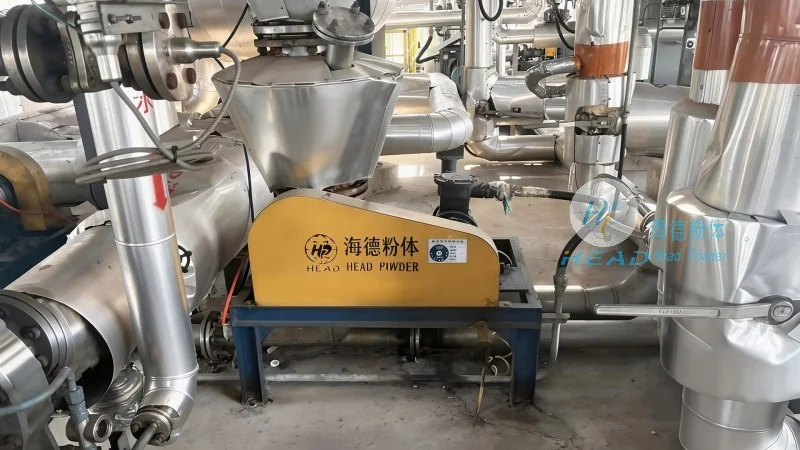
Key Features and Advantages of the Pneumatic Conveying System
Granular fertilizer pneumatic conveying systems offer several distinct advantages that make them ideal for industrial applications. Firstly, they provide high efficiency in material transport, capable of moving large volumes of granular materials over significant distances with minimal energy consumption. The system's design minimizes material degradation and loss, ensuring that the fertilizer quality is maintained throughout the conveying process. Additionally, pneumatic conveying systems are highly flexible, allowing for easy integration into existing production lines or expansion of the conveying network as needed. They also contribute to improved safety and hygiene in the workplace, as the material is contained within the pipeline, reducing dust exposure and the risk of contamination. Environmental benefits are another key feature, as these systems often incorporate air filtration and recycling mechanisms to minimize emissions and waste, aligning with modern sustainability goals in the industry.
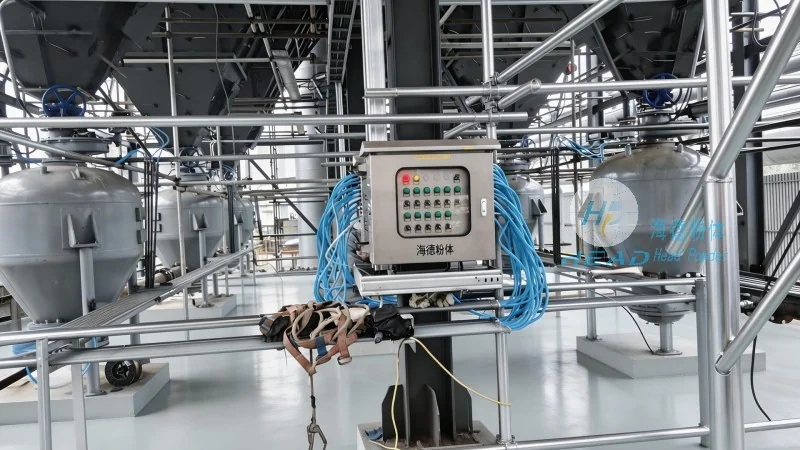
Company Information and Location
HeadPowder, a leading manufacturer of industrial conveying equipment, specializes in designing and producing granular fertilizer pneumatic conveying systems tailored to the specific needs of agricultural and chemical sectors. With headquarters in Shandong, China, the company leverages advanced engineering and manufacturing capabilities to deliver high-quality, reliable equipment that meets international standards. The company's commitment to innovation and customer satisfaction ensures that clients receive not only efficient conveying solutions but also comprehensive support throughout the equipment lifecycle.




