Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for the handling of rare earth crystal powders. These systems are engineered to meet the stringent requirements of industries that rely on precise and efficient material transport, ensuring minimal loss and optimal performance.
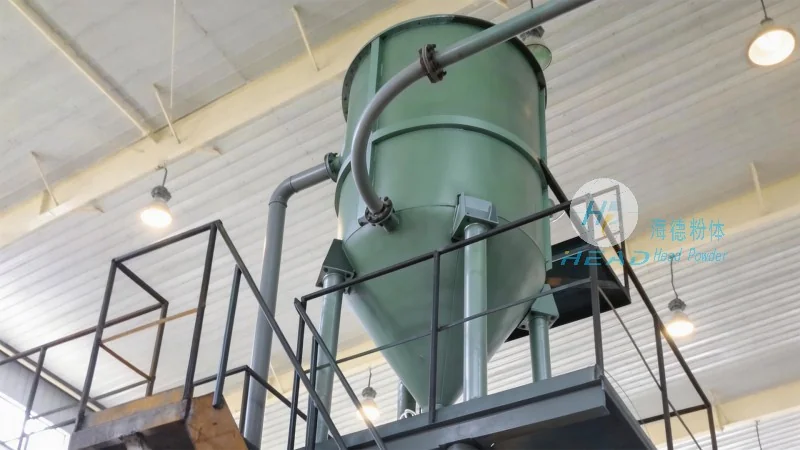
The working principle of a rare earth crystal powder pneumatic conveying system involves the use of compressed air or other gas to transport solid particles through a pipeline. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into a high-pressure air stream. As the air flows through the system, it carries the powder particles along the pipeline, delivering them to the desired destination. Key components include the material feeder, which controls the flow rate; the conveying line, which provides the path for the material and air mixture; and the separation equipment, such as cyclones or filters, which separates the powder from the air at the receiving end.
For rare earth crystal powders, the system is optimized to handle the unique properties of these materials, including their fine particle size, high density, and potential for static charge. The design incorporates features like static eliminators and anti-static coatings to prevent material buildup and ensure smooth operation. Additionally, the system may include temperature control mechanisms to maintain the integrity of the powder, as some rare earth compounds are sensitive to heat.
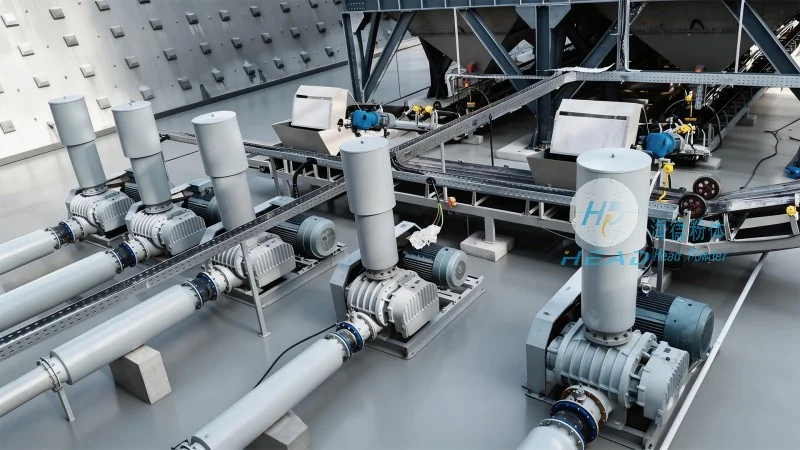
One of the primary advantages of pneumatic conveying systems for rare earth crystal powders is their efficiency in handling fine powders without the need for mechanical components that could cause clogging or contamination. Unlike traditional belt or screw conveyors, which may struggle with fine particles, pneumatic systems use air to move the material, reducing the risk of blockages and ensuring consistent flow rates. This makes them ideal for applications where precision and reliability are critical, such as in the production of rare earth magnets, catalysts, and other high-value materials.
Another key feature is the system's ability to handle a wide range of particle sizes and moisture content. By adjusting the air pressure and flow rate, operators can control the conveying velocity and prevent material degradation. This flexibility allows the system to adapt to varying production demands, making it a versatile solution for different stages of the rare earth processing workflow.
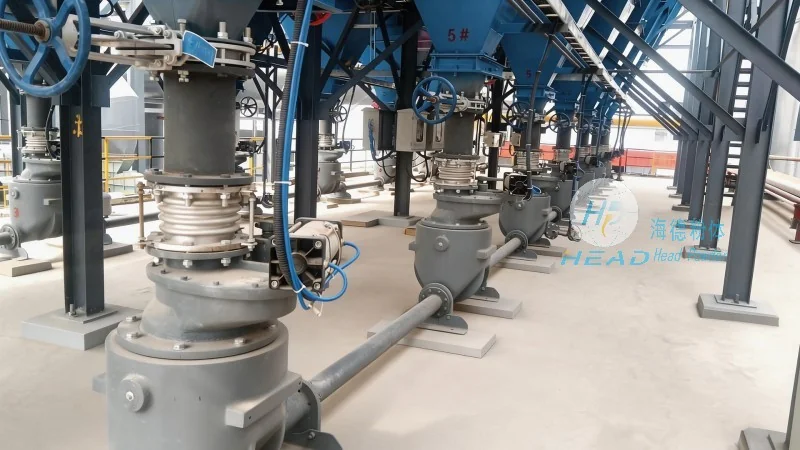
Environmental considerations are also a significant aspect of modern pneumatic conveying systems. The use of enclosed pipelines and efficient dust collection systems minimizes the release of fine powders into the environment, reducing health and safety risks for workers and complying with environmental regulations. This is particularly important for rare earth materials, which can be hazardous if inhaled or come into contact with skin.
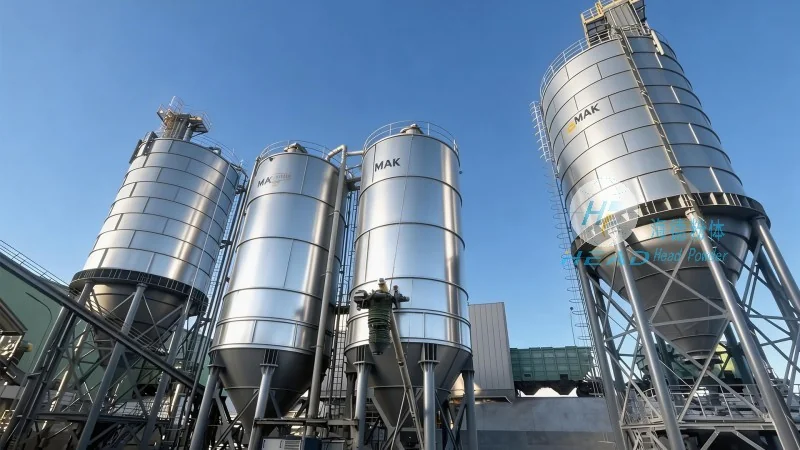
From a practical standpoint, the system's design ensures minimal maintenance and operational downtime. The use of robust materials, such as stainless steel or corrosion-resistant alloys, protects against the chemical properties of rare earth powders, which can be aggressive. Regular cleaning and maintenance procedures are simplified due to the enclosed nature of the system, as there are fewer exposed parts that could accumulate dust or debris.
In summary, the rare earth crystal powder pneumatic conveying system by Shandong HeadPowder Engineering Co., Ltd. combines advanced engineering with practical application to deliver a reliable and efficient solution for material transport. By understanding the working principles and leveraging the key features of this system, industries can enhance their production processes, improve safety, and maintain the quality of their rare earth products.




