Urea granule pneumatic conveying systems are critical in industrial processes for the efficient and safe transportation of urea granules. This article explores the working principle and key features of such systems, presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China.
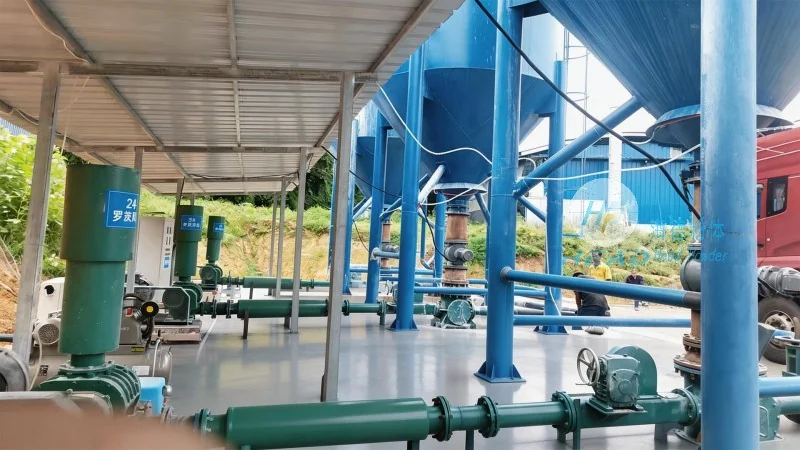
Introduction to Urea Granule Pneumatic Conveying Systems
Urea granule pneumatic conveying systems utilize air or gas to transport urea granules through a pipeline. This method is widely used in the fertilizer industry due to its ability to handle bulk materials with minimal human intervention and reduced risk of contamination. The systems are designed for reliable, continuous operation while maintaining product quality and adhering to safety standards.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company specializing in the design, manufacturing, and installation of pneumatic conveying equipment. Headquartered in China, the company has established a strong presence in the industry, delivering high-quality solutions tailored to the fertilizer and chemical sectors. HeadPowder's expertise lies in creating customized systems that enhance operational efficiency and reduce downtime, ensuring client satisfaction through professional service and robust product design.
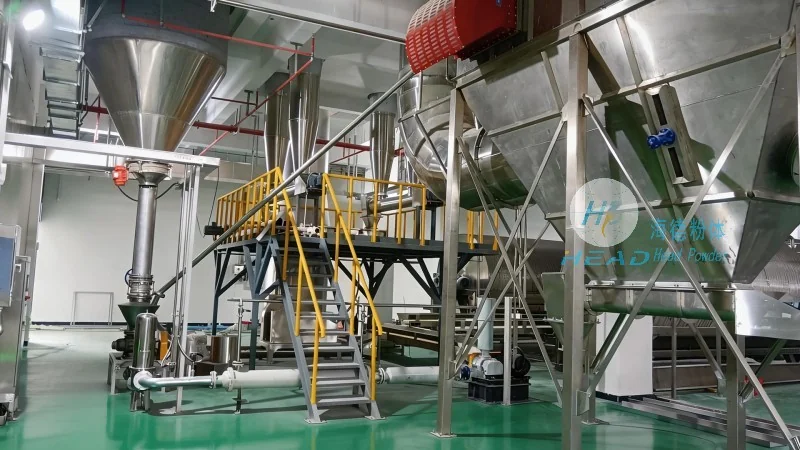
Working Principle of the Urea Granule Pneumatic Conveying System
The core working principle of a urea granule pneumatic conveying system involves generating airflow using a blower or compressor. The urea granules are introduced into the system via a hopper or feeder and are carried along by the moving air. The system operates on the principle of pneumatic transport, where the air velocity is sufficient to lift and transport the granules through the pipeline. Key components include a feeding device to introduce the material, a conveying line to transport it, and a discharge device to release the material at the destination. The system may also incorporate air filtration, pressure regulation, and material separation to ensure optimal performance and prevent system blockages.
Key Features and Advantages of the System
Urea granule pneumatic conveying systems offer several advantages that make them a preferred choice in industrial applications. One primary benefit is the ability to transport materials over long distances without complex infrastructure, such as conveyor belts or elevators, reducing installation and maintenance costs. The systems are highly flexible, allowing for adjustments in conveying route or capacity as production needs change. Another significant advantage is the reduced risk of material spillage and contamination, as the enclosed pipeline minimizes exposure to external elements. The systems also enhance safety by eliminating manual handling of bulk materials, thereby lowering the risk of accidents and injuries. Additionally, the systems contribute to energy efficiency by optimizing air usage and reducing waste.
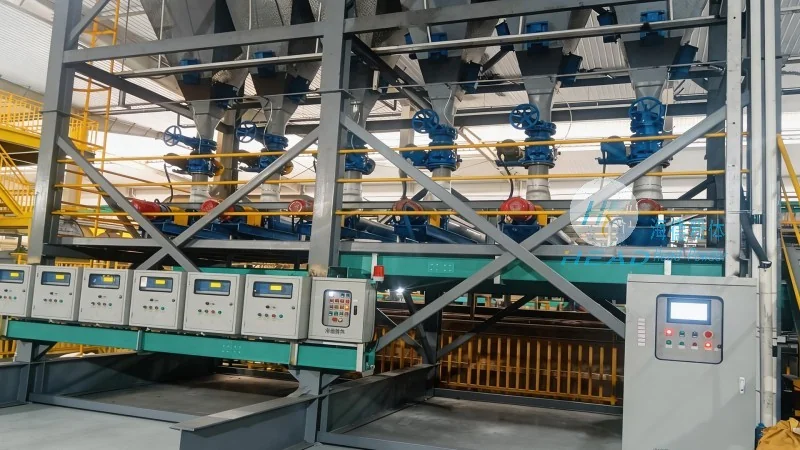
Customization and Application Scope
HeadPowder provides customized urea granule pneumatic conveying systems to meet diverse client requirements. The company's engineers collaborate closely with customers to understand specific operational needs, such as material volume, transport distance, and desired speed. Based on these inputs, the system is designed and manufactured to ensure optimal performance. The systems are applicable in various industries, including fertilizer production, chemical processing, and agricultural applications, where efficient handling of urea granules is critical for production continuity and product quality.
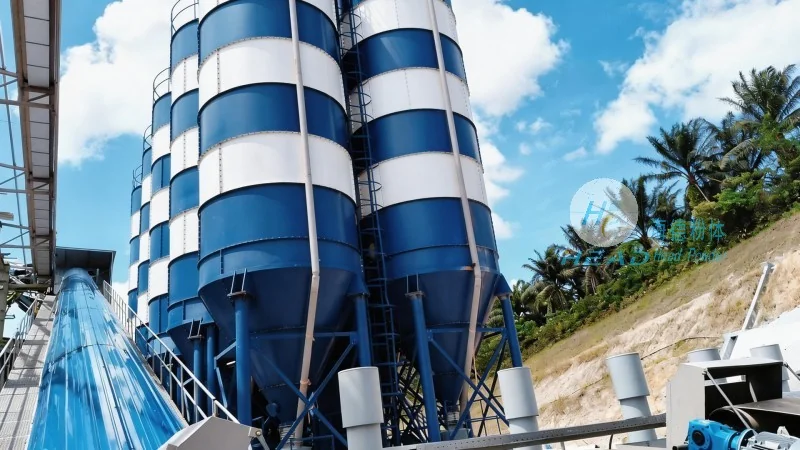
Maintenance and Operational Considerations
Proper maintenance is essential to ensure the longevity and reliability of urea granule pneumatic conveying systems. Regular inspections of components like the blower, pipeline, and feeding devices are necessary to identify and address potential issues before they escalate. System performance can be affected by factors including air pressure, temperature, and urea granule moisture content. Monitoring these parameters and adjusting the system accordingly is crucial for maintaining consistent operation. HeadPowder offers comprehensive maintenance services and technical support to clients, ensuring systems operate at peak efficiency and minimizing downtime.
Conclusion
In conclusion, urea granule pneumatic conveying systems are vital for the efficient handling of urea granules in industrial settings. The working principle, which relies on pneumatic transport, offers numerous benefits, including flexibility, safety, cost-effectiveness, and energy efficiency. Shandong HeadPowder Engineering Co., Ltd. specializes in delivering high-quality, customized systems that meet the specific needs of the industry. By understanding the working principles and features of these systems, users can make informed decisions about their material handling requirements, leading to improved operational efficiency, product quality, and overall business performance.




