HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced powder handling systems. Among their product portfolio is the tote bag packing powder conveying equipment, a sophisticated solution tailored for efficient bulk powder transportation and packaging. This article delves into the working principle and key features of this equipment, providing a comprehensive understanding for potential users and industry professionals.
Working Principle of Tote Bag Packing Powder Conveying Equipment
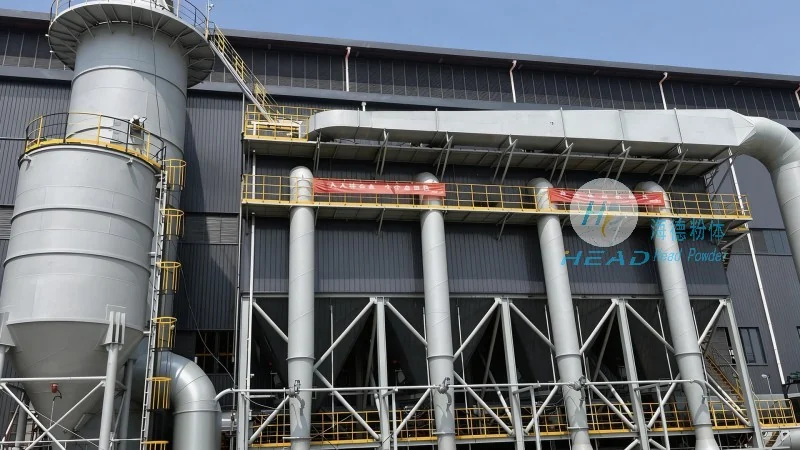
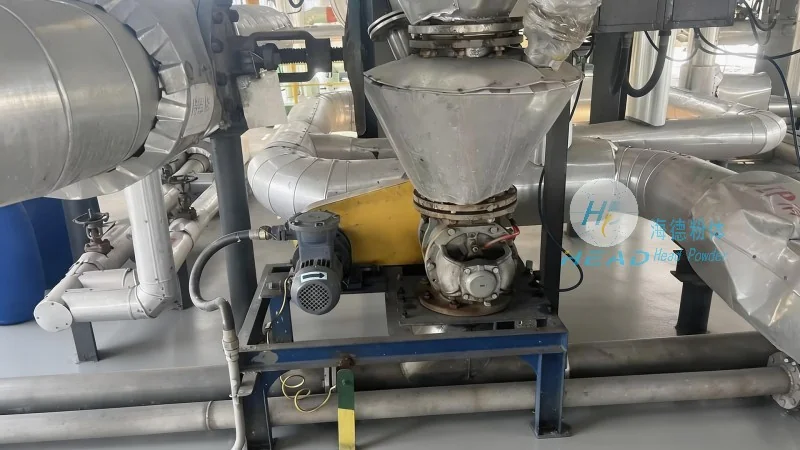
The tote bag packing powder conveying equipment operates on a systematic process that ensures seamless and reliable powder transfer from storage to packaging units. At its core, the system integrates several critical components, each playing a vital role in the overall functionality. The process begins with the loading of bulk powder into a storage hopper or silo. From there, the powder is fed into a conveyor system, typically utilizing screw conveyors or pneumatic pipelines, depending on the specific application and powder characteristics. The conveying mechanism then transports the powder to the tote bag filling station. Here, the equipment precisely measures and dispenses the required powder quantity into each tote bag, ensuring consistent weight and quality. The entire operation is controlled by an advanced PLC (Programmable Logic Controller) system, which manages the flow rate, pressure, and timing of the powder transfer. This automation not only enhances efficiency but also minimizes human error, leading to higher production throughput and reduced material waste.
Key Features of Tote Bag Packing Powder Conveying Equipment
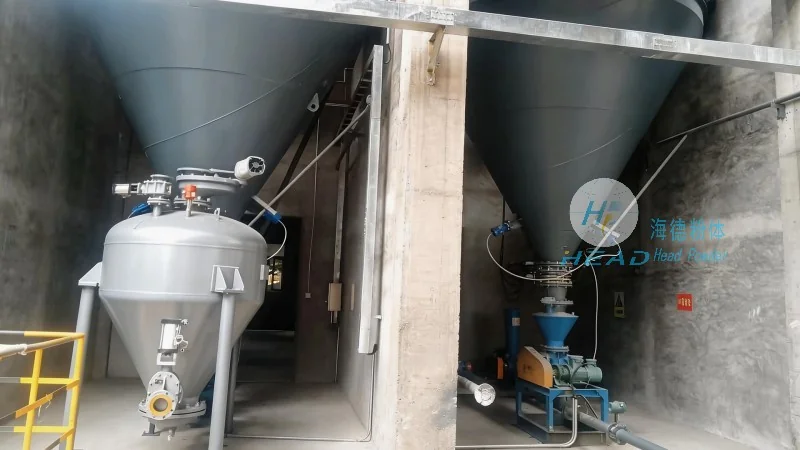
HeadPowder's tote bag packing powder conveying equipment is distinguished by a range of innovative features that address the unique challenges of powder handling. Firstly, the equipment is designed for high-capacity operation, capable of handling large volumes of powder while maintaining consistent performance. This is achieved through robust construction and efficient power transmission systems, ensuring durability even under heavy operational loads. Secondly, the system incorporates advanced sealing and dust control mechanisms, which are essential for maintaining product purity and preventing contamination. The use of high-quality materials and precision engineering minimizes the risk of powder leakage or airborne particles, making it suitable for applications in pharmaceuticals, food, and chemical industries where product integrity is paramount. Thirdly, the equipment offers high levels of flexibility and adaptability. It can be customized to accommodate various powder types, bag sizes, and filling volumes, allowing for versatile use across different production lines. Additionally, the integration of user-friendly interfaces and remote monitoring capabilities enables operators to easily adjust settings and troubleshoot issues, enhancing operational efficiency and reducing downtime. Finally, the equipment adheres to strict safety standards, incorporating features such as emergency stop buttons, overload protection, and automatic shut-off in case of blockages. These safety measures ensure a secure working environment and protect both personnel and equipment from potential hazards.
Benefits and Applications
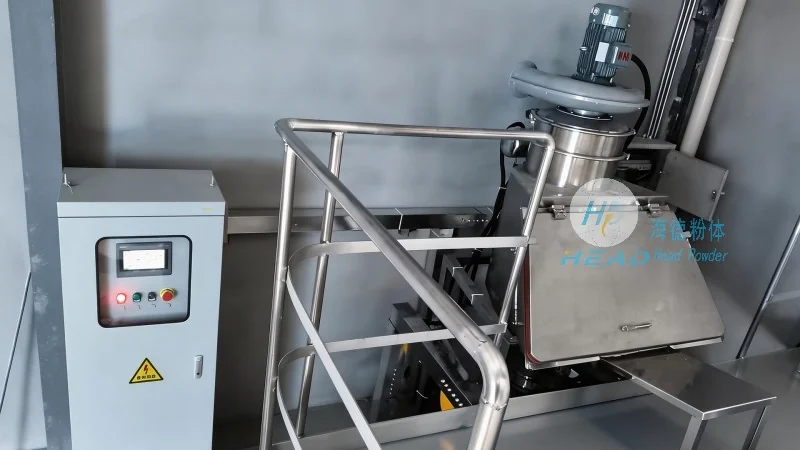
The tote bag packing powder conveying equipment from HeadPowder offers numerous benefits that make it an ideal choice for industries requiring reliable bulk powder handling solutions. The primary advantage is the significant improvement in operational efficiency, as the automated system reduces the time and labor required for powder transfer and packaging. This leads to higher production rates and lower operational costs. Additionally, the equipment enhances product quality by ensuring precise and consistent filling, which is crucial for maintaining product specifications and meeting regulatory requirements. The advanced sealing and dust control features also contribute to better product safety and compliance with industry standards. In terms of applications, this equipment is widely used in sectors such as food processing, pharmaceutical manufacturing, chemical production, and agricultural industries. It is particularly beneficial for handling fine powders, granules, and other bulk materials that are prone to caking or segregation. By streamlining the powder handling process, the equipment helps companies optimize their production workflows, improve inventory management, and enhance overall operational performance.




