[WOKING PRINCIPLE AND CHARACTERISTICS OF RARE EARTH MINERAL POWDER PNEUMATIC CONVEYING SYSTEMS]
Release time:2026-09-18 08:01:27
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for handling rare earth mineral powders. This article provides an in-depth look at the working principles and key characteristics of such systems, which are crucial for efficient material transport in industrial applications.
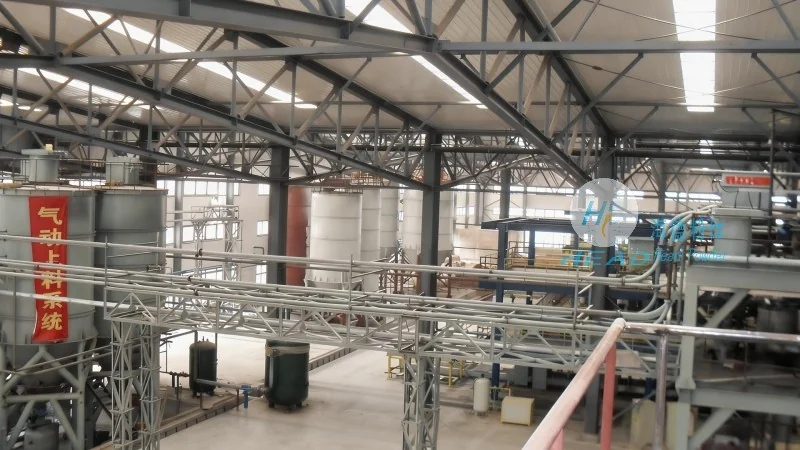
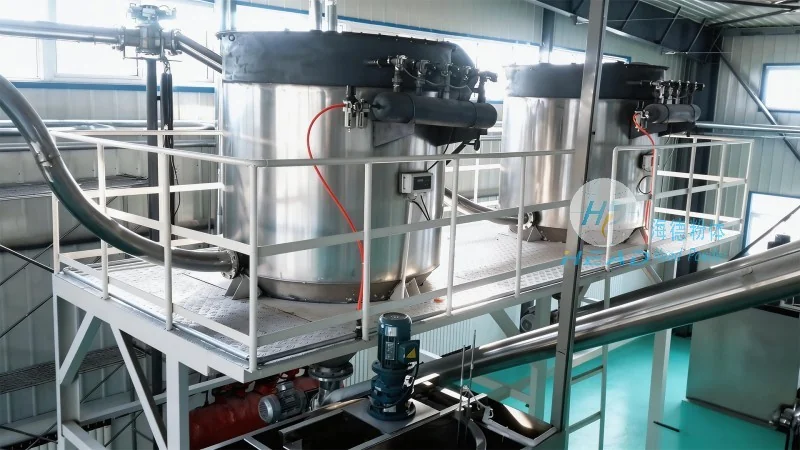
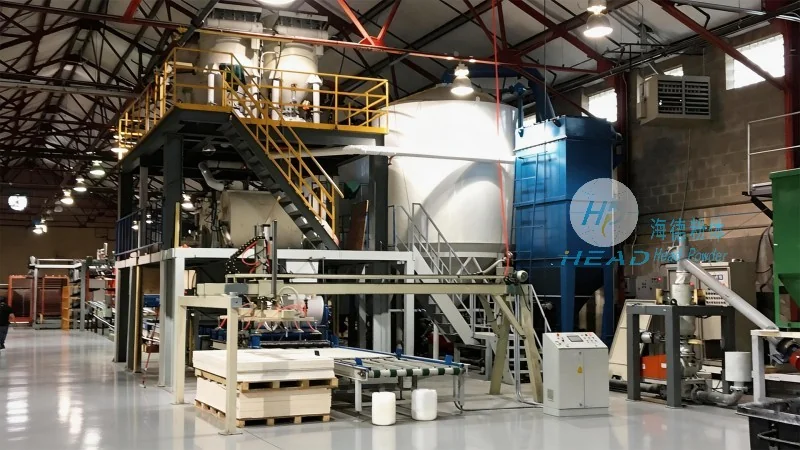
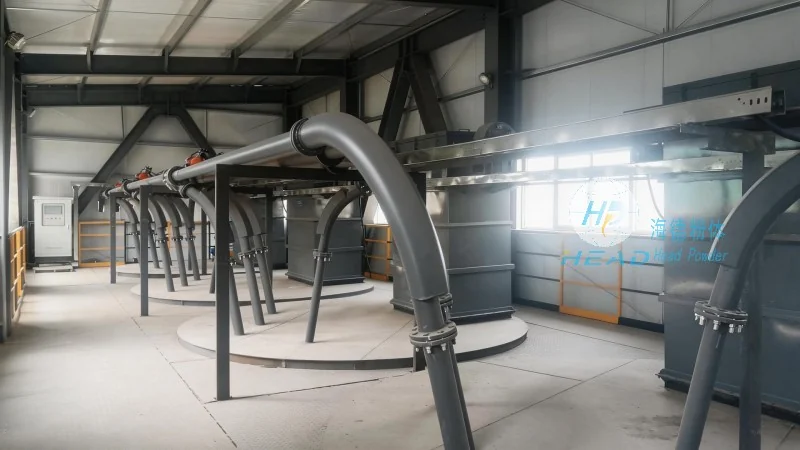
Working Principle of Pneumatic Conveying Systems for Rare Earth Mineral Powders
The core mechanism of a pneumatic conveying system involves the use of air or gas to transport bulk materials like rare earth mineral powders through a pipeline network. The process typically operates under either positive pressure (pressure conveying) or negative pressure (vacuum conveying), depending on the system design and application requirements. In positive pressure systems, a blower or compressor generates compressed air that propels the material forward through the pipeline. The material is often introduced into the system via a hopper or feeder, where it is mixed with the air stream to form a slurry or suspension. As the mixture travels through the pipeline, it encounters various components such as bends, elbows, and expansion joints, which are designed to maintain the material's flow without causing blockages or degradation. The system terminates at a receiver or destination point, where the material is separated from the air stream and collected. In contrast, negative pressure systems use a vacuum pump to create a low-pressure environment that draws the material into the pipeline. This method is particularly useful for applications requiring dust control or when the material needs to be transported from a higher elevation to a lower one. The working principle emphasizes the balance between air velocity, material feed rate, and pipeline design to ensure smooth and continuous transport.
Key Characteristics and Advantages of Rare Earth Mineral Powder Pneumatic Conveying Systems
Several distinct characteristics define the performance and benefits of pneumatic conveying systems for rare earth mineral powders. First, the system offers a high degree of flexibility in terms of layout and integration with existing industrial facilities. Unlike traditional mechanical conveying methods, pneumatic systems can easily adapt to complex or irregular plant layouts, allowing for efficient material transport between multiple points. Second, these systems provide excellent dust control and environmental protection. By enclosing the material in a sealed pipeline, the system minimizes dust emissions, which is critical for maintaining workplace safety and complying with environmental regulations. Third, pneumatic conveying systems are highly efficient in terms of energy consumption and operational costs. The use of air as the transport medium reduces the need for mechanical components like belts or chains, leading to lower maintenance requirements and longer service life. Additionally, the system can handle a wide range of material properties, including varying particle sizes, moisture content, and bulk densities, making it suitable for diverse rare earth mineral applications. Fourth, the technology offers enhanced process control and reliability. Modern pneumatic conveying systems are equipped with advanced sensors and control systems that monitor flow rates, pressure, and material levels in real-time. This allows for precise control over the transport process, reducing the risk of material loss or system downtime. Finally, the system provides a hygienic and clean environment for handling sensitive materials like rare earth powders, which is essential for industries where product purity is paramount.




