HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for handling calcium carbonate limestone powder. This article delves into the core working principles and distinctive features of such systems, providing a comprehensive overview for industry professionals and potential clients.
Working Principle of the Pneumatic Conveying System
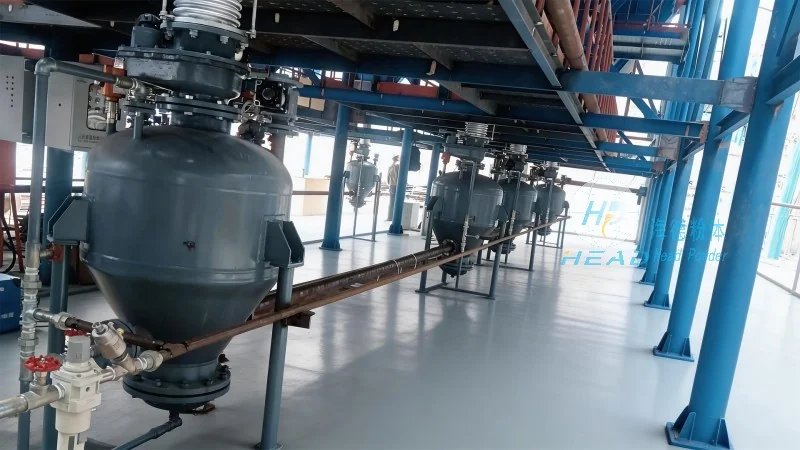
The pneumatic conveying system for calcium carbonate limestone powder operates on the fundamental principle of using compressed air to transport bulk materials through a pipeline network. The process typically involves several key components and steps that ensure efficient and reliable material transfer. First, the limestone powder is fed into a hopper or feeder, where it is then introduced into the conveying line. Compressed air, generated by a blower or compressor, is introduced at one end of the pipeline, creating a pressure differential that propels the powder particles forward. The air and powder mixture travels through the pipeline, with the air providing the necessary force to overcome friction and gravitational forces. At the receiving end, the air is separated from the powder, often through a cyclone separator or a filter, allowing the powder to be discharged into a storage or processing unit. The air, now clean, is either recirculated back into the system or vented to the atmosphere, depending on the system design. This continuous cycle of material feeding, air compression, and product separation ensures a seamless and automated operation, minimizing manual intervention and enhancing overall productivity.
Key Features of the Pneumatic Conveying System
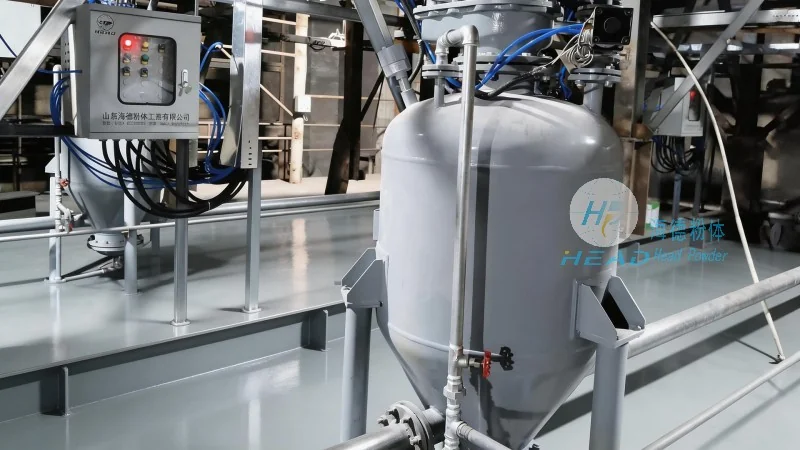
HeadPowder's pneumatic conveying systems for calcium carbonate limestone powder are characterized by several notable features that enhance performance, reliability, and user experience. One of the primary advantages is the ability to handle fine powders with high efficiency, ensuring minimal loss and consistent product quality. The system's design incorporates advanced control mechanisms that allow for precise regulation of air flow and pressure, which is crucial for maintaining optimal conveying conditions. This precision helps prevent issues such as blockages or uneven material distribution, which can occur in traditional mechanical conveying methods. Additionally, the system is designed for easy integration with existing production lines, making it a versatile solution for various industrial applications. The use of durable materials in the construction of the pipeline and components ensures long-term durability and resistance to corrosion, particularly important when handling calcium carbonate, which can be abrasive. Another significant feature is the system's ability to operate in a closed-loop environment, reducing dust emissions and improving workplace safety. This is achieved through the incorporation of efficient dust collection and filtration systems, which comply with environmental regulations and promote a healthier working environment. Furthermore, the system's compact design allows for installation in limited spaces, making it suitable for both new and retrofit projects. The integration of monitoring and diagnostic tools provides real-time feedback on system performance, enabling proactive maintenance and reducing downtime. These features collectively contribute to a system that is not only efficient but also user-friendly and environmentally responsible.
Benefits and Applications
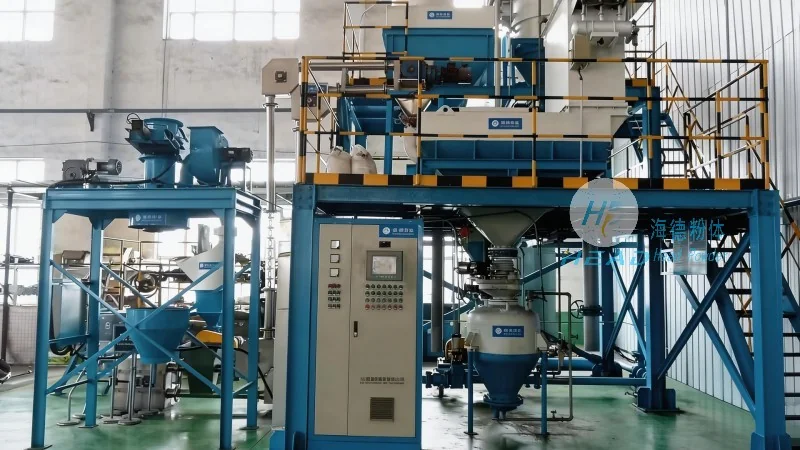
The pneumatic conveying system for calcium carbonate limestone powder offers numerous benefits that make it an ideal choice for various industrial applications. One of the most significant advantages is the reduction in labor costs and operational time, as the system automates the material handling process. This leads to increased productivity and lower operational expenses. The system also ensures consistent product quality by maintaining uniform particle size and preventing contamination, which is critical in industries such as pharmaceuticals, food processing, and chemical manufacturing. The ability to handle fine powders without degradation or agglomeration is particularly valuable in applications where material integrity is paramount. Additionally, the system's flexibility allows for easy adjustment of conveying rates and distances, making it adaptable to changing production demands. The closed-loop design contributes to environmental sustainability by minimizing dust emissions and reducing the need for additional cleaning and maintenance. This aligns with modern industrial standards and regulatory requirements, making the system a responsible choice for businesses committed to environmental stewardship. The system's reliability and low maintenance requirements further enhance its appeal, as it reduces the need for frequent repairs and downtime. Overall, the pneumatic conveying system provides a cost-effective and efficient solution for the transportation of calcium carbonate limestone powder, supporting the smooth operation of production lines and contributing to overall business success.




