For industries dealing with glucose powder, efficient and reliable material handling is crucial. Pneumatic conveying equipment has emerged as a preferred solution due to its ability to transport fine powders like glucose powder with precision and minimal contamination. This article explores the working principle and key features of such equipment, highlighting its application in the glucose powder processing sector.
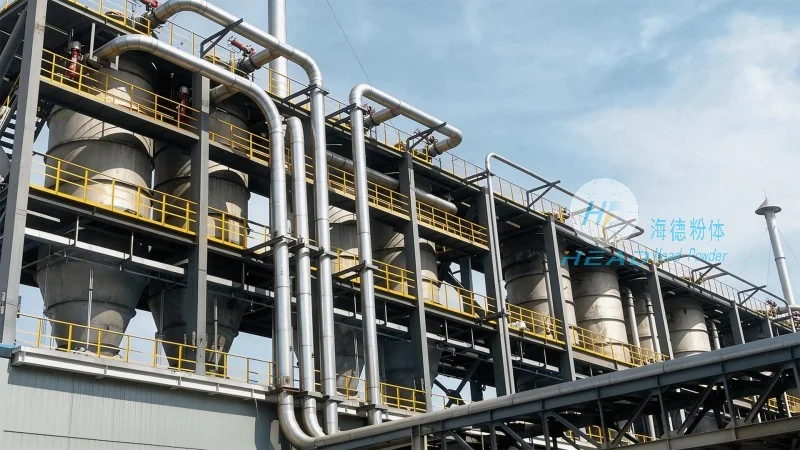
Introduction to Pneumatic Conveying Equipment for Glucose Powder Materials
Pneumatic conveying systems are widely used in the food and pharmaceutical industries to handle glucose powder, a critical raw material in various products. These systems offer a hygienic, dust-free method of transporting powders, which is essential for maintaining product quality and adhering to regulatory standards. The equipment is designed to move glucose powder from storage silos or processing units to packaging lines or other processing stages without the need for manual handling or mechanical conveyors.
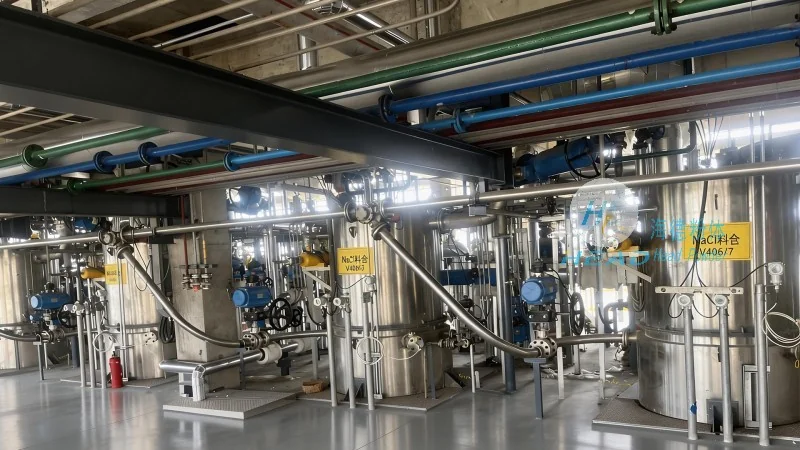
Working Principle of the Pneumatic Conveying Equipment
The core of pneumatic conveying equipment lies in the use of compressed air or other gases to create a flow that transports the glucose powder. The process typically involves a few key components: a hopper or feed inlet where the glucose powder is loaded, a conveying line (often flexible or rigid), and a receiver or discharge point where the material is deposited. The equipment operates by introducing a high-pressure air stream into the conveying line, which generates sufficient velocity to lift and move the glucose powder particles. The air and powder mixture travels through the line until it reaches the receiver, where the air is separated from the powder, often through a cyclone separator or other filtration system. This separation ensures that the glucose powder is collected in a clean, dry state, ready for further processing or packaging.
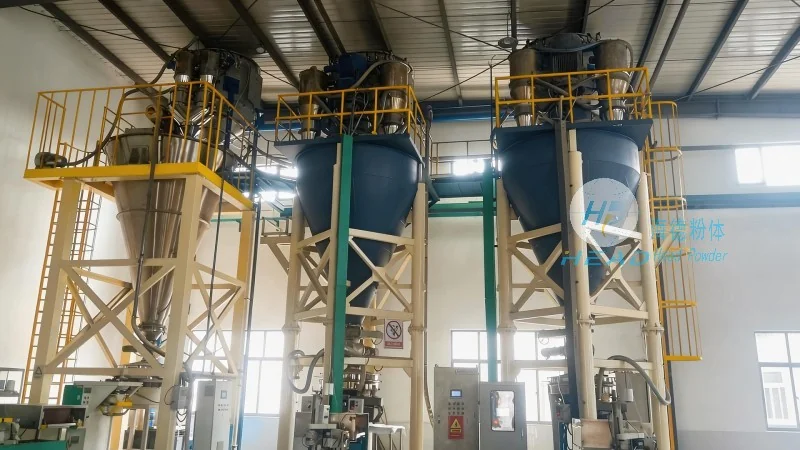
Key Features of the Equipment
The pneumatic conveying equipment for glucose powder materials is characterized by several advantages that make it ideal for industrial applications. Firstly, it provides high efficiency in material transport, capable of moving large volumes of glucose powder quickly and consistently. The system can be adjusted to handle varying particle sizes and moisture content, ensuring optimal performance for different types of glucose powders. Secondly, the equipment offers a hygienic and dust-free operation, which is critical in food and pharmaceutical manufacturing. The enclosed design prevents cross-contamination and minimizes the risk of product degradation due to exposure to air or external elements. Thirdly, it reduces labor costs and operational complexity compared to traditional methods like bucket elevators or belt conveyors. The system requires minimal maintenance, as it has fewer moving parts and is less prone to mechanical failures. Additionally, the flexibility of the conveying line allows for easy reconfiguration of the production layout, enabling manufacturers to adapt to changing production needs without significant modifications.
Application in Glucose Powder Processing
In the glucose powder processing industry, pneumatic conveying equipment plays a vital role in ensuring smooth workflow from raw material storage to final product packaging. The equipment is commonly used to transfer glucose powder from bulk storage silos to mixing or blending units, and then to packaging machines. Its ability to handle fine powders without clogging or agglomeration makes it suitable for maintaining the quality and consistency of the glucose powder. The system also helps in reducing downtime by providing a continuous and reliable supply of material, which is essential for maintaining production schedules and meeting customer demands. Furthermore, the hygienic design of the equipment ensures compliance with food safety regulations, such as those set by the FDA or EU, which is crucial for manufacturers in the food and beverage sector.
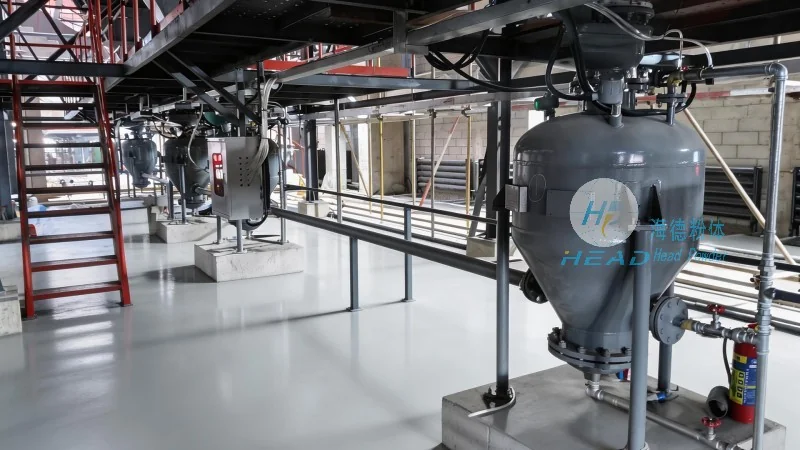
Company Information
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of pneumatic conveying equipment, specializes in providing customized solutions for glucose powder and other fine powder materials. With a focus on quality and innovation, the company has developed advanced systems that meet the stringent requirements of the food and pharmaceutical industries. HeadPowder's equipment is designed to enhance operational efficiency, reduce costs, and improve product quality, making it a trusted partner for businesses in the glucose powder processing sector. The company is located in Shandong, China, and serves clients globally with reliable and durable conveying solutions.




