Intelligent centralized material handling conveyors represent a pivotal advancement in modern industrial logistics, designed to streamline material flow, enhance operational efficiency, and reduce labor costs. These systems integrate advanced technologies such as automation, real-time monitoring, and data analytics to optimize material movement within manufacturing and warehouse environments. As businesses strive for greater productivity and flexibility, the adoption of such intelligent solutions has become increasingly critical.
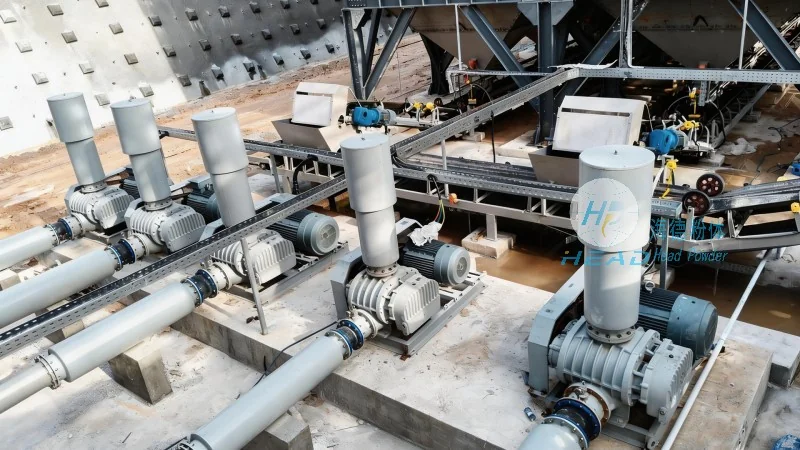
About Shandong HeadPowder Engineering Co., Ltd.
Headpowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of intelligent centralized material conveying systems. With a strong commitment to innovation and customer-centric service, the company has established itself as a trusted partner for industries seeking to upgrade their material handling infrastructure. Headpowder’s headquarters is located in Shandong, China, where the company leverages local expertise and resources to deliver high-quality products tailored to diverse industrial needs.
Principles of Intelligent Centralized Material Handling Conveyors
The core principle of intelligent centralized material handling conveyors lies in the integration of centralized control and distributed execution. These systems typically feature a central control unit that manages the entire material flow process, while individual conveying components (such as belts, rollers, or automated guided vehicles) operate autonomously based on real-time data and predefined algorithms. Key technologies include sensors for position and load detection, IoT connectivity for remote monitoring, and AI-driven decision-making to adapt to changing production demands. By centralizing control, these systems enable seamless coordination of material movement, minimizing bottlenecks and ensuring timely delivery of goods to workstations or storage areas.
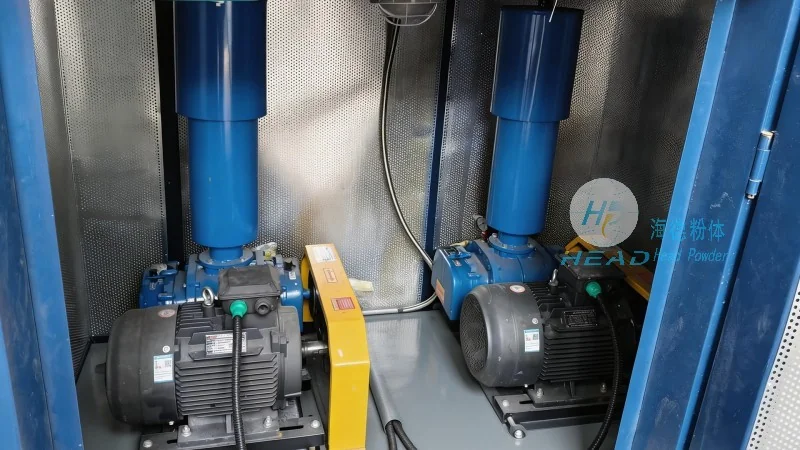
Working Scenarios and Key Features
Intelligent centralized material handling conveyors are versatile and adaptable to a wide range of industrial applications. They are commonly used in manufacturing plants, assembly lines, and distribution centers where high-volume material movement is required. The systems are designed to handle various types of materials, including bulk items, packaged goods, and even fragile or heavy loads, thanks to adjustable speed, load capacity, and safety features. A notable advantage is the ability to integrate with existing production lines, allowing for incremental upgrades without disrupting ongoing operations. Additionally, the centralized control system provides real-time visibility into material status, enabling operators to monitor performance, identify inefficiencies, and make data-driven adjustments to improve overall workflow.
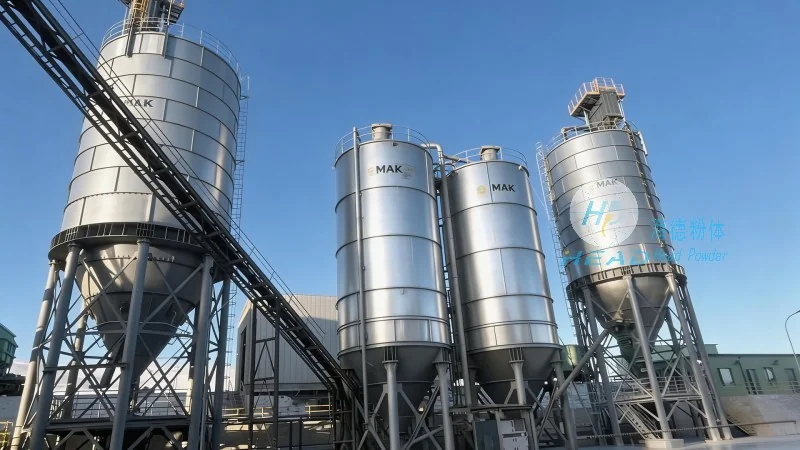
Benefits and Advantages in Practical Applications
Implementing intelligent centralized material handling conveyors offers numerous benefits that directly impact operational performance. Firstly, the automation of material movement reduces the need for manual labor, leading to significant cost savings and improved safety in the workplace. Secondly, the real-time monitoring capabilities enhance traceability and accountability, ensuring that materials are handled efficiently and in compliance with quality standards. Thirdly, the system’s adaptability allows for quick reconfiguration to accommodate changes in production schedules or product lines, providing flexibility in dynamic manufacturing environments. Furthermore, by optimizing material flow, these systems contribute to reduced lead times and increased throughput, ultimately boosting overall productivity and competitiveness for businesses.
Conclusion
Intelligent centralized material handling conveyors, as exemplified by the solutions offered by Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated approach to modern material logistics. By leveraging advanced technologies and centralized control, these systems address the challenges of traditional material handling methods, delivering enhanced efficiency, flexibility, and cost-effectiveness. For industries seeking to modernize their operations and stay competitive in today’s fast-paced market, investing in intelligent material handling solutions is a strategic move that can yield long-term benefits and sustainable growth.




