Bin pump material conveying lines are advanced pneumatic conveying systems widely used in various industrial sectors for efficient and reliable transportation of bulk materials. These systems are designed to handle a wide range of materials, including powders, granules, and fine particles, with high precision and minimal product degradation. The core of a bin pump system lies in its ability to utilize compressed air or other gases to create a pressure differential that propels materials through pipelines. This technology offers significant advantages over traditional conveying methods, such as reduced maintenance, lower energy consumption, and the capability to transport materials over long distances without the need for multiple transfer points.
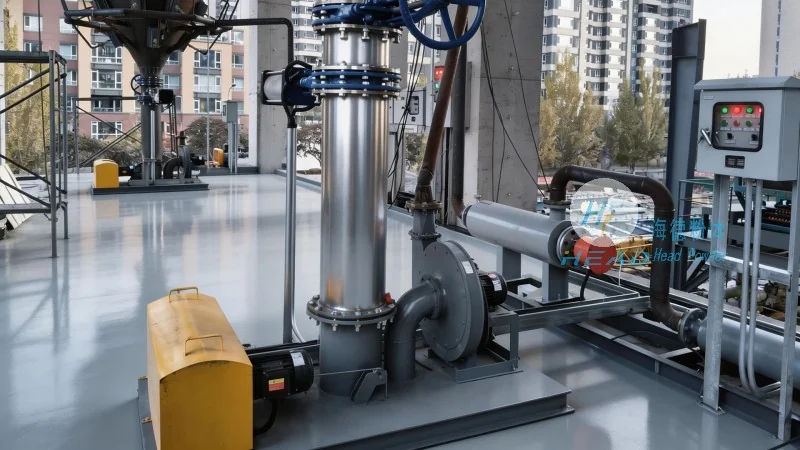
Company Profile: HeadPowder Engineering
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of material handling equipment based in Shandong, China. With years of experience in the industry, HeadPowder specializes in the design, development, and installation of bin pump systems tailored to meet the diverse needs of clients across different industries. The company's commitment to quality, innovation, and customer satisfaction has established it as a trusted partner in the material handling sector.
Principle of Bin Pump Material Conveying
The fundamental principle of a bin pump material conveying line is based on the pneumatic transport of bulk materials using compressed air. The system typically consists of a hopper or storage bin, a pump unit, and a pipeline network. The process begins with the material being fed into the hopper, where it is then sealed and pressurized by the pump unit. Compressed air is introduced into the hopper, creating a pressure that forces the material to flow through the pipeline to the discharge point. This pressure differential ensures a continuous and controlled flow of material, minimizing the risk of clogging and ensuring consistent performance. The bin pump operates efficiently by maintaining a stable pressure within the system, which is crucial for the smooth transport of various materials, including those with different particle sizes and densities.
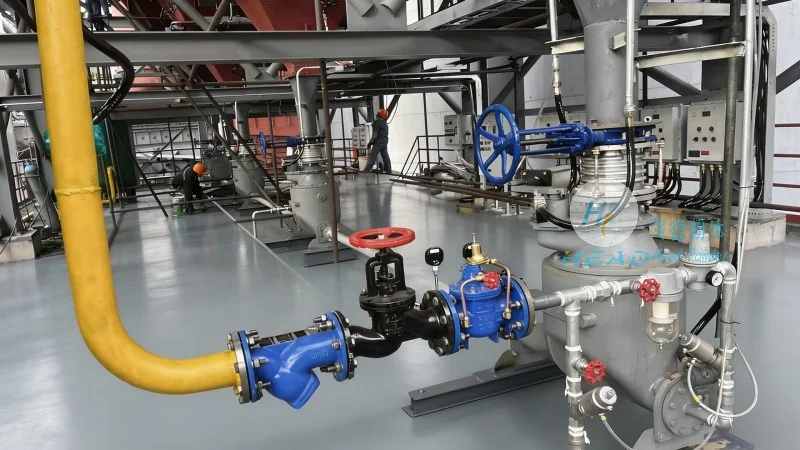
Working Scene Characteristics and Applications
Bin pump material conveying lines are versatile and can be applied in a wide range of working environments and industries. In the cement industry, for example, these systems are used to transport raw materials and finished products efficiently from storage silos to production lines. The high-pressure operation of bin pumps allows for the reliable handling of cement and other fine powders, ensuring minimal dust generation and product contamination. In the chemical and pharmaceutical sectors, bin pumps are employed to convey sensitive materials, such as powders used in drug manufacturing, with precision and hygiene. The ability to maintain a controlled environment and prevent cross-contamination makes bin pumps ideal for these applications. Additionally, in the food processing industry, bin pumps are utilized to transport dry food ingredients, such as flour and sugar, while adhering to strict sanitary standards. The system's design allows for easy cleaning and maintenance, ensuring compliance with food safety regulations.
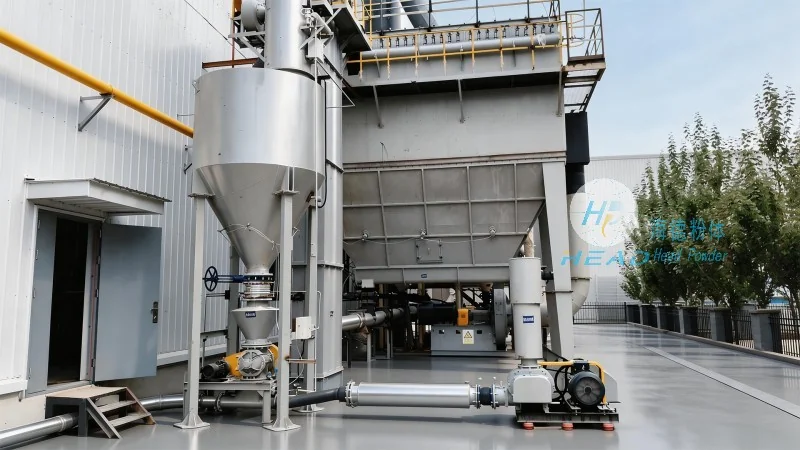
Key Features and Advantages
Bin pump material conveying lines offer several key features and advantages that make them a preferred choice for industrial material handling. One of the primary advantages is their ability to transport materials over long distances with minimal energy consumption. Unlike traditional belt conveyors or screw conveyors, bin pumps require less power to operate, resulting in lower operational costs. The system also provides flexibility in terms of layout, as the pipelines can be installed in various configurations to suit the specific needs of a facility. This adaptability allows for efficient use of space and easy integration with existing production lines. Another significant advantage is the reduced maintenance requirements. Bin pumps have fewer moving parts compared to other conveying systems, which reduces the likelihood of mechanical failures and lowers maintenance costs over time. The self-cleaning feature of bin pumps, where the pressure differential helps to clear any blockages, further enhances their reliability and operational efficiency.
Conclusion
Bin pump material conveying lines represent a sophisticated solution for the efficient and reliable transport of bulk materials in various industrial applications. With their pneumatic operation, high-pressure capabilities, and versatility, these systems offer significant benefits over traditional conveying methods. HeadPowder Engineering, as a leading manufacturer based in Shandong, China, continues to innovate and provide high-quality bin pump systems that meet the evolving needs of industries worldwide. By leveraging the principles of bin pump technology, companies can enhance their material handling processes, improve productivity, and ensure compliance with industry standards.




