Phosphorus pentoxide, a highly reactive and hygroscopic chemical compound, is widely used in various industrial applications such as pharmaceuticals, electronics, and chemical synthesis. The safe and efficient transportation of this hazardous material requires specialized equipment designed to handle its unique properties. This article explores the principles behind phosphorus pentoxide material conveying lines and highlights the key characteristics of their operational environments.
Introduction to Phosphorus Pentoxide and Its Handling Requirements
Phosphorus pentoxide (P₂O₅) is an inorganic compound known for its strong affinity for water, making it highly hygroscopic. When exposed to moisture, it rapidly reacts to form phosphoric acid, which can cause corrosion and pose safety risks. Due to its reactivity and potential for spontaneous combustion or release of toxic fumes, the handling of phosphorus pentoxide demands strict control measures. Conventional material handling methods, such as open-air conveyors or bulk storage, are unsuitable for this substance. Therefore, specialized conveying systems are essential to ensure safe and reliable transport from production sites to processing facilities or storage areas.
HeadPowder: A Leading Provider of Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a prominent manufacturer specializing in the design and production of advanced material conveying systems. With years of experience in the chemical processing industry, HeadPowder has developed state-of-the-art solutions tailored to the unique challenges of handling hazardous materials like phosphorus pentoxide. The company's commitment to safety, efficiency, and innovation has established it as a trusted partner for industries requiring reliable and secure material transport solutions.
The Principle of Phosphorus Pentoxide Material Conveying Lines
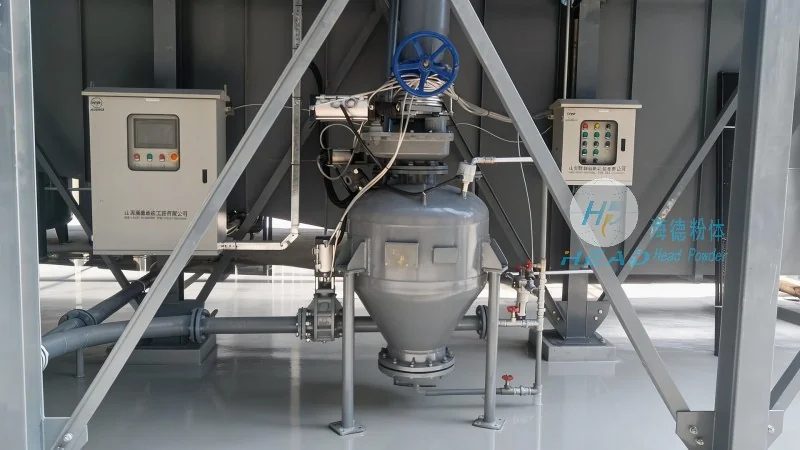
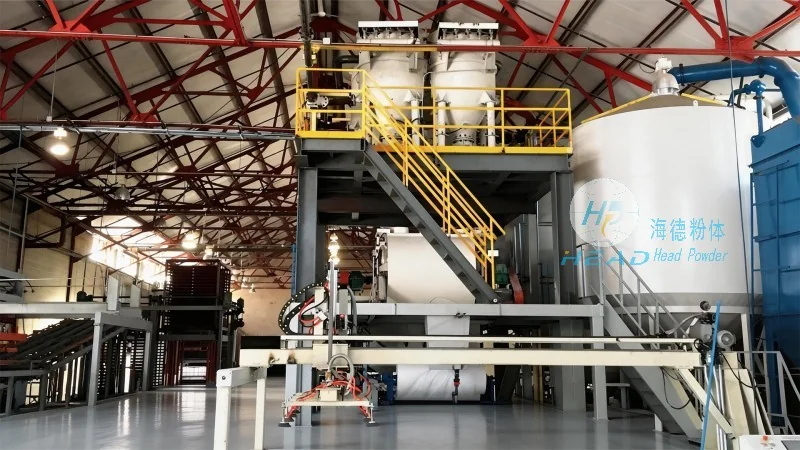
Phosphorus pentoxide material conveying lines typically operate on the principle of closed-loop or vacuum-assisted systems to prevent exposure to the environment and minimize the risk of accidental release. The core components of such a system include a vacuum pump, a sealed conveying pipeline, and a material feed hopper. The vacuum pump creates a negative pressure within the pipeline, drawing the phosphorus pentoxide powder from the feed hopper into the system. The sealed pipeline ensures that the material remains contained and does not come into contact with external air or moisture. The system may also incorporate additional features such as temperature control, filtration, and monitoring sensors to maintain optimal operating conditions and ensure the integrity of the material being transported.
Key Working Scene Characteristics
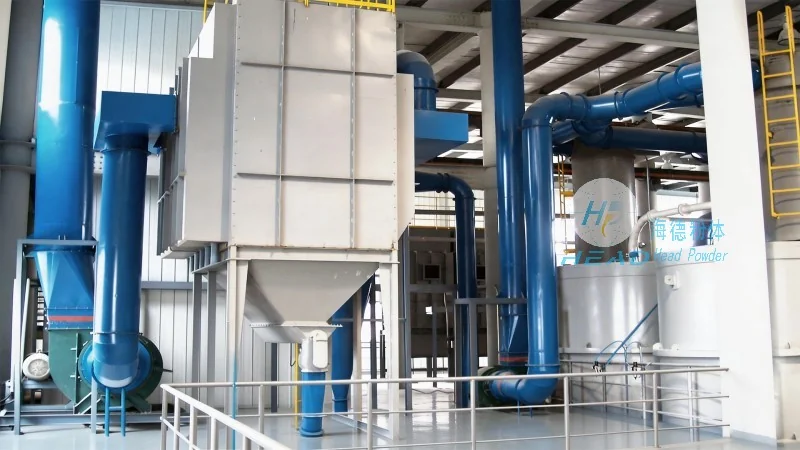
The operational environments of phosphorus pentoxide material conveying lines exhibit several distinct characteristics that influence their design and performance. Firstly, the need for strict containment and safety measures is paramount due to the material's reactivity and potential hazards. Conveying lines are typically installed in controlled environments, such as enclosed rooms or dedicated processing areas, to prevent accidental exposure. Secondly, the system must be capable of handling the material's hygroscopic nature, as moisture can cause clumping or degradation of the powder. This often requires the integration of drying or moisture-proofing components within the conveying line. Thirdly, the operational efficiency of the system is critical, as phosphorus pentoxide is often used in high-volume production processes. The design of the conveying line must optimize material flow rates while minimizing energy consumption and downtime. Additionally, the system must comply with relevant safety regulations and standards, such as those related to hazardous material handling, to ensure compliance and operational safety.
Applications and Industry Impact
Phosphorus pentoxide material conveying lines are widely used in various industrial sectors, including pharmaceutical manufacturing, electronic component production, and chemical synthesis. In pharmaceutical applications, the material is used as a drying agent or in the production of certain drugs, requiring precise and safe transport to avoid contamination or degradation. In electronics, phosphorus pentoxide is used in the production of semiconductor materials and as a component in certain types of batteries, necessitating reliable conveying systems to maintain product quality. The efficient operation of these conveying lines directly impacts production efficiency and product quality, making them a critical component of modern industrial processes.




