Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced cereal material conveying systems. These systems are engineered to efficiently handle the transportation of various cereal products, ensuring optimal performance and reliability in diverse industrial applications.
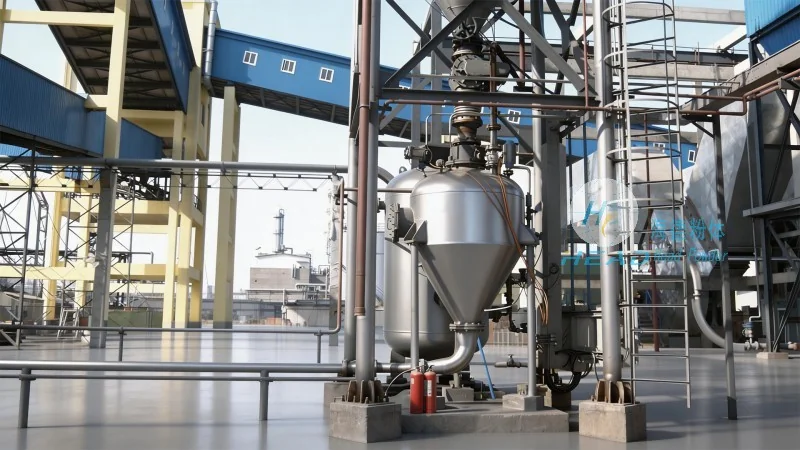
Principles of Operation for Cereal Material Conveying Equipment
The core principle of HeadPowder's cereal material conveying systems lies in the integration of robust mechanical components and intelligent control mechanisms. The systems typically utilize a combination of conveyor belts, screw conveyors, and pneumatic transport technologies to move cereal materials from one processing stage to another. Each component is meticulously designed to handle the specific characteristics of different cereal types, such as grain size, moisture content, and bulk density. The mechanical design ensures minimal material degradation while maintaining high throughput rates, making the equipment suitable for both large-scale production lines and smaller processing facilities.
Working Scene Characteristics and Applications
HeadPowder's cereal material conveying systems are tailored to meet the unique demands of various working environments. In food processing plants, these systems are commonly used in the initial stages of cereal handling, such as unloading raw materials from trucks or silos. The equipment is designed to operate in clean, sanitary conditions, adhering to food safety standards. Additionally, the systems are adaptable to different production scales, from small-scale artisanal operations to large industrial facilities. For example, in a breakfast cereal manufacturing plant, the conveying system efficiently transports raw grains to the milling and grinding units, ensuring a smooth flow of materials throughout the production process. The versatility of these systems also makes them suitable for use in grain storage facilities, where they help in the movement of stored cereals between storage bins and processing lines.
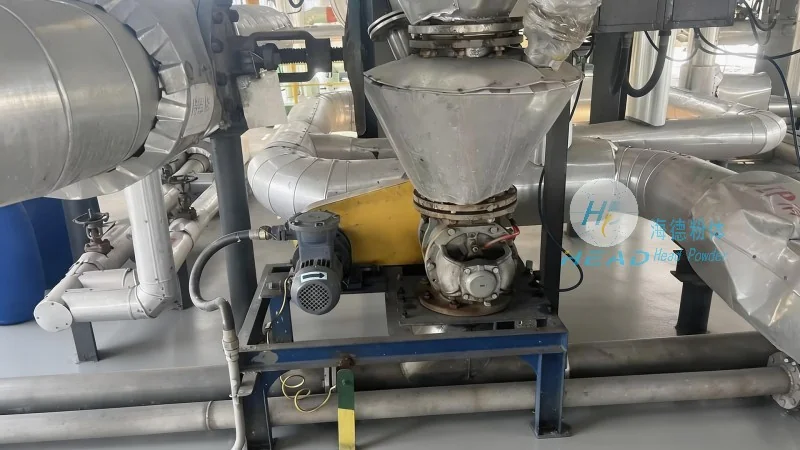
Key Features and Advantages in Real-World Applications
HeadPowder's cereal material conveying systems are equipped with several features that enhance their performance and reliability in real-world applications. One notable feature is the adjustable speed control, which allows operators to modify the conveyor speed based on the material being transported. This flexibility is particularly useful when handling different cereal types with varying flow characteristics. Another key feature is the inclusion of material sensors and monitoring systems, which provide real-time data on the system's operation and alert operators to any potential issues. These sensors can detect blockages, overloads, or changes in material flow, enabling quick troubleshooting and minimizing downtime. Additionally, the systems are constructed with durable materials, such as stainless steel and high-quality plastics, ensuring long-term durability and resistance to corrosion and wear. This durability is essential for maintaining consistent performance in harsh industrial environments.
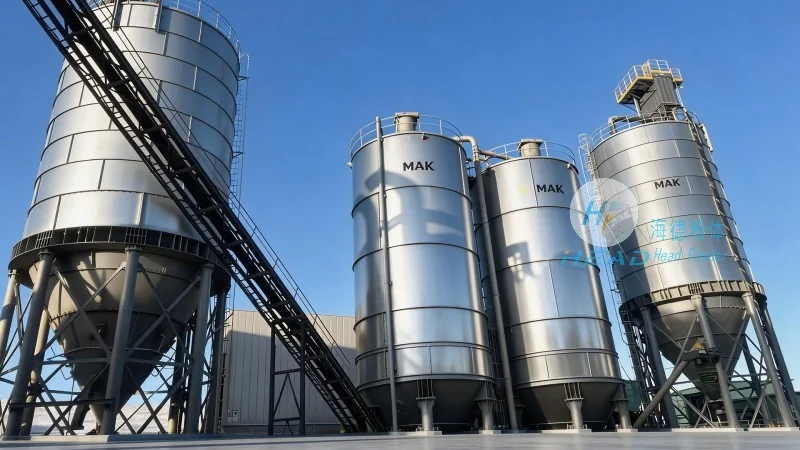
Adaptability to Diverse Industrial Environments
The adaptability of HeadPowder's cereal material conveying systems is a critical factor in their effectiveness across different working scenes. These systems are designed to operate in a wide range of conditions, including high humidity, temperature fluctuations, and dust-prone environments. For instance, in regions with high humidity, the equipment may include special sealing and moisture-resistant components to prevent material spoilage. In contrast, in dry, dusty environments, the systems may feature dust suppression mechanisms to maintain air quality and prevent material loss. This adaptability ensures that the conveying systems can be deployed in various industrial settings without compromising performance or safety. The robust design also allows for easy integration with existing production infrastructure, reducing installation time and costs for businesses.
Conclusion: The Role of Cereal Material Conveying Systems in Modern Processing
HeadPowder's cereal material conveying systems represent a sophisticated solution for the efficient and reliable transportation of cereal products in modern industrial settings. By combining advanced mechanical engineering with intelligent control technologies, these systems address the specific challenges of cereal handling, ensuring minimal material loss, consistent quality, and high operational efficiency. As a leading manufacturer based in Shandong, China, HeadPowder continues to innovate and refine its conveying systems to meet the evolving needs of the food processing industry. The adaptability and reliability of these systems make them a valuable asset for businesses seeking to optimize their production processes and enhance overall operational performance.




