Phosphate calcium powder, a critical raw material in various industrial applications, requires efficient and reliable handling solutions to ensure smooth production processes. The pneumatic conveying equipment designed for phosphate calcium powder is a specialized system that leverages air flow to transport these fine powders over long distances or within complex processing environments. This equipment is engineered to address the unique challenges associated with handling phosphate calcium powder, such as its dustiness, potential for agglomeration, and the need for precise control over particle movement.
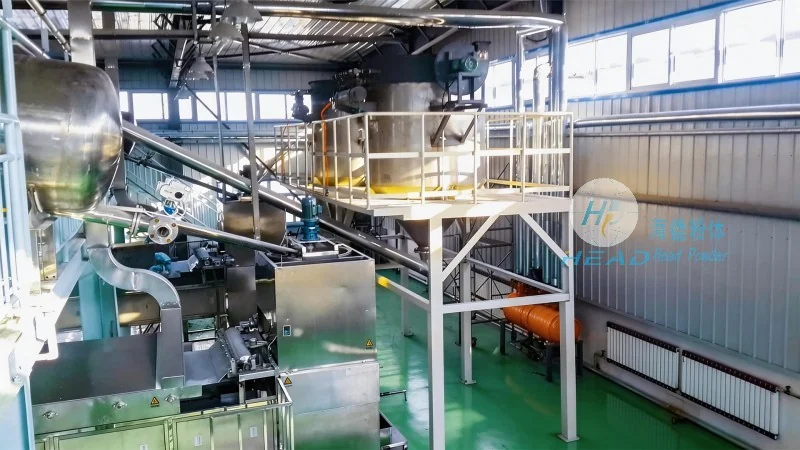
Working Principle of Pneumatic Conveying Systems for Phosphate Calcium Powder
The core principle of pneumatic conveying for phosphate calcium powder involves the use of a pressurized or suction system to move the powder through a pipeline using air. The system typically consists of a hopper or feeder that feeds the powder into the conveying line, a compressor or vacuum pump that generates the necessary air pressure, and a series of pipes and valves that direct the flow. In a pressurized system, air is introduced into the conveying line under pressure, pushing the powder forward. In a suction system, the air is drawn through the line, creating a negative pressure that pulls the powder along. The design of the system, including the type of air flow (e.g., dilute phase or dense phase), is tailored to the specific characteristics of phosphate calcium powder, such as particle size, density, and moisture content. The dilute phase system is commonly used for long-distance conveying, as it allows for higher flow rates and lower pressure drops, while the dense phase system is preferred for short distances or when handling more sensitive powders to minimize particle degradation.
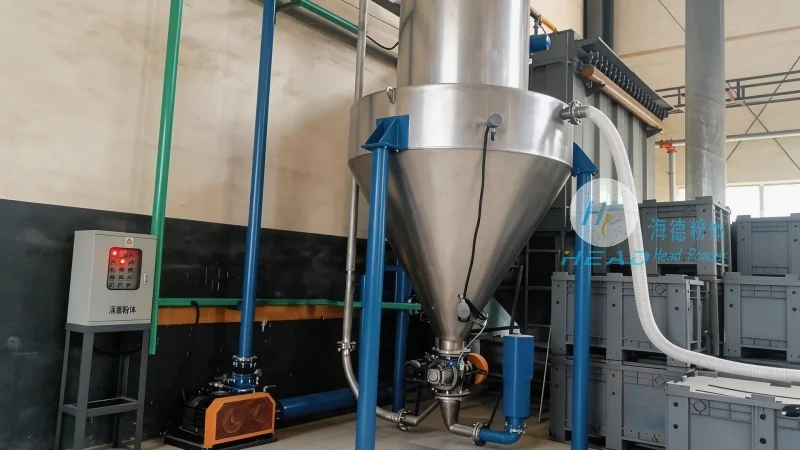
Key Features and Advantages of Phosphate Calcium Powder Pneumatic Conveying Equipment
Equipment for phosphate calcium powder pneumatic conveying is equipped with several features that enhance its performance and reliability. These include: 1. Advanced Feeding Mechanisms: The system utilizes precision feeders, such as rotary valves or screw conveyors, to ensure consistent and controlled powder intake, preventing blockages and maintaining uniform flow rates. 2. Specialized Hopper Design: The hoppers are designed with smooth, non-stick surfaces and sometimes equipped with vibration or air agitation systems to prevent powder agglomeration and ensure reliable discharge. 3. Efficient Air Compressors: High-efficiency compressors are used to generate the required air pressure, with options for variable speed control to adjust flow rates as needed. 4. Control Systems: Integrated control panels allow operators to monitor and adjust the conveying process in real-time, ensuring optimal performance and minimizing downtime. The advantages of this equipment include improved safety (as it eliminates the need for manual handling of powders), reduced material loss (compared to traditional methods like bucket elevators), and enhanced process control. Additionally, the system can be integrated with other processing equipment, such as mixers or reactors, to create a seamless production line.
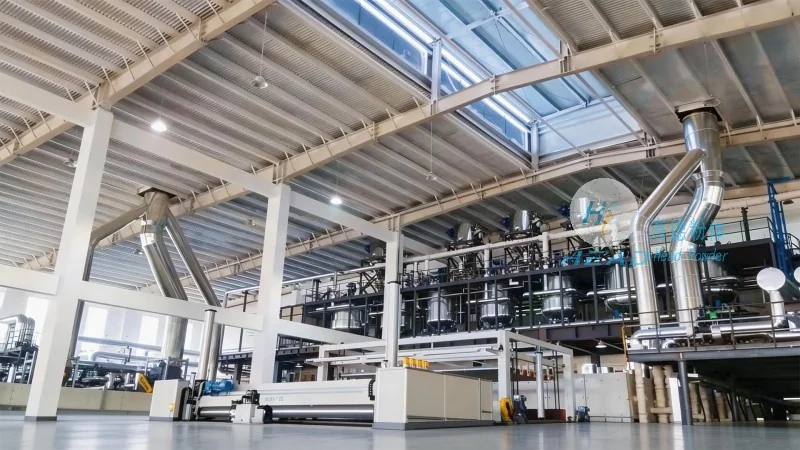
Typical Working Scenarios and Applications
The pneumatic conveying equipment for phosphate calcium powder is widely used in various industrial sectors, including pharmaceuticals, food processing, and chemical manufacturing. In the pharmaceutical industry, it is used to transport raw materials like calcium phosphate, which are critical components in drug formulations. The equipment ensures that these powders are handled in a sterile and controlled environment, minimizing contamination risks. In food processing, it is used to convey ingredients such as calcium carbonate or phosphate additives in food products, maintaining product quality and consistency. In chemical manufacturing, it is used to transport raw materials for the production of fertilizers, detergents, or other chemical products. The equipment is also suitable for applications where the powder needs to be transported from storage silos to processing units or between different stages of production. The working scenarios typically involve long-distance conveying (e.g., from a warehouse to a processing plant) or within complex factory layouts, where traditional mechanical conveyors may not be feasible due to space constraints or the need to avoid cross-contamination.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized pneumatic conveying equipment for various industrial powders, including phosphate calcium powder. The company is headquartered in Shandong, China, and has established itself as a trusted provider of high-quality, reliable conveying solutions. With years of experience in the industry, headpowder has developed a deep understanding of the unique challenges associated with handling phosphate calcium powder and has engineered equipment that addresses these challenges effectively. The company's products are designed to meet international standards and are customized to meet the specific requirements of each client, ensuring optimal performance and long-term reliability. Headpowder's commitment to quality and innovation has made it a preferred choice for many industries seeking efficient and safe powder handling solutions.
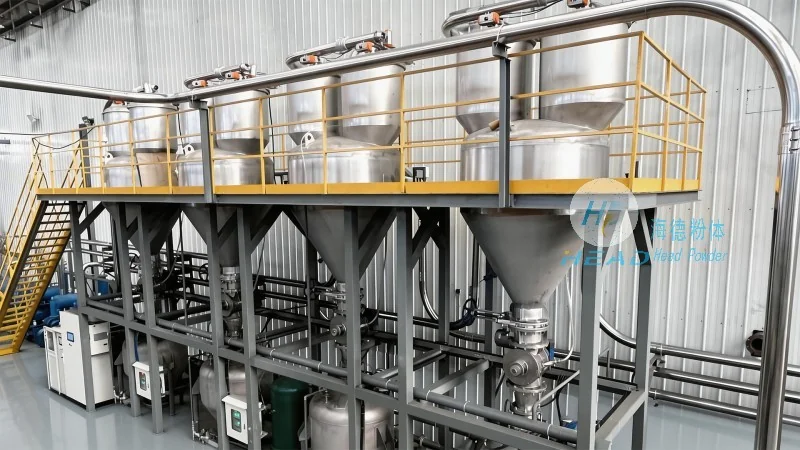
Conclusion and Future Outlook
Phosphate calcium powder pneumatic conveying equipment plays a vital role in modern industrial processes, providing efficient, safe, and reliable solutions for transporting these critical powders. The equipment's working principle, combined with its advanced features and tailored applications, ensures that it meets the demands of various industries. As industries continue to evolve and demand higher efficiency and precision in their operations, the importance of specialized conveying equipment like this will only grow. Companies like Shandong HeadPowder Engineering Co., Ltd. are at the forefront of developing and improving such equipment, ensuring that the needs of the industry are met with cutting-edge technology and expertise. The future of phosphate calcium powder handling is likely to see further advancements in equipment design, with a focus on sustainability, energy efficiency, and automation, which will further enhance the performance and benefits of pneumatic conveying systems.




