

What is a Dusty Ash Material Handling System Equipment? What Are Its Design Principles?
For industrial facilities dealing with dusty ash and similar materials, efficient material handling systems are crucial for maintaining operational efficiency and safety. The dusty ash material handling system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized solution designed to manage the transportation and processing of these materials with precision and reliability. This equipment plays a vital role in various industrial applications, ensuring that dusty ash is handled safely and effectively throughout the material flow process.
Key Components and Functions of the System
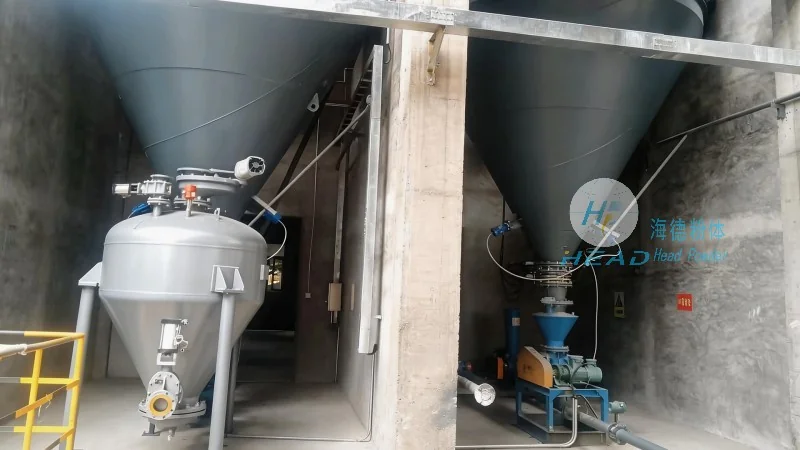
The dusty ash material handling system typically consists of several key components that work in tandem to ensure smooth material transport. These components include conveyor systems, dust collection units, and control mechanisms. The conveyor systems, often equipped with specialized belts or buckets, are designed to move dusty ash from one location to another within the facility. Dust collection units are integrated to capture and filter airborne particles, ensuring compliance with environmental regulations and maintaining a safe working environment. Control mechanisms allow operators to monitor and adjust the system's performance in real-time, optimizing material flow and reducing downtime.
Design Principles and Engineering Considerations
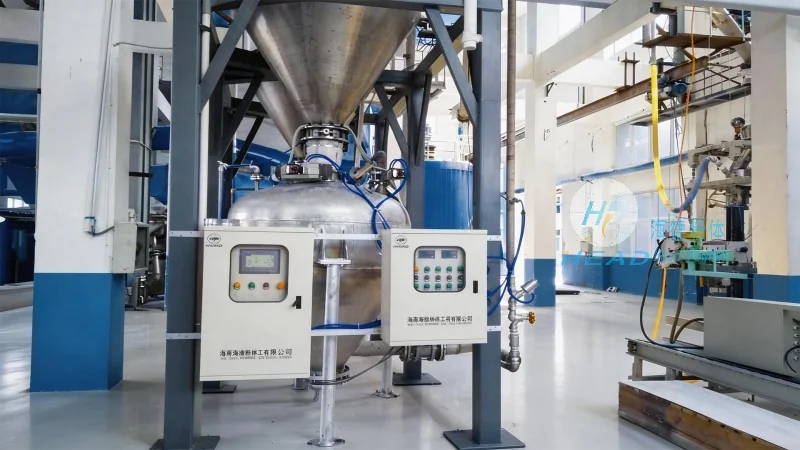
The design of the dusty ash material handling system equipment follows several critical principles to ensure durability, efficiency, and safety. One of the primary design considerations is material compatibility. The equipment is constructed using materials that can withstand the abrasive nature of dusty ash, such as high-strength steel or specialized coatings, to prevent wear and tear over time. Another key principle is the integration of dust control measures. By incorporating efficient dust collection and filtration systems, the design minimizes the release of airborne particles, reducing health risks for workers and environmental impact. Additionally, the system is engineered for easy maintenance and accessibility, with components that can be easily inspected and serviced to ensure long-term reliability. The design also emphasizes energy efficiency, using advanced motor technologies and optimized system layouts to reduce operational costs while maintaining high performance.
Applications and Benefits in Industrial Settings
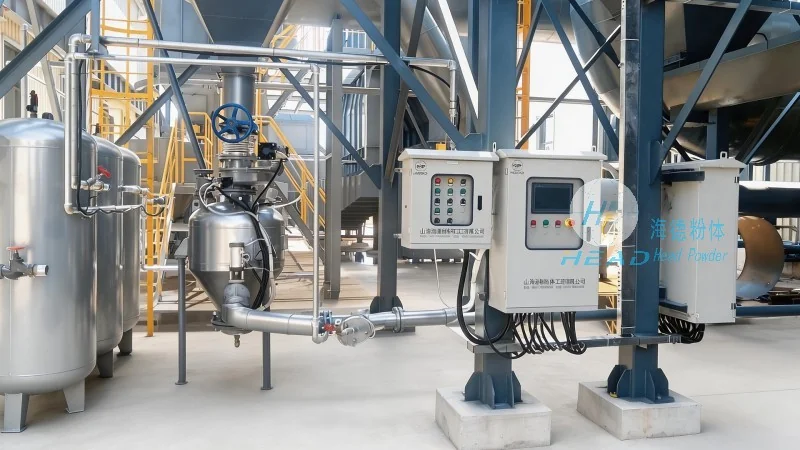
The dusty ash material handling system equipment is widely used in various industrial sectors, including power plants, cement factories, and waste management facilities. In power plants, for example, the system is used to transport fly ash from boilers to storage silos or for further processing. In cement factories, it helps manage the handling of raw materials and byproducts, improving overall production efficiency. The benefits of this system extend beyond just material transport; it enhances workplace safety by reducing exposure to dust, improves environmental compliance by minimizing emissions, and increases operational efficiency through automated and reliable material handling. The system's modular design also allows for easy integration into existing industrial setups, making it a versatile solution for different operational needs.
Customization and Adaptability for Specific Needs
Shandong HeadPowder Engineering Co., Ltd. understands that each industrial facility has unique requirements when it comes to dusty ash handling. Therefore, the company offers customized solutions tailored to specific applications and operational conditions. The system can be adapted to handle different types of dusty materials, varying particle sizes, and different flow rates. Customization options may include adjustments to conveyor speed, dust collection capacity, and control system features to meet the exact needs of the client. This adaptability ensures that the equipment performs optimally in diverse industrial environments, providing a reliable and efficient solution for material handling challenges.
Conclusion and Future Outlook
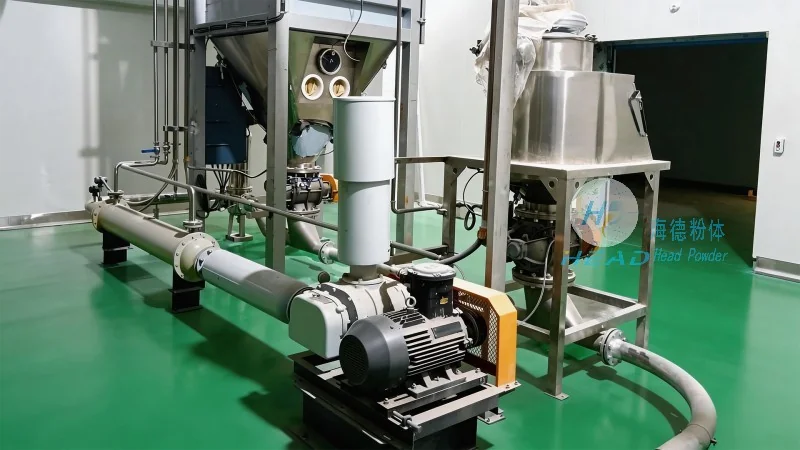
The dusty ash material handling system equipment from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated and reliable solution for industrial facilities dealing with dusty ash and similar materials. By integrating advanced design principles, robust construction, and efficient control systems, the equipment ensures safe, efficient, and environmentally compliant material handling. As industrial demands continue to evolve, the company remains committed to innovation, continuously improving its products to meet the changing needs of the industry. The system's durability, adaptability, and performance make it a valuable asset for any facility seeking to optimize its material handling processes and enhance overall operational efficiency.