Understanding the working principle and characteristics of negative pressure dilute phase material conveying is crucial for industries that rely on efficient and reliable material handling solutions. This article provides a detailed overview of how negative pressure systems operate and the key features that make them effective in various applications.
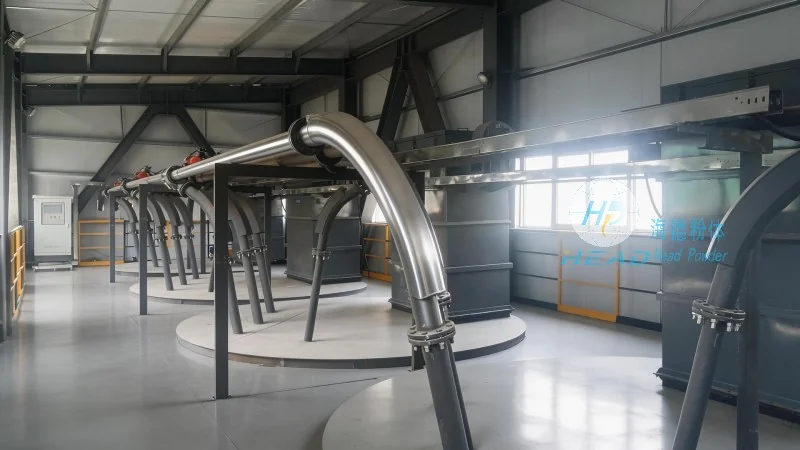
Overview of Negative Pressure Dilute Phase Material Conveying
Negative pressure dilute phase material conveying is a method used to transport powders and granular materials through a pipeline using a vacuum or negative pressure environment. Unlike positive pressure systems that force material through the line, negative pressure systems create a suction effect that draws the material from the source to the destination. This approach is particularly advantageous for applications where dust control, energy efficiency, and low operating costs are critical factors.
The Working Principle of Negative Pressure Dilute Phase Conveying
The core of negative pressure dilute phase material conveying lies in the creation of a pressure differential between the source and the destination. The system typically consists of a vacuum pump that generates a negative pressure in the pipeline, causing the material to be drawn into the line from the hopper or storage bin. As the material is conveyed, it is mixed with a small amount of air, forming a dilute phase stream that travels through the pipeline. The vacuum pump maintains the necessary suction to ensure continuous material flow, while the pipeline design ensures minimal pressure drop and efficient transport.
Key components of a negative pressure dilute phase system include the vacuum pump, inlet and outlet hoppers, pipeline, and any necessary filtration or separation equipment. The vacuum pump is responsible for creating the negative pressure, and its capacity must be matched to the material characteristics, such as particle size, density, and flowability. The pipeline is usually made of materials like stainless steel or plastic, depending on the material being conveyed, to prevent corrosion and material buildup.
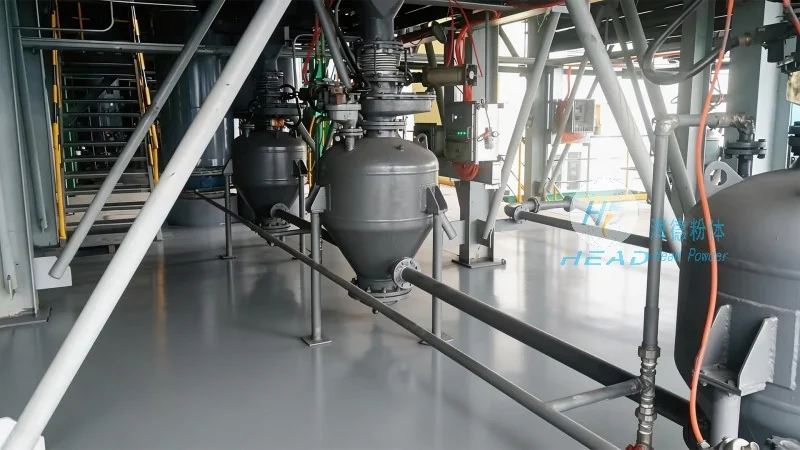
Key Characteristics and Advantages of Negative Pressure Dilute Phase Conveying
One of the primary advantages of negative pressure dilute phase material conveying is its ability to control dust and minimize environmental impact. By drawing material into the system, the process reduces the amount of dust released into the air, making it suitable for applications in pharmaceutical, food, and chemical industries where air quality is a concern. Additionally, negative pressure systems are generally more energy-efficient compared to positive pressure systems, as they require less power to operate due to the suction mechanism.
Another important characteristic is the system's flexibility in handling a wide range of materials. Negative pressure dilute phase conveying can transport materials with varying particle sizes, from fine powders to coarse granules, without the need for extensive modifications to the system. This adaptability makes it suitable for diverse industrial applications, including mining, cement production, and agricultural processing.
The system also offers cost-effective solutions for material transport over moderate distances. By eliminating the need for high-pressure pumps and reducing energy consumption, negative pressure dilute phase conveying can lower operational costs and increase overall efficiency. Furthermore, the design of the system allows for easy integration with existing facilities, making it a practical choice for retrofitting or expanding material handling capabilities.
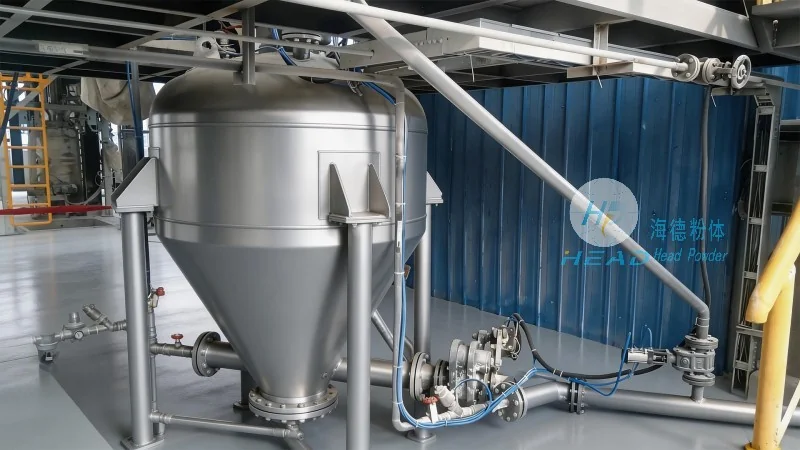
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of material handling solutions specializing in negative pressure dilute phase conveying systems. With a focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for industries seeking reliable and efficient material transport solutions. The company is headquartered in Shandong, China, and serves clients globally with customized systems tailored to their specific needs.
HeadPowder's expertise lies in designing and manufacturing high-quality negative pressure dilute phase conveying systems that meet the stringent requirements of various industries. The company's team of engineers and technicians work closely with clients to understand their material handling challenges and develop solutions that optimize performance, reduce costs, and enhance safety. By leveraging advanced technology and rigorous quality control processes, HeadPowder ensures that its systems deliver consistent and reliable results, helping clients improve their operational efficiency and productivity.
HeadPowder's commitment to excellence is reflected in its comprehensive service offerings, which include system design, installation, maintenance, and technical support. The company provides ongoing assistance to clients to ensure that their negative pressure dilute phase conveying systems operate at peak performance, minimizing downtime and maximizing material throughput. With a strong presence in the market and a reputation for quality and reliability, HeadPowder continues to be a preferred choice for businesses seeking advanced material handling solutions.




