For industries dealing with sand, gravel, and other fine powders, efficient material handling is crucial. Pneumatic conveying systems offer a reliable solution for transporting these materials over short to medium distances. This article explores the working principle and key features of sand and gravel powder pneumatic conveying systems, highlighting their applications and benefits.
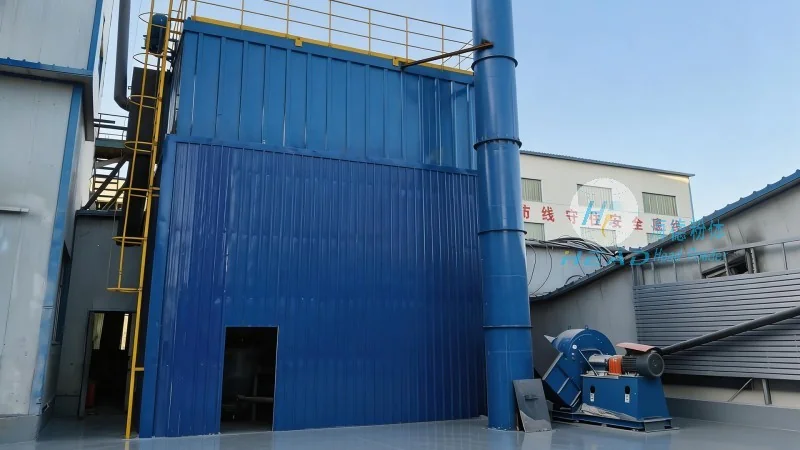
Working Principle of Sand and Gravel Powder Pneumatic Conveying Systems
The core of a pneumatic conveying system is the use of air to transport solid particles. In sand and gravel applications, these systems typically operate under either positive pressure (pressure conveying) or negative pressure (vacuum conveying). Pressure conveying involves blowing air through a pipeline at a high velocity, creating a flow that carries the powder. The system includes a blower, a hopper for material storage, and a pipeline network. As air moves through the pipe, it entrains the sand or gravel particles, forming a dense phase or dilute phase flow. The design of the system, including the blower capacity and pipeline layout, is critical to ensure stable and efficient transport. The process begins with loading the material into the hopper, where it is then drawn into the pipeline by the moving air. This method is particularly effective for transporting materials from a central storage area to processing units or storage locations.
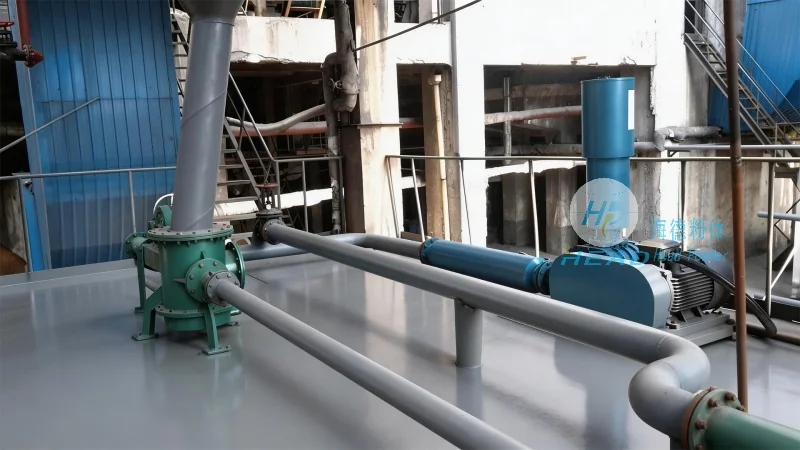
Key Features of Sand and Gravel Powder Pneumatic Conveying Systems
Several distinct features make pneumatic conveying systems suitable for sand and gravel applications. First, they provide a closed system, which helps prevent dust contamination and environmental pollution. This is especially important in industries where dust control is a regulatory requirement. Second, these systems offer high transport efficiency, with the ability to move large volumes of material over significant distances with minimal energy loss. The flexibility of the pipeline layout allows for easy integration into existing production lines or new facility designs. Another notable feature is the reduced need for manual handling, which enhances workplace safety and reduces labor costs. Additionally, pneumatic conveying systems can handle a wide range of particle sizes and moisture contents, making them versatile for various sand and gravel processing operations. The systems are also designed for durability, with components that can withstand the abrasive nature of these materials, ensuring long-term reliability.
Applications and Benefits in Industrial Settings
Sand and gravel powder pneumatic conveying systems are widely used in construction, mining, and manufacturing sectors. In construction, they are essential for transporting sand and gravel from quarries to mixing plants or job sites. The systems ensure consistent material quality and reduce downtime associated with traditional truck or belt conveyors. In mining operations, these systems help move crushed gravel and fine powders from processing units to storage or further treatment facilities. The benefits extend to manufacturing industries, where precise material delivery is critical for quality control. The closed-loop design minimizes material loss and contamination, which is vital for producing high-quality products. Furthermore, the energy efficiency of modern pneumatic conveying systems contributes to lower operational costs, making them a cost-effective solution for long-term material handling needs.
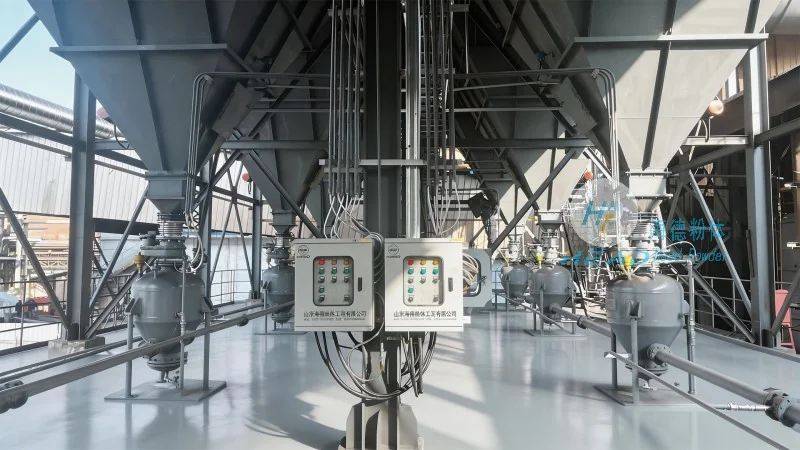
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. With a focus on innovation and customer satisfaction, the company has established itself as a leading provider in the industry. HeadPowder's expertise lies in tailoring systems to meet the specific requirements of sand and gravel processing applications. The company's team of engineers and technicians works closely with clients to understand their operational needs, ensuring that the final system is both efficient and reliable. HeadPowder's facilities in Shandong, China, are equipped with state-of-the-art technology and quality control measures, guaranteeing that each system meets international standards. The company's commitment to sustainability and environmental responsibility is reflected in the design of its systems, which minimize energy consumption and reduce emissions. Clients benefit from HeadPowder's comprehensive service, including system design, installation, and after-sales support, ensuring a seamless integration into their existing operations.




