Warehouse bottom air conveying systems represent a sophisticated solution for material handling within industrial and logistics environments. These systems leverage compressed air to transport bulk materials, powders, and granules efficiently from one location to another, often with minimal human intervention. The technology is particularly well-suited for applications where traditional conveyor systems may face challenges due to space constraints, material properties, or operational requirements.
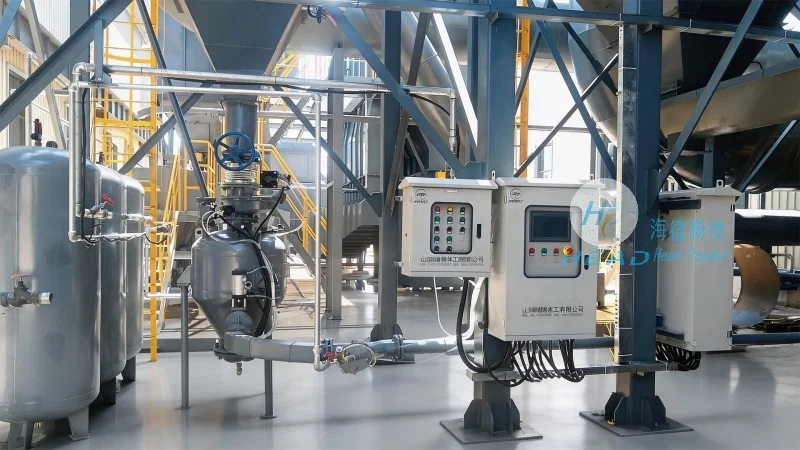
The Core Principle of Air Conveying Technology
The fundamental principle behind warehouse bottom air conveying systems is the use of differential air pressure to create a flow of material through a network of pipes. Compressed air is introduced into the system, typically at the discharge end, creating a pressure differential that propels the material forward. The system often incorporates a combination of positive and negative pressure zones to optimize material movement and minimize energy consumption. This approach allows for flexible routing of material flow, enabling complex layouts that adapt to the specific needs of a warehouse or production facility.
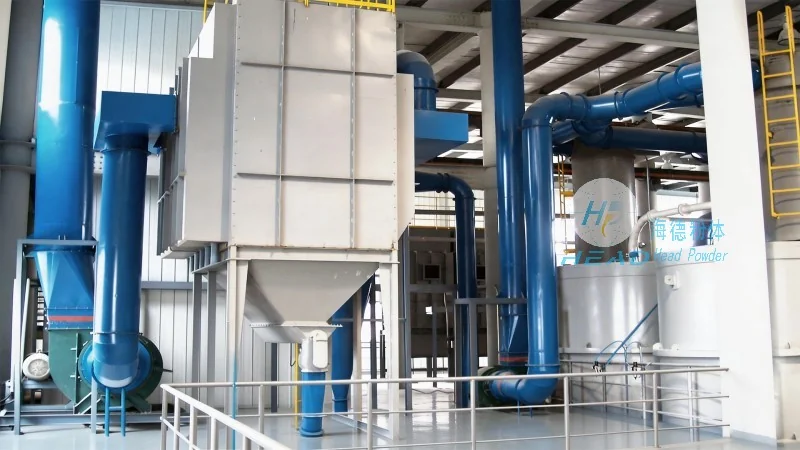
Key Working Scene Characteristics and Applications
Warehouse bottom air conveying systems excel in various working scenarios, including high-volume material transfer in manufacturing plants, bulk material handling in chemical and food processing industries, and inventory management in distribution centers. The systems are particularly effective for transporting fine powders, such as cement, flour, or pharmaceutical powders, where traditional methods may cause dust or contamination. Additionally, they are well-suited for applications requiring gentle material handling, as the air flow minimizes product degradation and ensures consistent quality. The flexibility of the system allows it to integrate seamlessly with existing infrastructure, reducing the need for extensive reconfiguration or new construction.
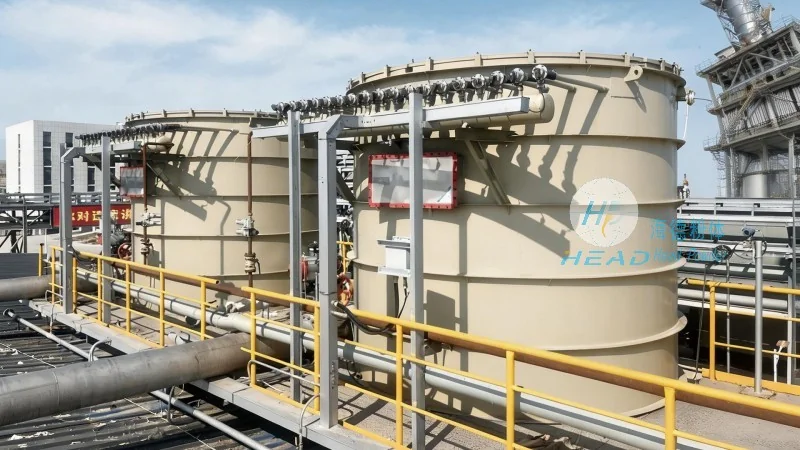
Technical Advantages and Practical Benefits
One of the primary advantages of warehouse bottom air conveying systems is their ability to handle a wide range of material types and sizes with minimal maintenance. The system's design minimizes mechanical components, reducing wear and tear and extending operational life. This results in lower long-term costs and increased reliability compared to traditional conveyor systems. Furthermore, the systems are highly adaptable, allowing for adjustments to material flow rates and routing without significant modifications. The quiet operation of air conveying systems also contributes to a safer and more comfortable working environment, particularly in facilities where noise levels are a concern. Additionally, the systems can be integrated with automation controls, enabling real-time monitoring and optimization of material handling processes.
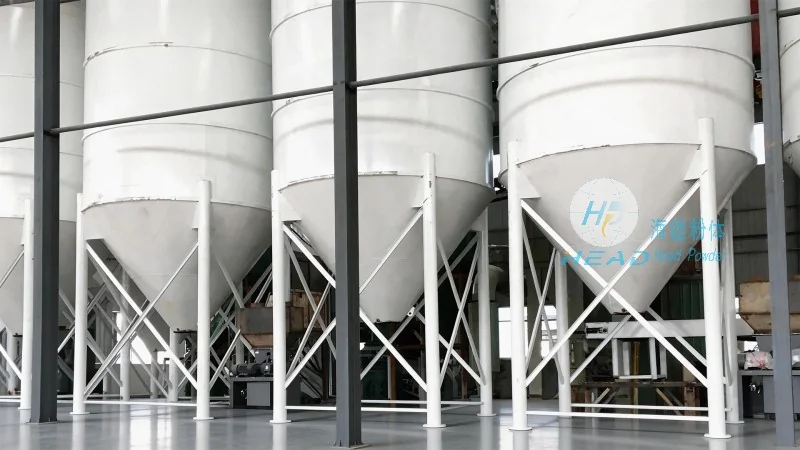
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading provider of advanced material handling solutions, specializing in the design, manufacturing, and installation of warehouse bottom air conveying systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner in the industrial sector. HeadPowder's headquarters is located in Shandong, China, where the company leverages local expertise and resources to deliver high-quality products tailored to the unique needs of its clients. The company's team of experienced engineers and technicians ensures that each system is customized to meet specific operational requirements, guaranteeing optimal performance and reliability. HeadPowder's dedication to quality and customer service has earned it a reputation for excellence in the industry, making it a preferred choice for businesses seeking efficient and reliable material handling solutions.




