HeadPowder, a leading provider of advanced powder handling solutions, specializes in intelligent powder transport systems designed to optimize material flow in industrial applications. The company, based in Shandong, China, leverages cutting-edge technology to deliver efficient, reliable, and safe powder handling systems tailored to diverse operational needs.
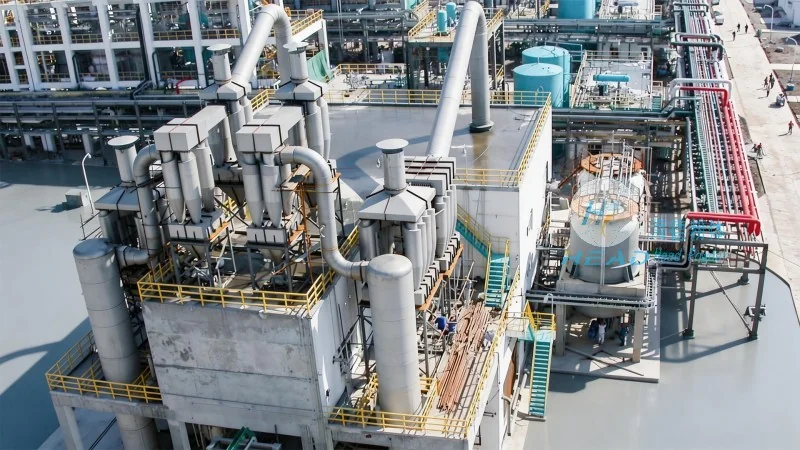
Core Principles of Intelligent Powder Handling Systems
The intelligent powder handling system operates on fundamental principles that ensure precise and controlled movement of powders. These systems typically utilize negative pressure (vacuum) or positive pressure (compressed air) to draw or push powders through pipelines. Advanced sensors and control algorithms monitor flow rates, pressure, and material density in real-time, enabling dynamic adjustments to maintain optimal performance. The integration of IoT (Internet of Things) technology allows for remote monitoring and data analytics, enhancing system efficiency and predictive maintenance capabilities.
Key Working Scene Characteristics
Intelligent powder handling systems are widely applied in various industrial sectors, each presenting unique challenges and requirements. In the chemical industry, for instance, these systems are crucial for transporting reactive powders with strict safety protocols. The systems’ ability to handle high-purity materials and prevent contamination is a critical feature. In pharmaceutical manufacturing, precision and sterility are paramount, making intelligent systems ideal for handling active pharmaceutical ingredients (APIs) and excipients. The systems’ modular design allows for easy integration into existing production lines, reducing downtime and increasing overall productivity.
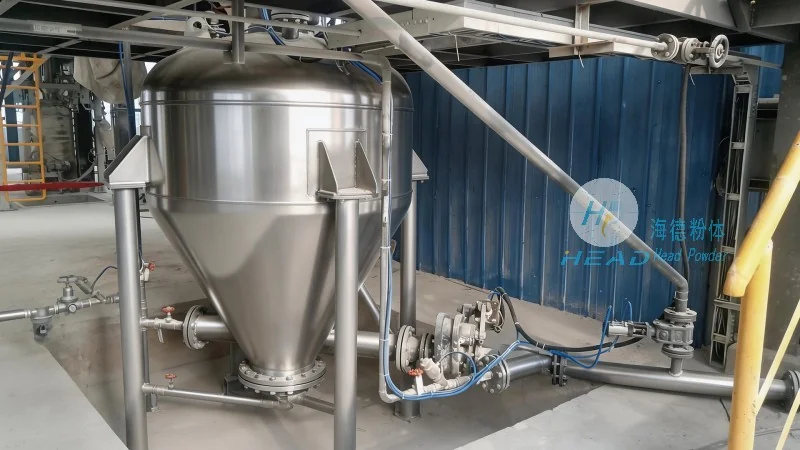
Advantages in Industrial Applications
Compared to traditional manual or semi-automated powder handling methods, intelligent powder transport systems offer significant advantages. The automated control reduces human error, minimizes material waste, and enhances safety by eliminating direct contact with powders. Real-time data collection provides insights into system performance, enabling proactive maintenance and extending equipment lifespan. The scalability of these systems allows businesses to expand their operations without significant infrastructure changes, making them a cost-effective solution for growing enterprises. Additionally, the energy-efficient design of modern systems contributes to lower operational costs and aligns with sustainability goals.
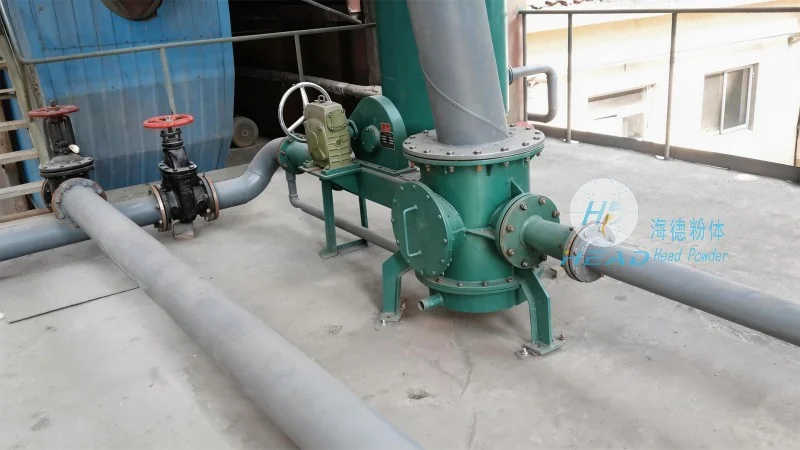
Customization and Integration Capabilities
HeadPowder’s intelligent powder handling systems are highly customizable to meet specific client requirements. The company offers tailored solutions that integrate seamlessly with existing production processes, ensuring minimal disruption during implementation. Clients can choose from a range of components, including different types of pumps, filters, and control panels, to suit their operational needs. The systems are designed to be compatible with various powder types, from fine powders like talc to bulk materials like cement, demonstrating versatility across industries. The company’s technical team provides comprehensive support, from system design and installation to ongoing maintenance and troubleshooting, ensuring long-term reliability and client satisfaction.
Future Trends and Innovation
As technology advances, intelligent powder handling systems continue to evolve, incorporating new features to enhance performance. The integration of artificial intelligence (AI) and machine learning (ML) enables predictive analytics, allowing systems to anticipate potential issues and optimize operational parameters. Smart sensors and IoT connectivity enable remote monitoring and automated adjustments, further improving efficiency. The focus on sustainability drives the development of energy-efficient systems and materials that reduce environmental impact. HeadPowder remains at the forefront of these innovations, continuously investing in research and development to deliver cutting-edge solutions that meet the evolving needs of industrial clients.




