HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of fine sand and gravel material conveying equipment. The company's products are engineered to meet the specific demands of various industrial applications, ensuring efficient material handling and processing.
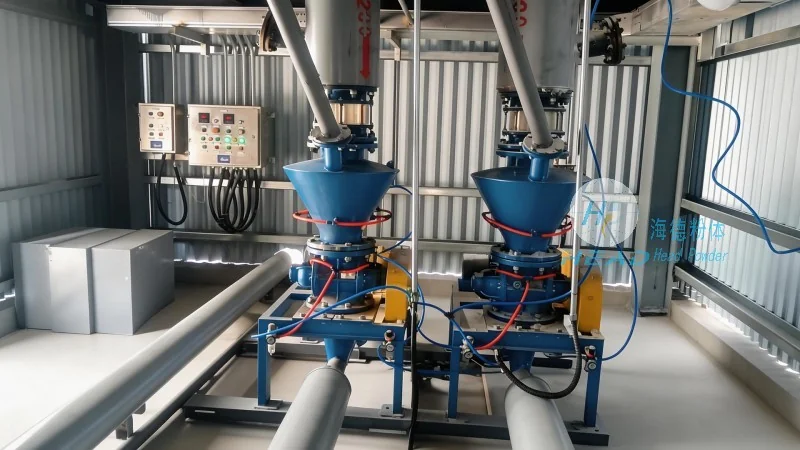
Overview of Fine Sand and Gravel Material Conveying Equipment
Fine sand and gravel material conveying equipment is a critical component in many industrial processes, particularly in the construction, mining, and aggregate processing sectors. These systems are designed to transport fine sand, gravel, and similar granular materials from one location to another with precision and reliability. The equipment typically includes components such as feeders, conveyors, and control systems, all working in tandem to ensure smooth material flow.
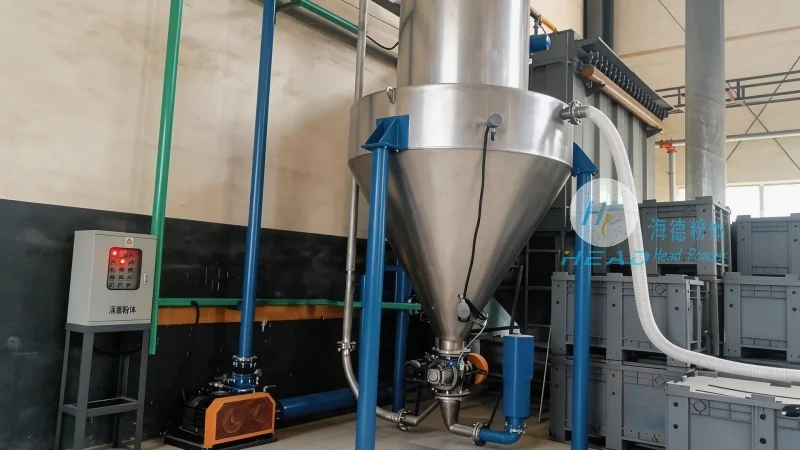
Working Principle of the Conveying Equipment
The core principle behind fine sand and gravel material conveying equipment is the mechanical transfer of bulk materials. The system often utilizes a combination of gravity, mechanical force, and sometimes pneumatic assistance to move the material. For instance, screw conveyors use rotating screws to push the material forward, while belt conveyors rely on the friction between the belt and the material to achieve transport. In some advanced systems, vibration or air pressure may be employed to enhance material movement, especially for fine particles that are prone to clogging or sticking. The control system monitors parameters like speed, pressure, and material level to maintain optimal operation and prevent downtime.
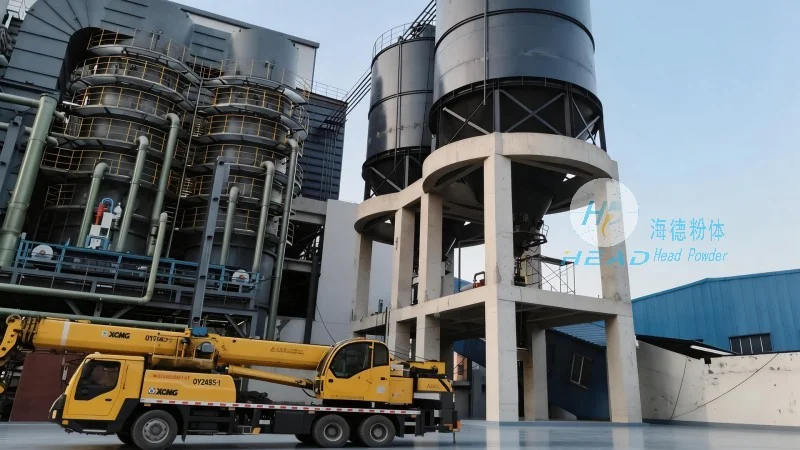
Key Features and Technical Specifications
HeadPowder's conveying equipment is equipped with several key features that enhance performance and durability. These include robust construction to withstand heavy loads and abrasive materials, adjustable speed controls for precise material flow, and integrated safety mechanisms to prevent accidents. The equipment is also designed for easy maintenance, with accessible components that allow for quick repairs and replacements. Technical specifications vary based on the specific application, but common features include high efficiency, low energy consumption, and the ability to handle a wide range of particle sizes and moisture content.
Working Scene Characteristics and Applications
The working scene characteristics of fine sand and gravel material conveying equipment are tailored to meet the diverse needs of different industries. In mining operations, the equipment is used to transport ore and gravel from extraction sites to processing facilities, ensuring a continuous supply of raw materials. In construction sites, it facilitates the movement of sand and gravel for concrete mixing and foundation work, improving productivity and reducing manual labor. In aggregate processing plants, the equipment plays a crucial role in sorting, cleaning, and transporting materials, contributing to higher quality end products. The adaptability of these systems allows them to operate in various environmental conditions, from indoor processing facilities to outdoor mining sites, making them versatile solutions for material handling challenges.
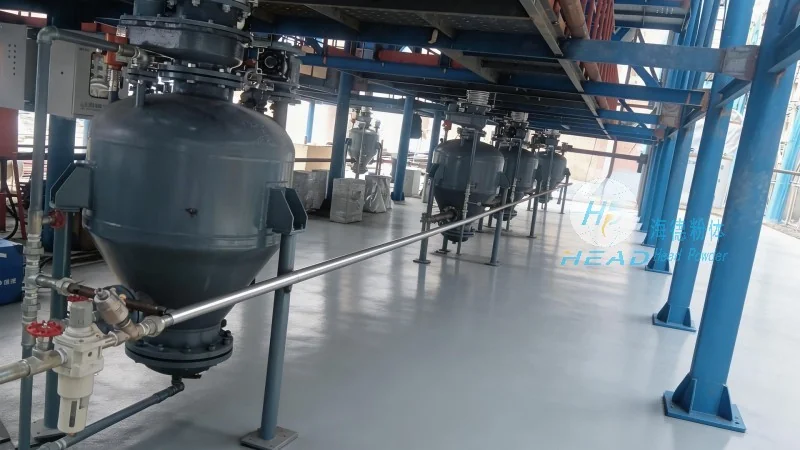
Advantages in Industrial Applications
Implementing fine sand and gravel material conveying equipment offers several advantages in industrial settings. Firstly, it significantly improves operational efficiency by automating the material transport process, reducing the time and labor required for manual handling. Secondly, it enhances safety by minimizing the need for workers to handle heavy or hazardous materials directly. Thirdly, the equipment's ability to handle large volumes of material at a consistent rate reduces bottlenecks in production lines, leading to increased output. Additionally, the precise control over material flow helps in maintaining quality standards, as it prevents overloading or underloading of processing equipment. These advantages make the equipment a valuable investment for businesses looking to optimize their material handling processes.




