HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dust-free automatic bulk material pneumatic conveying systems. These systems represent a sophisticated solution for transporting dry powders and granules in industries where maintaining a clean environment is paramount. This article delves into the fundamental principles behind such systems and highlights the key characteristics of their operational scenarios.
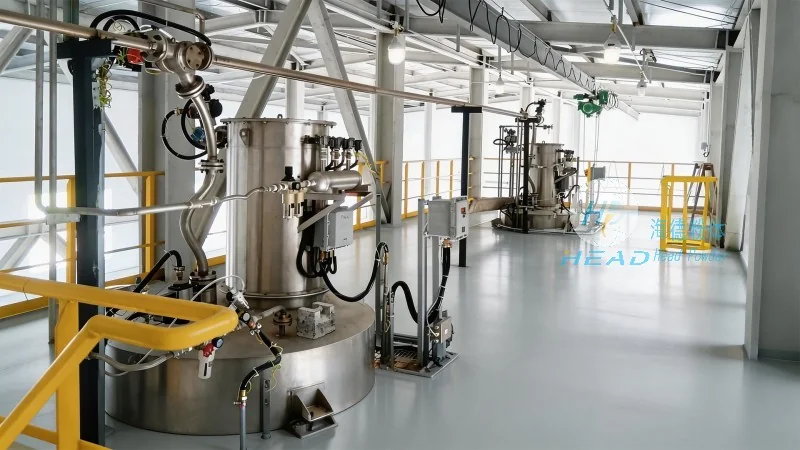
Principle of Dust-Free Automatic Pneumatic Conveying Systems
The core principle of dust-free automatic pneumatic conveying systems is the use of compressed air or gas to transport bulk materials through a sealed pipeline network. Unlike traditional mechanical conveying methods, which rely on moving parts like belts or screws, pneumatic systems utilize air pressure to move materials, minimizing contamination and ensuring a clean transfer process. The system typically consists of a blower, a hopper for material storage, a conveying line, and a receiver for the delivered material. The compressed air is introduced into the hopper, creating a pressure differential that draws the material into the pipeline. As the air and material mixture travels through the sealed system, the material is carried to the destination, where it is separated from the air and collected. This process is highly efficient and can handle a wide range of materials, from fine powders to coarse granules, while maintaining strict dust control.
Key Working Scene Characteristics
The operational characteristics of dust-free automatic pneumatic conveying systems are tailored to meet the specific demands of various industrial applications. These systems are particularly well-suited for environments where dust generation must be minimized, such as pharmaceutical, food processing, and chemical manufacturing facilities. The sealed design of the system prevents material leakage and air contamination, ensuring compliance with stringent regulatory standards. In pharmaceutical applications, for example, the system can transport active pharmaceutical ingredients (APIs) and excipients while maintaining a sterile and dust-free environment, which is critical for product quality and safety. Similarly, in food processing, the system can handle ingredients like flour, sugar, and spices without cross-contamination, preserving product integrity and meeting food safety regulations.
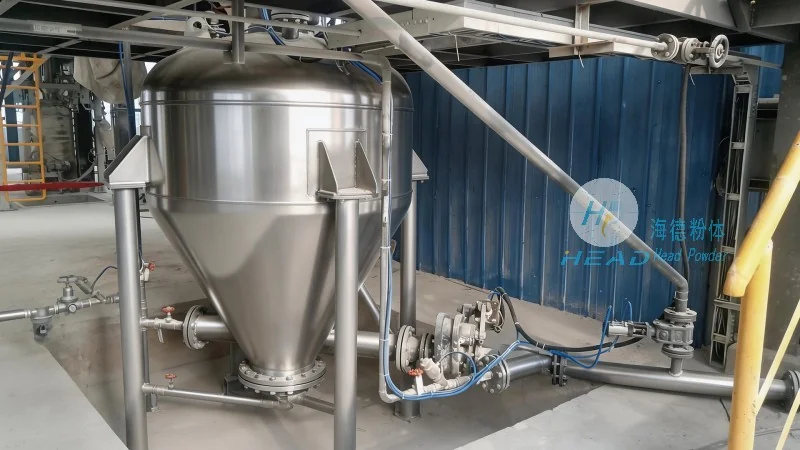
Another key characteristic is the system's adaptability to different material properties. The design allows for the conveyance of materials with varying flowability, moisture content, and particle sizes. This flexibility makes the system suitable for diverse operational scenarios, including short-distance and long-distance transfers. For instance, in a chemical plant, the system can transport raw materials from storage silos to processing units over several hundred meters, while maintaining consistent flow rates and preventing material degradation. In smaller-scale applications, such as in a food processing plant, the system can efficiently move ingredients between processing stages, reducing labor costs and improving production efficiency.
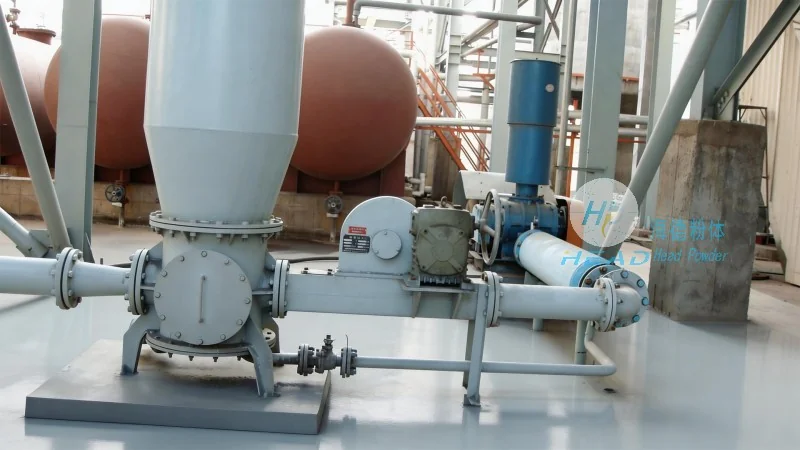
Advantages in Industrial Applications
The implementation of dust-free automatic pneumatic conveying systems offers several advantages that enhance operational performance and product quality. One of the primary benefits is the reduction of dust-related hazards, which not only improves workplace safety but also minimizes the risk of product contamination. By eliminating the need for manual handling of powders, the system reduces the likelihood of human error and improves overall process reliability. Additionally, the automated nature of the system allows for precise control over material flow rates and pressure, ensuring consistent delivery to downstream processes. This precision is crucial in industries where material consistency directly impacts product quality, such as in the production of pharmaceuticals or high-value food products.
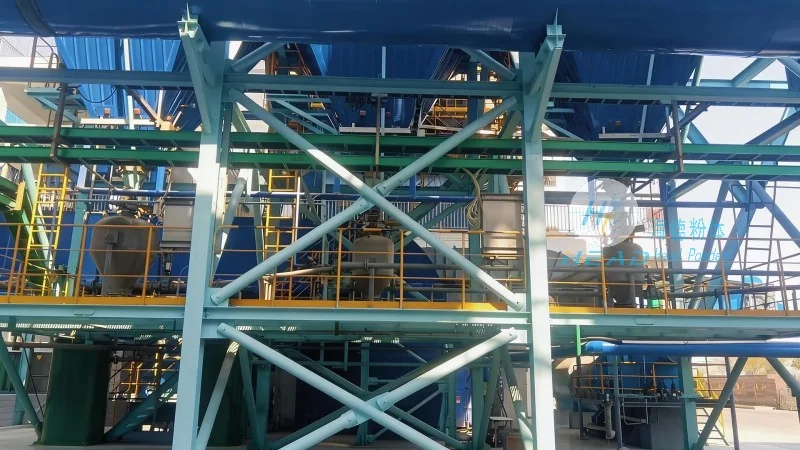
Furthermore, the sealed and enclosed design of the system reduces energy consumption compared to open-air conveying methods. The air is recirculated within the system, minimizing waste and lowering operational costs. This energy efficiency, combined with the system's low maintenance requirements, makes it a cost-effective solution for long-term industrial use. The system's modular design also allows for easy integration with existing production lines, enabling companies to upgrade their material handling processes without significant disruptions.
Conclusion
HeadPowder's dust-free automatic bulk material pneumatic conveying systems exemplify advanced engineering solutions for modern industrial needs. By combining the principles of pneumatic transport with strict dust control measures, these systems provide efficient, reliable, and safe material handling capabilities. The working scene characteristics, tailored to various industries, highlight the system's versatility and adaptability. As a manufacturer based in Shandong, China, HeadPowder continues to innovate in this field, delivering high-quality products that meet the evolving demands of global industries. The systems not only enhance operational efficiency but also contribute to maintaining the highest standards of product purity and workplace safety.




