Automatic bulk material pneumatic conveying equipment, as a core solution in modern material handling, plays a crucial role in improving production efficiency and ensuring operational safety. This equipment is designed to transport bulk materials such as powders, granules, and fine particles through a closed pipeline system using air pressure or vacuum. The technology not only enhances the flexibility and scalability of material transport but also reduces labor costs and environmental pollution compared to traditional methods like belt conveyors or manual handling.
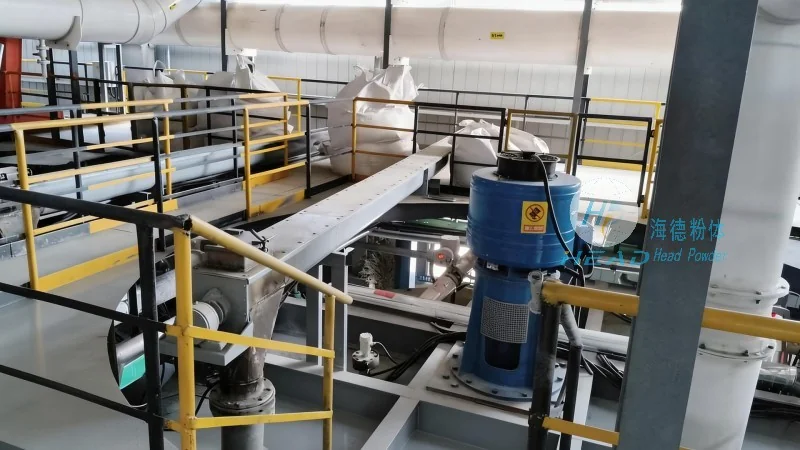
Core Principles of Pneumatic Conveying Systems
The fundamental principle of pneumatic conveying is to use the pressure difference between the conveying pipeline and the ambient environment to drive material movement. There are two main types of pneumatic conveying systems: pressure conveying and vacuum conveying. Pressure conveying operates by injecting high-pressure air into the material container, forcing the material to flow along the pipeline under the pressure of compressed air. Vacuum conveying, on the other hand, creates a negative pressure in the pipeline by extracting air, which draws the material into the system. The selection of the appropriate conveying type depends on factors such as material properties, transport distance, and system layout. For example, pressure conveying is more suitable for long-distance and high-volume transport, while vacuum conveying is ideal for short-distance and low-volume applications, especially for materials that are sensitive to pressure or require gentle handling.
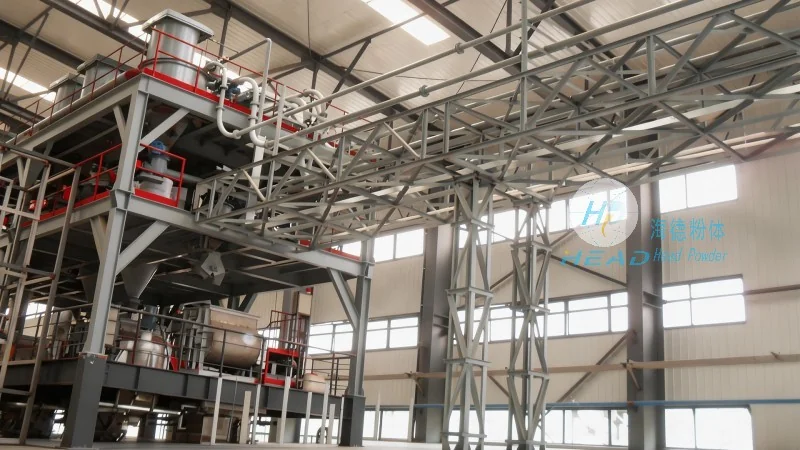
Key Working Scene Characteristics and Applications
The working scene characteristics of automatic bulk material pneumatic conveying equipment are diverse and tailored to different industrial needs. In the chemical industry, this equipment is widely used for transporting powders like calcium carbonate, titanium dioxide, and various chemical additives, ensuring stable and clean material transfer in production lines. In the food industry, it is employed for conveying ingredients such as flour, sugar, and spices, maintaining hygiene standards and preventing cross-contamination. The equipment also finds extensive applications in the pharmaceutical industry, where it handles active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination risk. Additionally, in the mining and construction sectors, it is used for transporting raw materials like coal, ore, and cement, improving the efficiency of material handling in large-scale projects. The adaptability of the system allows it to be integrated into various production environments, from small-scale workshops to large industrial plants, making it a versatile solution for different working scenarios.
Technical Advantages and Operational Efficiency
Automatic bulk material pneumatic conveying equipment offers several technical advantages that make it a preferred choice in modern industrial applications. One of the key benefits is its high efficiency in material transport. The system can achieve rapid and continuous material movement, reducing the time required for material transfer and increasing overall production throughput. For instance, in a chemical plant, the equipment can transport 10-20 tons of powder per hour, significantly improving the production cycle. Another advantage is the flexibility of the system, which allows for easy adjustment of the conveying parameters, such as air pressure and flow rate, to accommodate different material types and transport requirements. This adaptability ensures optimal performance under various conditions. Furthermore, the equipment is designed with a closed pipeline system, which helps to prevent material leakage and environmental pollution, maintaining a clean and safe working environment. The use of advanced materials and components in the construction of the equipment enhances its durability and longevity, reducing maintenance costs and downtime. Overall, the technical advantages of this equipment contribute to improved operational efficiency and cost-effectiveness in industrial settings.
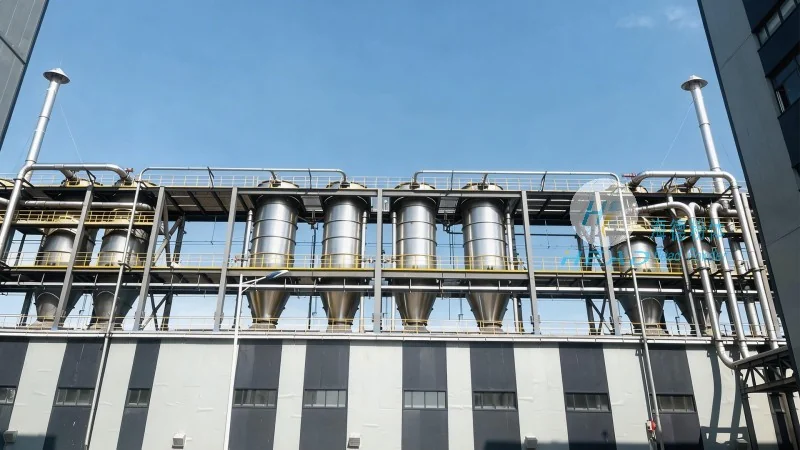
Company Profile and Professional Support
HeadPowder, as a professional manufacturer of automatic bulk material pneumatic conveying equipment, is committed to providing high-quality and reliable solutions for various industrial needs. The company, Shandong HeadPowder Engineering Co., Ltd., is located in Shandong, China, with a strong R&D team and advanced manufacturing facilities. HeadPowder focuses on the research and development of pneumatic conveying technology, continuously improving product performance and expanding application fields. The company's products are designed to meet the specific requirements of different industries, ensuring stable and efficient material transport. HeadPowder provides comprehensive technical support and after-sales service, helping customers optimize their production processes and achieve better results. With years of experience in the industry, HeadPowder has established a good reputation for its quality products and professional service, making it a trusted partner for customers worldwide.




