Red bean powder conveying systems are specialized equipment designed to transport red bean powder efficiently and safely. These systems are crucial in industries where red bean powder is processed, stored, or used in various applications. Understanding the components and design principles of such systems is essential for optimizing workflow and ensuring product quality.
Introduction to Red Bean Powder Conveying Systems
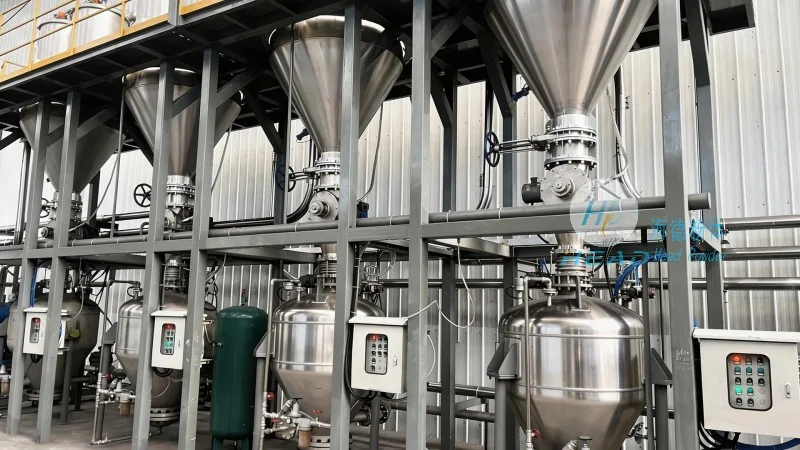
Red bean powder, a popular ingredient in many food products and traditional medicines, requires careful handling due to its fine particle size and potential for dust generation. A red bean powder conveying system addresses these challenges by providing a controlled environment for material movement. The system typically includes components like hoppers, feeders, conveyors, and control mechanisms, all working in tandem to ensure smooth and reliable transport.
Company Overview: HeadPowder
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer in the field of powder handling equipment. With headquarters in Shandong, China, the company specializes in designing and producing advanced conveying systems tailored to the unique needs of various industries. HeadPowder's expertise lies in creating solutions that enhance productivity while maintaining high standards of safety and efficiency.
Design Principles of Red Bean Powder Conveying Systems
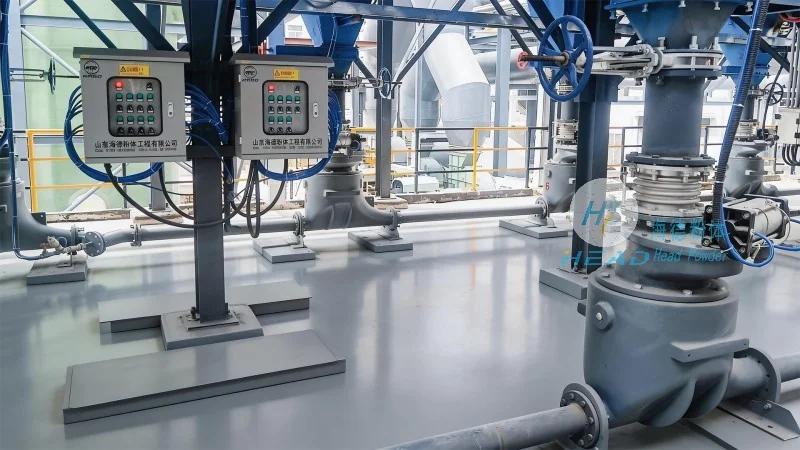
The design of a red bean powder conveying system is based on several key principles to ensure optimal performance. First, the system must handle the specific properties of red bean powder, such as its fine particle size and tendency to agglomerate. This involves using appropriate materials for construction, often stainless steel or other corrosion-resistant metals, to prevent contamination and ensure durability. Second, the system incorporates dust control measures, including sealed enclosures and filtration systems, to minimize airborne dust and comply with environmental regulations.
Third, the conveying mechanism is carefully selected to match the flow characteristics of red bean powder. Common types include pneumatic conveying systems, which use air to move powder through pipes, and mechanical conveyors like screw conveyors or belt conveyors. The choice of mechanism depends on factors such as the volume of material, distance to be conveyed, and the need for gentle handling to avoid particle breakage. For red bean powder, a pneumatic system is often preferred as it can handle fine powders without causing excessive wear on components.
Key Components and Their Functions
A typical red bean powder conveying system consists of several interconnected parts, each playing a vital role in the overall operation. The hopper is the first component, where red bean powder is stored before being fed into the system. It is designed to hold a sufficient quantity of material and often includes a discharge valve to control the flow rate. The feeder, usually a rotary valve or a vibratory feeder, regulates the amount of powder entering the conveyor, ensuring a consistent and controlled feed.
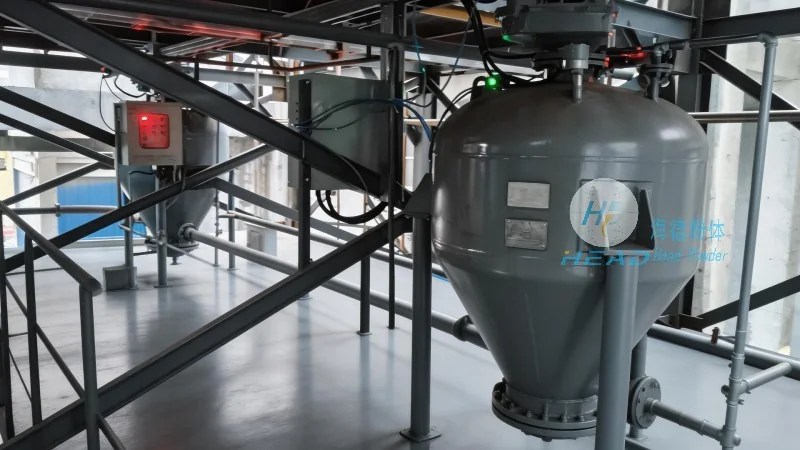
The conveyor itself is the core of the system, responsible for transporting the powder from the feeder to the destination. In pneumatic systems, this is achieved through a series of pipes and a blower that generates the necessary air pressure. The blower draws the powder into the pipe and propels it to the outlet. Mechanical conveyors, on the other hand, use rotating screws or belts to move the powder along a path. The design of the conveyor, including its speed and inclination, is critical to prevent material buildup and ensure smooth flow.
The control system is another essential component, which monitors and regulates the operation of the conveying system. It includes sensors to detect the level of powder in the hopper and the flow rate, as well as controls to adjust the speed of the blower or the feeder. This ensures that the system operates efficiently and safely, preventing overloading or underloading that could lead to system failure or product contamination.
Benefits and Applications
Implementing a red bean powder conveying system offers numerous benefits for businesses. Firstly, it improves productivity by automating the material handling process, reducing the need for manual labor and minimizing downtime. Secondly, it enhances safety by containing dust and preventing exposure to workers, which is crucial in industries where red bean powder can cause respiratory issues. Thirdly, it maintains product quality by ensuring gentle handling and preventing contamination from external sources.
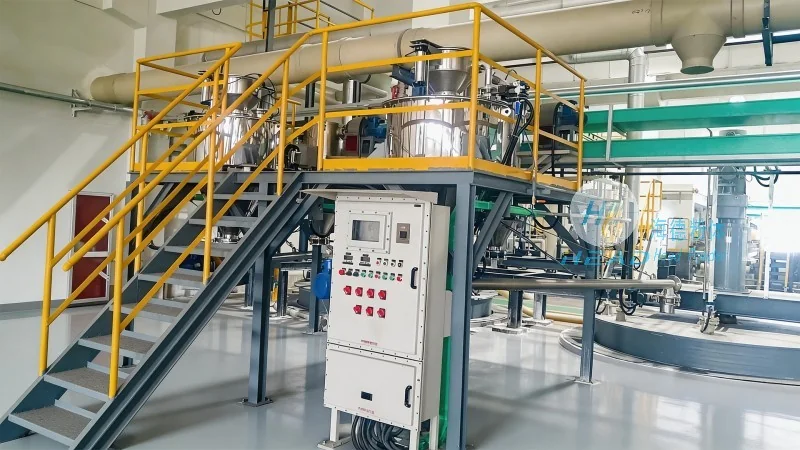
Red bean powder conveying systems are widely used in various industries, including food processing, pharmaceuticals, and cosmetics. In food processing, they are used to transport red bean powder from storage to production lines for making products like red bean paste, drinks, and snacks. In pharmaceuticals, they help in the handling of red bean-based medicinal powders, ensuring that the final product is of high quality and free from contaminants. The versatility of these systems makes them suitable for a wide range of applications where fine powders need to be transported efficiently.
Conclusion
Red bean powder conveying systems are sophisticated pieces of equipment that play a vital role in industries dealing with fine powders. By understanding the design principles and components of such systems, businesses can select the most appropriate solution to meet their specific needs. HeadPowder, with its expertise and commitment to quality, offers reliable and efficient conveying systems that enhance productivity and ensure product safety. Whether for food processing or pharmaceutical applications, a well-designed red bean powder conveying system is an investment that pays off in terms of efficiency, safety, and product quality.




