Stone aggregate powder conveying equipment is a specialized system designed to transport bulk materials such as stone aggregates, powders, and granular substances efficiently and reliably. These systems are crucial in various industrial applications, including construction, mining, and material processing, where the seamless movement of raw materials is essential for operational efficiency and productivity. Understanding the design principles behind these equipment is vital for optimizing performance and ensuring safe, effective material handling.
Overview of Stone Aggregate Powder Conveying Equipment
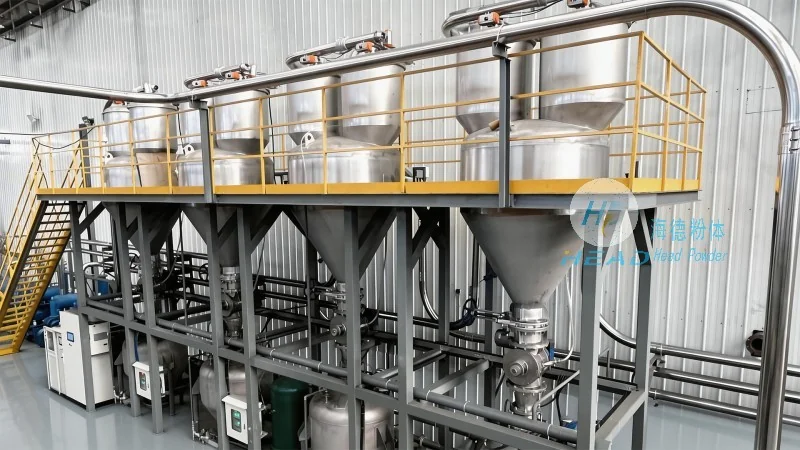
Stone aggregate powder conveying equipment, often referred to as bulk material handling systems, encompasses a range of machinery and components engineered to move loose materials from one location to another. The primary goal of these systems is to facilitate the transfer of materials with minimal loss, reduced dust generation, and optimal energy efficiency. The equipment typically includes components like hoppers, feeders, conveyors, and control systems, all working in tandem to achieve the desired material flow. HeadPowder, a leading manufacturer in this field, specializes in designing and supplying high-quality conveying solutions tailored to meet the specific needs of clients in the construction and industrial sectors.
Key Components and Their Functions
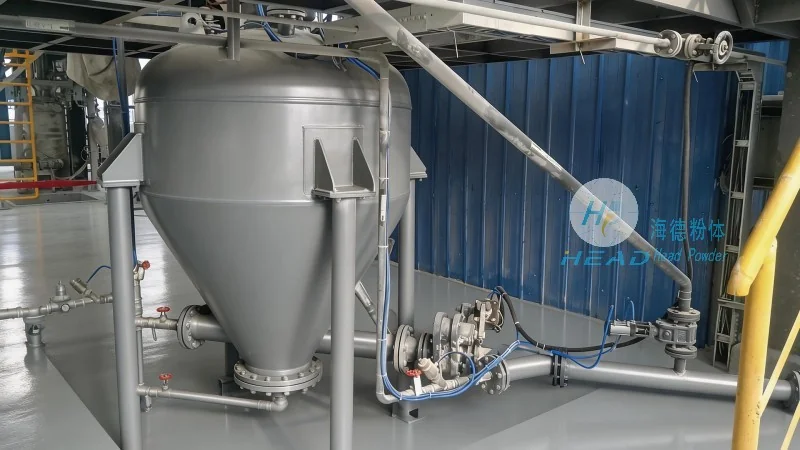
The design of stone aggregate powder conveying equipment relies on several critical components, each playing a specific role in the overall material handling process. The first component is the hopper, which serves as the storage and feeding unit for the bulk material. Hoppers are designed with appropriate dimensions and angles to prevent material bridging and ensure smooth discharge. The feeder, often a rotary or vibratory type, regulates the flow rate of the material into the conveyor system, preventing overloading and maintaining consistent material throughput. The conveyor itself, which can be a belt, screw, or pneumatic type, is responsible for transporting the material from the source to the destination. For stone aggregates and powders, screw conveyors are commonly used due to their ability to handle abrasive materials and maintain a consistent flow. The control system, which includes sensors and automation devices, monitors the operation of the equipment, ensuring safety and optimizing performance by adjusting parameters such as speed and pressure.
Design Principles for Efficient Material Handling
The design principles of stone aggregate powder conveying equipment are centered around several key factors that ensure efficiency, reliability, and safety. One of the primary principles is the minimization of material degradation and loss during transport. This is achieved through the use of appropriate materials for the conveyor components, such as corrosion-resistant metals and wear-resistant coatings, which can withstand the abrasive nature of stone aggregates and powders. Another critical principle is the prevention of dust generation, which is a significant concern in material handling operations. The equipment is designed with dust containment features, such as sealed hoppers and enclosed conveyor systems, to reduce airborne particles and improve workplace safety. Energy efficiency is also a key design consideration, as the equipment operates continuously and consumes significant power. Manufacturers like HeadPowder incorporate energy-saving technologies, such as variable speed drives and optimized conveyor designs, to reduce operational costs and environmental impact.
Application Examples and Industry Impact
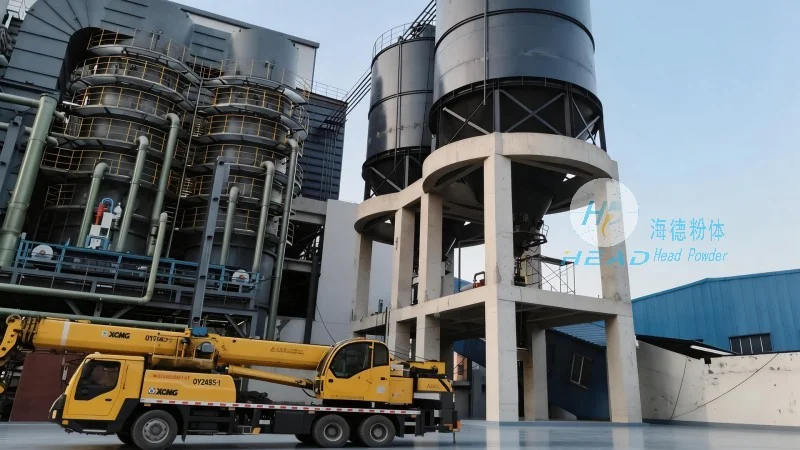
Stone aggregate powder conveying equipment is widely used in various industries, with significant impact on operational efficiency and productivity. In the construction industry, these systems are essential for transporting raw materials like sand, gravel, and cement to construction sites. The ability to handle large volumes of material quickly and reliably reduces downtime and improves project timelines. In the mining sector, the equipment is used to transport ore and other minerals from the mine to processing facilities, ensuring a continuous supply of raw materials for extraction and processing. The industrial sector also benefits from these systems, as they are used to handle a variety of bulk materials, including chemicals, food products, and agricultural materials. The consistent and efficient transport of these materials is crucial for maintaining production schedules and meeting quality standards.
HeadPowder: A Leading Provider of Conveying Solutions
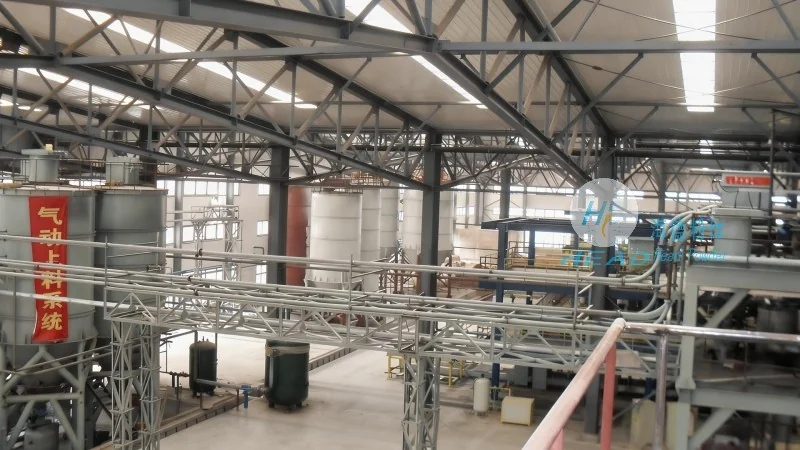
HeadPowder, a prominent company in the material handling industry, is dedicated to providing high-quality stone aggregate powder conveying equipment and related services. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. The company's products are designed based on the latest engineering principles and are manufactured using advanced technologies to ensure durability and performance. HeadPowder's team of experienced engineers and technicians work closely with clients to understand their specific requirements and develop customized solutions that meet their needs. The company's facilities are located in Shandong, China, where it has a strong presence in the industry and access to a skilled workforce and advanced manufacturing capabilities.
Conclusion
Stone aggregate powder conveying equipment plays a vital role in modern industrial operations, enabling the efficient and safe transport of bulk materials. The design principles behind these systems, including material handling efficiency, dust control, and energy efficiency, are crucial for optimizing performance and reducing operational costs. HeadPowder, with its expertise and commitment to quality, continues to be a leading provider of conveying solutions, helping businesses in the construction and industrial sectors achieve their operational goals. By understanding the design and functionality of these equipment, businesses can make informed decisions and select the most suitable solutions for their material handling needs.




