When it comes to the efficient handling and transportation of sorghum distillers grains powder, specialized equipment plays a crucial role in optimizing industrial processes. This article explores the concept of sorghum distillers grains powder conveying equipment and delves into the underlying design principles that ensure its effective operation.
Understanding Sorghum Distillers Grains Powder Conveying Equipment
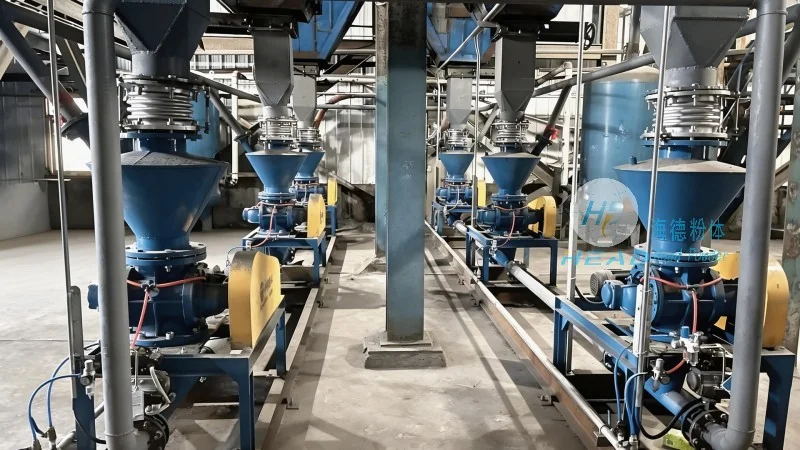
Sorghum distillers grains powder conveying equipment is a specialized system engineered to transport the fine powder derived from sorghum distillation processes. This material, often used as animal feed or in other industrial applications, requires careful handling due to its fine particle size and potential for dust generation. The equipment is designed to move this powder from one location to another within a facility or between different stages of production, ensuring a smooth and controlled flow.
Key Components and Functions of the Conveying System
The sorghum distillers grains powder conveying equipment typically consists of several key components that work in tandem to achieve efficient material transport. These components may include hoppers for material storage, conveyor belts or screw conveyors for horizontal and vertical movement, and dust control systems to manage airborne particles. Each component is carefully selected and integrated to address the unique challenges posed by the fine powder, such as caking, segregation, and dust explosion risks.
Design Principles for Optimal Performance
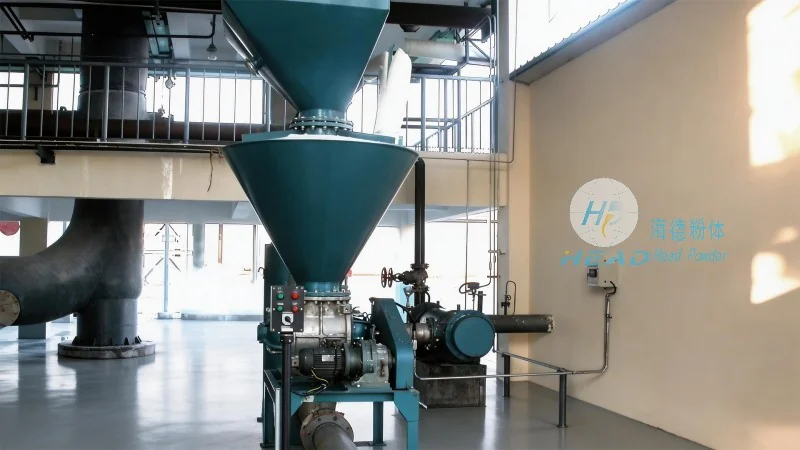
The design of sorghum distillers grains powder conveying equipment is guided by several fundamental principles aimed at maximizing efficiency, safety, and reliability. One of the primary principles is the minimization of material degradation during transport. This involves using materials that are resistant to abrasion and corrosion, as well as ensuring that the equipment operates at appropriate speeds to prevent particle breakage or agglomeration.
Another critical design principle is the prevention of dust accumulation and explosion hazards. This is achieved through the incorporation of effective dust collection systems, such as baghouses or cyclones, and the use of explosion-proof components throughout the system. Additionally, the design emphasizes the need for easy cleaning and maintenance to ensure consistent performance over time.
Material Handling Considerations
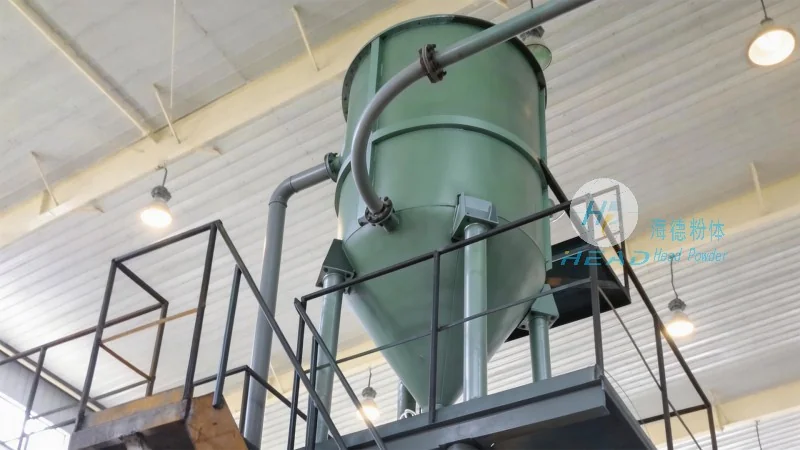
Handling sorghum distillers grains powder requires attention to several factors that influence the design and operation of the conveying equipment. The fine particle size of the powder means that it can easily flow and create blockages if not properly managed. Therefore, the equipment often includes features such as vibration systems or air-assisted conveying to prevent clogging and ensure a consistent flow rate.
Furthermore, the hygroscopic nature of the powder means that it can absorb moisture from the air, leading to clumping and reduced flowability. The design of the conveying system addresses this by incorporating drying or moisture control mechanisms, such as heated conveyor sections or desiccant systems, to maintain the powder's quality and prevent operational issues.
Applications and Benefits of the Equipment
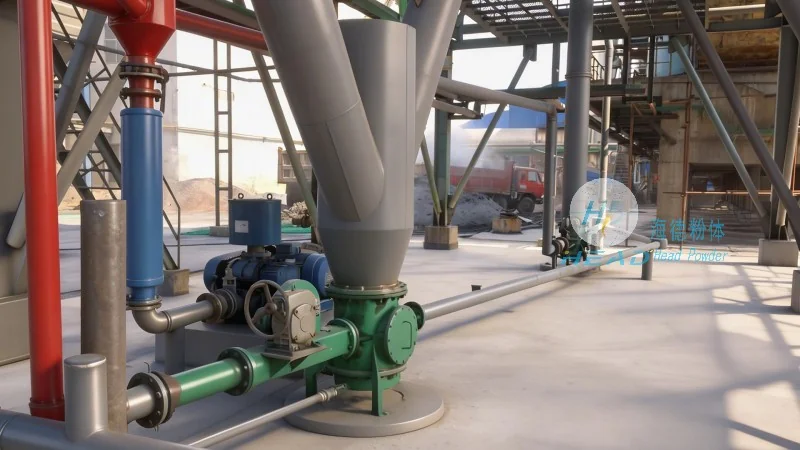
Sorghum distillers grains powder conveying equipment is widely used in the food and animal feed industries, as well as in other sectors where this byproduct is utilized. The benefits of using such equipment include improved process efficiency, reduced labor costs, and enhanced safety through the prevention of dust-related incidents. By ensuring that the powder is transported smoothly and safely, the equipment contributes to overall operational excellence and product quality.
Conclusion
In summary, sorghum distillers grains powder conveying equipment is a vital component in the industrial processing of sorghum distillers grains. Its design is based on principles that prioritize efficiency, safety, and material integrity, ensuring that the fine powder is handled effectively from production to end-use. The equipment, manufactured by companies like Shandong HeadPowder Engineering Co., Ltd. based in China, represents a sophisticated solution to the challenges of powder handling in modern industrial settings.




