For industries dealing with bulk powders, efficient and reliable material handling is crucial. A powder bin pneumatic conveying system is a specialized equipment designed to transport dry powders and granules from a storage bin to processing units or other locations within a facility. This article explores the fundamental aspects of such systems, focusing on their design principles and operational mechanisms.
Introduction to Powder Bin Pneumatic Conveying Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder handling equipment. The company's expertise lies in creating customized solutions that meet the unique demands of various industries, including pharmaceuticals, food processing, and chemical manufacturing. The powder bin pneumatic conveying system is a key product offered by HeadPowder, engineered to enhance productivity and ensure consistent material flow.
Core Components of a Powder Bin Pneumatic Conveying System
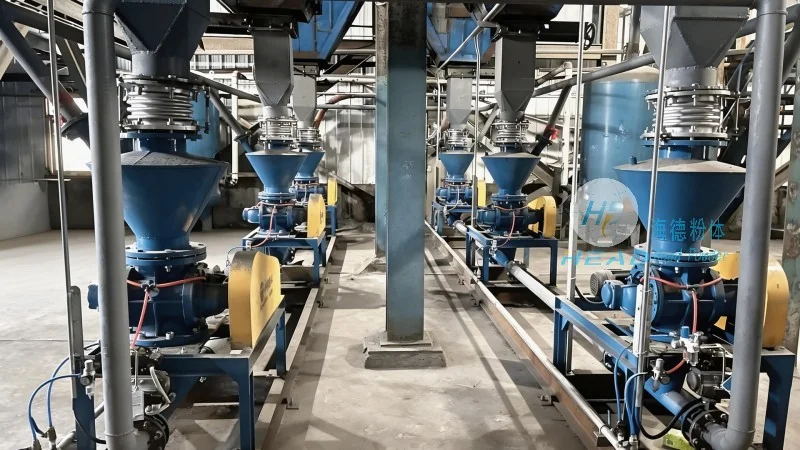
The system typically consists of several critical components that work in harmony to achieve effective powder transport. These include a storage bin, a conveying line, a blower or air compressor, a control system, and a receiver or discharge unit. The storage bin serves as the primary container for the bulk material, while the conveying line, often made of flexible or rigid tubing, facilitates the movement of the powder under pressure. The blower generates the necessary airflow to create a positive or negative pressure differential, enabling the powder to be conveyed through the system.
Design Principles Behind the System
The design of a powder bin pneumatic conveying system is guided by several key principles to ensure optimal performance and safety. One of the primary principles is the use of air as the conveying medium, which eliminates the need for mechanical components that could cause contamination or wear. The system operates on the principle of fluidization, where the powder particles are suspended in the air stream, allowing for smooth and continuous transport. Another critical principle is the maintenance of consistent air pressure and flow rates, which is achieved through advanced control systems that regulate the blower output and line pressure.
Operational Mechanisms and Flow Control
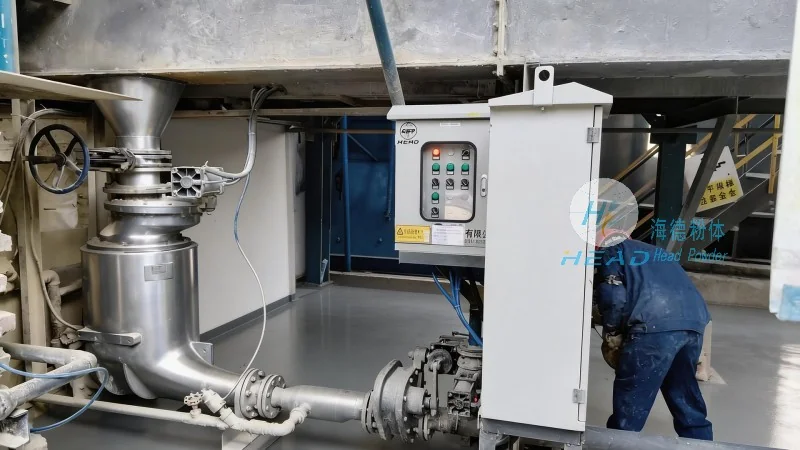
The operational mechanism of the system involves several steps. First, the powder is drawn from the storage bin into the conveying line by the air flow generated by the blower. The air pressure differential between the bin and the discharge point creates a suction effect, pulling the powder particles along the line. As the powder travels through the system, it may encounter various components such as bends, filters, or cyclones, which help in maintaining the flow and preventing blockages. The control system continuously monitors the pressure and flow rates, adjusting the blower speed or air volume as needed to maintain stable operation.
Advantages of Using a Powder Bin Pneumatic Conveying System
Implementing a powder bin pneumatic conveying system offers numerous advantages for industrial applications. One of the most significant benefits is the ability to transport powders over long distances without the need for intermediate storage or manual handling. This reduces labor costs and minimizes the risk of product contamination. Additionally, the system is highly flexible, allowing for easy integration with existing processing lines and the ability to adjust the conveying rate based on production demands. The use of air as the conveying medium also ensures that the powder remains dry and free from moisture, which is essential for many sensitive materials.
Applications in Different Industries
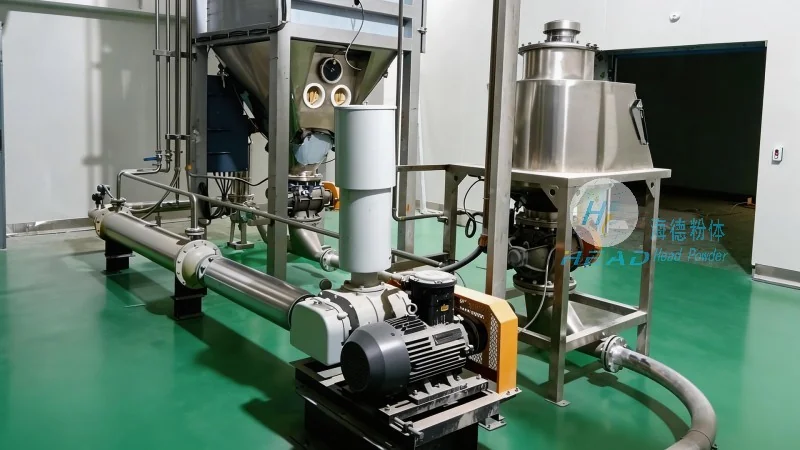
The versatility of powder bin pneumatic conveying systems makes them suitable for a wide range of industries. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal risk of cross-contamination. In the food processing sector, they are employed to handle powders like flour, sugar, and spices, ensuring hygienic and efficient transfer. The chemical industry also benefits from these systems when handling powders such as pigments, catalysts, and specialty chemicals, where maintaining product integrity is paramount.
Customization and Integration with HeadPowder Solutions
HeadPowder Engineering Co., Ltd., based in Shandong, China, provides customized powder bin pneumatic conveying systems tailored to the specific requirements of each client. The company's engineers work closely with customers to understand their operational needs, material characteristics, and facility layout, ensuring that the final system is optimized for performance and reliability. HeadPowder's solutions often include advanced features such as variable speed blowers, pressure sensors, and automated control interfaces, enhancing the system's adaptability and ease of use.
Conclusion
A powder bin pneumatic conveying system is a sophisticated piece of equipment that plays a vital role in modern industrial operations. By leveraging the principles of pneumatic transport and advanced engineering, these systems offer efficient, reliable, and hygienic solutions for handling bulk powders. HeadPowder, with its expertise and commitment to quality, continues to be a trusted provider of such systems, helping industries across the globe improve their material handling processes and overall productivity.




