For industrial operations dealing with sintered ash and other fine powders, efficient material handling is crucial. A sintered ash powder conveyor is a specialized piece of equipment designed to transport these materials with precision and reliability. This article explores the fundamental aspects of such conveyors, including their design principles and operational mechanisms.
Understanding the Core Function of Sintered Ash Powder Conveyors
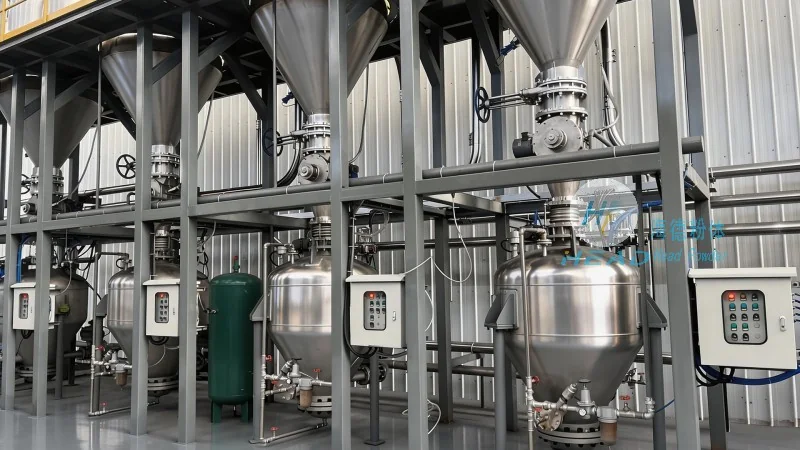
The primary function of a sintered ash powder conveyor is to move fine powders, such as sintered ash, from one location to another within a production facility. These conveyors are engineered to handle materials that are prone to dusting, caking, or bridging, ensuring consistent and controlled flow. The design focuses on minimizing material degradation and maintaining the integrity of the powder during transport.
Design Principles Behind Sintered Ash Powder Conveyors
The design principles of sintered ash powder conveyors are centered on addressing the unique challenges of handling fine powders. Key considerations include preventing material buildup, ensuring smooth material flow, and maintaining a clean, dust-free environment. The conveyor systems often incorporate features like variable speed drives, adjustable feed mechanisms, and specialized hopper designs to accommodate the properties of sintered ash and similar materials.
Key Components and Their Roles in Sintered Ash Powder Conveyors
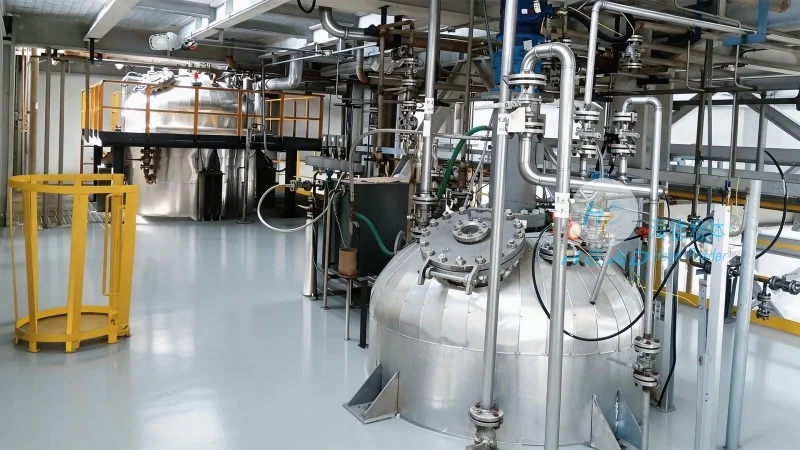
Several critical components contribute to the effective operation of a sintered ash powder conveyor. The hopper, typically made of corrosion-resistant materials like stainless steel, is designed to hold the sintered ash and prevent caking. The conveyor belt or screw mechanism, depending on the system type, ensures continuous movement of the material. Additionally, the system may include a dust collection system to maintain air quality and prevent environmental contamination. The control panel allows operators to adjust speed, feed rate, and other parameters to optimize performance.
Application Scenarios and Practical Uses of Sintered Ash Powder Conveyors
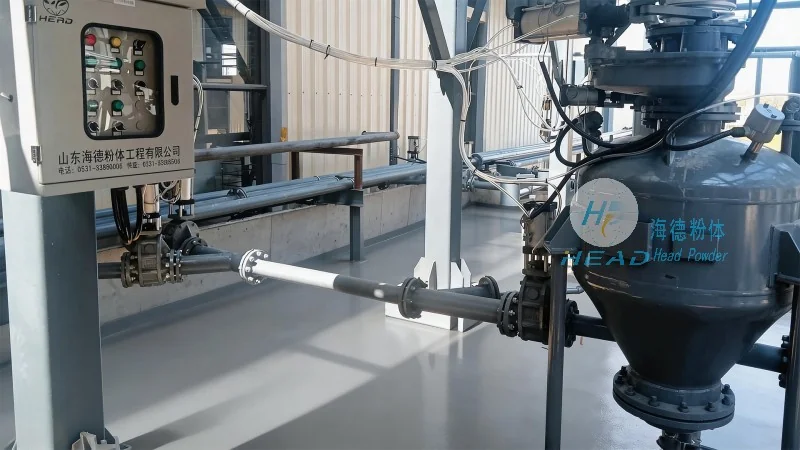
Sintered ash powder conveyors are widely used in various industrial applications, particularly in the cement, steel, and power generation sectors. They are essential for transporting sintered ash from storage silos to processing units or for moving it to disposal sites. The equipment is also used in recycling operations where sintered ash is repurposed as a raw material. In these applications, the conveyor's ability to handle fine powders efficiently and safely is critical to maintaining production efficiency and compliance with environmental regulations.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer specializing in the design and production of sintered ash powder conveyors and related material handling equipment. With a focus on quality and innovation, the company provides customized solutions tailored to the specific needs of industrial clients. HeadPowder's products are engineered to meet the highest standards of performance and durability, ensuring reliable operation in demanding industrial environments. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing techniques and expertise to deliver superior conveyor systems.




