Small-bag powder pneumatic conveying systems represent a sophisticated method for transporting bulk powders and granular materials over short to medium distances. This technology is particularly valuable in industries such as pharmaceuticals, food processing, and chemical manufacturing, where maintaining product purity and minimizing contamination is critical. The system operates by using compressed air to move material from a source to a destination, eliminating the need for mechanical components like conveyors or belts that could introduce contaminants or cause material degradation.
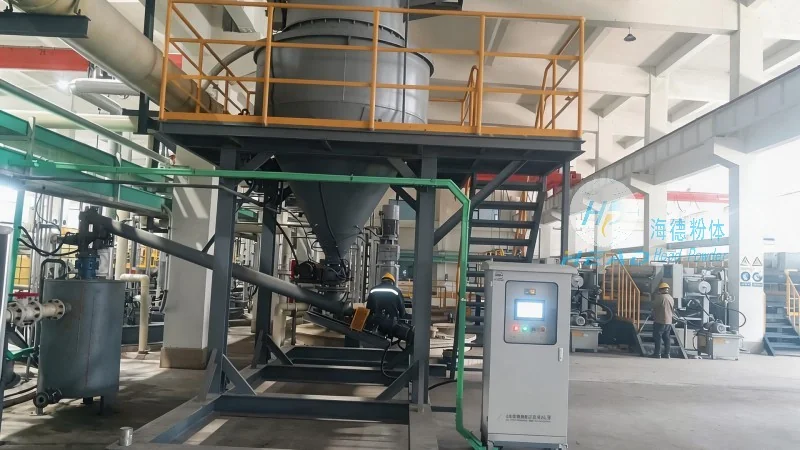
At the core of the small-bag powder pneumatic conveying system is the airlock or feeder, which controls the flow of material into the conveying line. The feeder typically consists of a hopper with a valve mechanism that allows precise control over the material discharge rate. This ensures a consistent and controlled flow of powder into the system, preventing overloading or underloading that could affect the conveying efficiency. The compressed air, often supplied by a dedicated air compressor, is introduced into the conveying line through a venturi or a series of pipes. The air flow creates a negative pressure or positive pressure environment, depending on the system design, which propels the powder particles forward. The velocity of the air and the size of the particles determine the optimal conveying conditions, with larger particles requiring higher air velocities to maintain suspension.
The system's design incorporates features that enhance efficiency and reliability. For instance, the use of flexible hoses or rigid pipes allows for easy installation in confined spaces or around obstacles, making it adaptable to various plant layouts. The air filtration system is another critical component, as it removes dust and particulates from the air before it is released into the environment, ensuring compliance with environmental regulations and maintaining air quality in the workplace. Additionally, the system may include a cyclone separator or a bag filter at the receiving end to separate the material from the air stream, allowing for clean material collection and air recirculation or discharge.
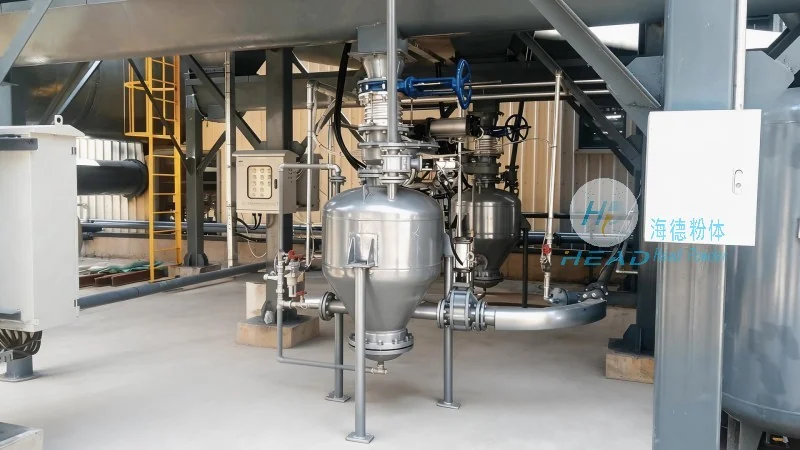
One of the key advantages of small-bag powder pneumatic conveying systems is their ability to handle a wide range of materials, from fine powders to coarse granules. This versatility makes them suitable for diverse applications, including the transport of pharmaceutical powders, food additives, and chemical reagents. The system's design minimizes product degradation by reducing friction and exposure to air, which is particularly important for heat-sensitive or moisture-sensitive materials. Furthermore, the enclosed nature of the system prevents cross-contamination between different product batches, a feature that is essential in industries where product purity is non-negotiable.
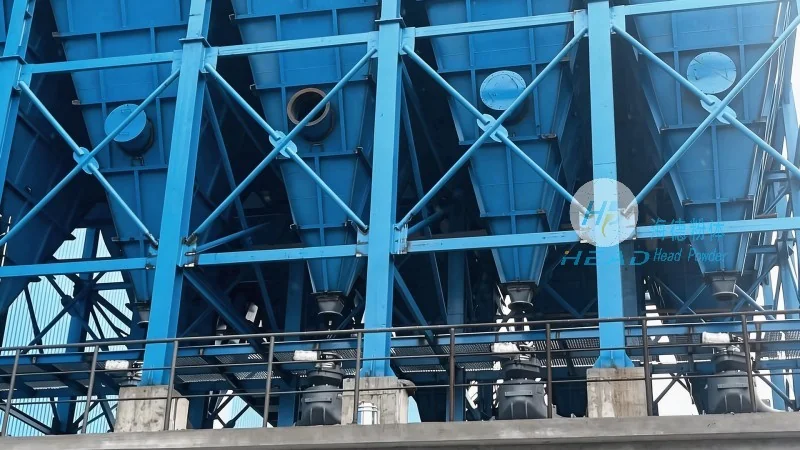
Another significant feature is the system's energy efficiency. By optimizing the air flow and particle size, the system can achieve high conveying rates with relatively low energy consumption compared to other methods like belt conveyors or screw conveyors. This not only reduces operational costs but also contributes to a more sustainable operation. The system's maintenance requirements are also relatively low, as the components are designed for durability and ease of replacement, minimizing downtime and maintenance expenses.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, specializes in the design, manufacturing, and installation of small-bag powder pneumatic conveying systems. With a strong commitment to quality and innovation, the company has developed systems that meet the stringent requirements of various industries. HeadPowder's systems are engineered to provide reliable performance, high efficiency, and low maintenance, ensuring that clients can achieve their production goals while maintaining product quality and safety standards. The company's facilities are located in Shandong, China, where it leverages advanced technology and skilled expertise to deliver superior products and services to its global clientele.




