For industrial applications involving the handling of copper sulfate, pneumatic conveying systems offer an efficient and reliable method of material transport. This article explores the working principles and key characteristics of such systems, providing insights into their operational efficiency and suitability for copper sulfate handling.
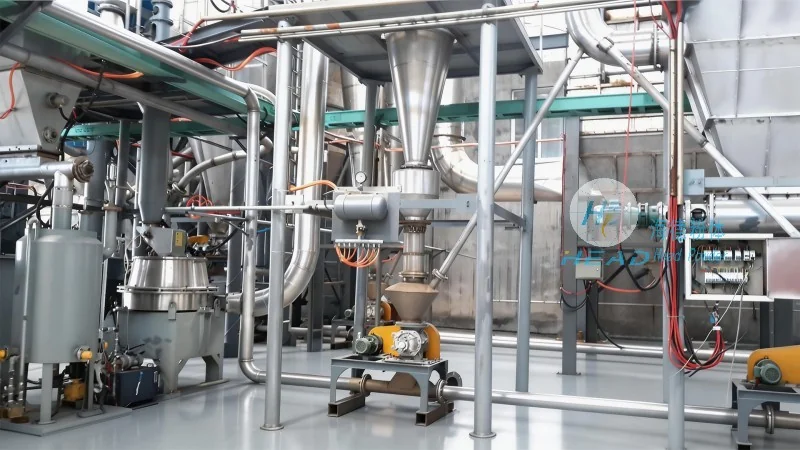
Understanding Pneumatic Conveying for Copper Sulfate
Pneumatic conveying, also known as pneumatic transport, is a technology that uses pressurized air or vacuum to move bulk materials through a pipeline. In the context of copper sulfate, which is often used in chemical processing, agriculture, and water treatment, this method provides a non-contact, hygienic, and efficient way to transport the material from storage to processing equipment or for distribution.
Working Principle of Copper Sulfate Pneumatic Conveying
The core working principle of a copper sulfate pneumatic conveying system involves the use of a fan or blower to generate airflow within a sealed pipeline. The system typically operates in either of two modes: vacuum (or suction) conveying or pressure (or pressure) conveying. In vacuum conveying, a vacuum is created at the receiving end to draw the copper sulfate particles into the pipeline, while the air and material mixture is then transported to the discharge point. Pressure conveying, on the other hand, involves forcing air and material through the pipeline from a pressurized source, often using a positive displacement blower.
During the conveying process, the copper sulfate particles are suspended in the air stream, allowing them to be transported over long distances without the need for mechanical components like conveyors or elevators. The system includes key components such as a hopper for material storage, a feeder to control the flow rate, a conveying line, and a separator or filter to separate the material from the air at the discharge end. The air is then typically filtered and recycled back into the system to maintain efficiency and reduce environmental impact.
Key Characteristics and Advantages of Copper Sulfate Pneumatic Conveying
Several distinct characteristics make pneumatic conveying an attractive option for copper sulfate handling. First, it is a hygienic and dust-free process, which is crucial when dealing with materials used in food, pharmaceutical, or water treatment applications. The enclosed system prevents contamination and exposure to airborne particles, ensuring compliance with health and safety regulations.
Second, pneumatic conveying offers high efficiency and flexibility. It can handle a wide range of particle sizes and moisture contents, making it suitable for various forms of copper sulfate, including powders, granules, or even wet slurries. The system can be easily adjusted to transport materials over different distances, from short distances within a facility to long-distance transfers between sites.
Third, the process is environmentally friendly. By using a closed system, it minimizes dust emissions and reduces the risk of material spillage or contamination of the surrounding environment. The air used in the system is often filtered and recycled, reducing energy consumption and waste generation compared to traditional mechanical conveying methods.
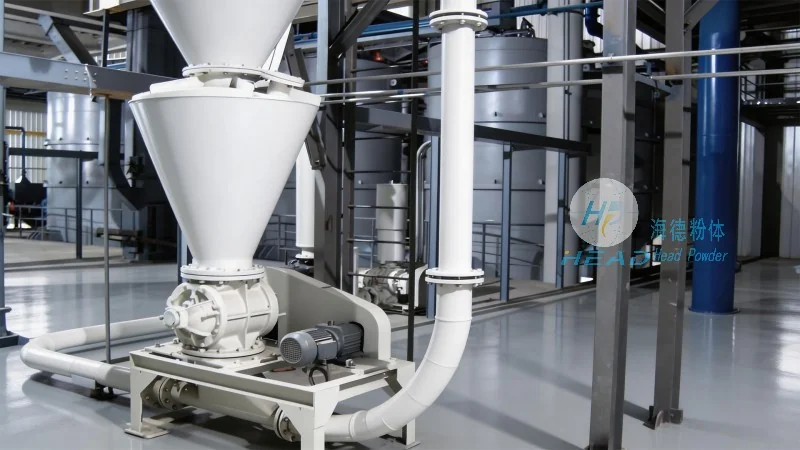
Fourth, the system provides high reliability and low maintenance. With fewer moving parts compared to belt or screw conveyors, pneumatic conveying systems experience less wear and tear, leading to lower maintenance costs and longer operational life. This reliability is particularly important for continuous industrial processes where downtime can be costly.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
As a specialized provider in the field of bulk material handling, Shandong HeadPowder Engineering Co., Ltd. offers comprehensive solutions for copper sulfate and other chemical materials. With a focus on engineering excellence and customer satisfaction, the company designs, manufactures, and installs customized pneumatic conveying systems tailored to the specific needs of its clients. HeadPowder's expertise in material flow technology ensures that the systems are optimized for efficiency, safety, and environmental compliance, meeting the stringent requirements of modern industrial applications.
HeadPowder is committed to delivering high-quality, reliable equipment and services, backed by a team of experienced engineers and technicians. The company's facilities are located in Shandong, China, where it leverages advanced manufacturing capabilities and stringent quality control processes to ensure that every system meets the highest standards. By choosing HeadPowder, industrial clients can benefit from innovative solutions that enhance operational performance and reduce long-term costs in their copper sulfate handling processes.




