Understanding the fundamentals of dust pneumatic conveying is crucial for industries that handle fine powders and granular materials. This technology, which relies on the movement of material through a pipeline using air or gas, offers a versatile solution for material transport. The core principle involves creating a pressure differential that propels the material forward, making it an efficient alternative to traditional mechanical conveying systems.
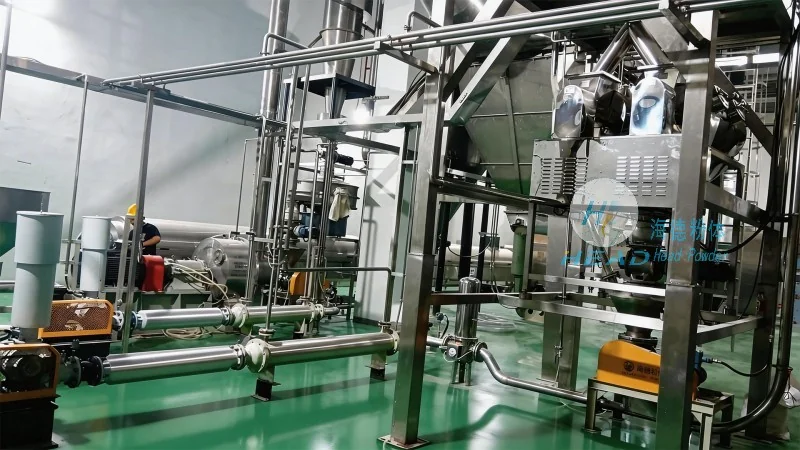
Principles of Dust Pneumatic Conveying
The operation of dust pneumatic conveying systems is based on the physics of fluid dynamics and particle movement. In a typical system, a fan or blower generates airflow that draws or pushes the material through a pipeline. The system can be categorized into two main types: dilute-phase and dense-phase. Dilute-phase systems use low air velocity and high material concentration, suitable for short distances and low material density. Dense-phase systems, on the other hand, use higher air velocity and lower material concentration, ideal for longer distances and higher material density, ensuring minimal product degradation and reduced pressure drop.
Working Scene Characteristics
The application of dust pneumatic conveying varies across different industrial sectors, each with unique requirements and challenges. In the pharmaceutical industry, for example, the system must maintain high levels of cleanliness and prevent cross-contamination, making it essential to use stainless steel components and sealed systems. In the food processing sector, the equipment is designed to handle hygienic materials, with features like easy cleaning and compliance with food safety regulations. The chemical industry requires systems that can handle corrosive or abrasive materials, often incorporating specialized materials of construction such as PTFE or high-grade stainless steel to ensure durability and safety.
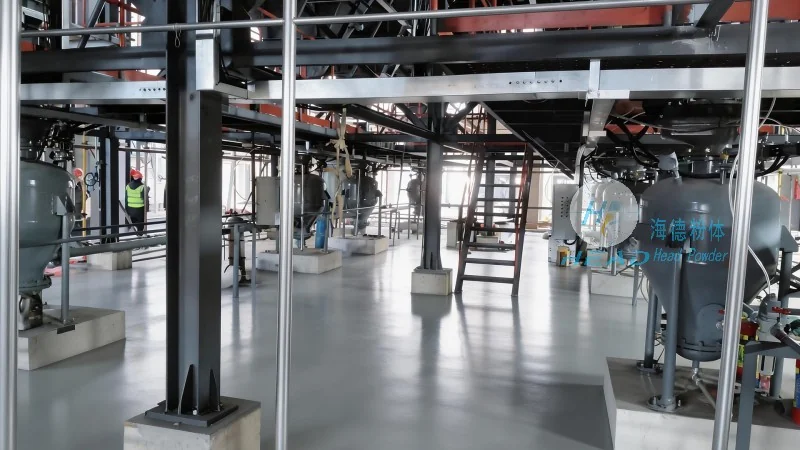
HeadPowder Engineering: Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying systems, specializes in designing and manufacturing customized solutions tailored to the specific needs of various industries. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable material handling solutions. HeadPowder's team of engineers and technicians brings extensive experience in the field, ensuring that each system is optimized for efficiency, safety, and longevity.
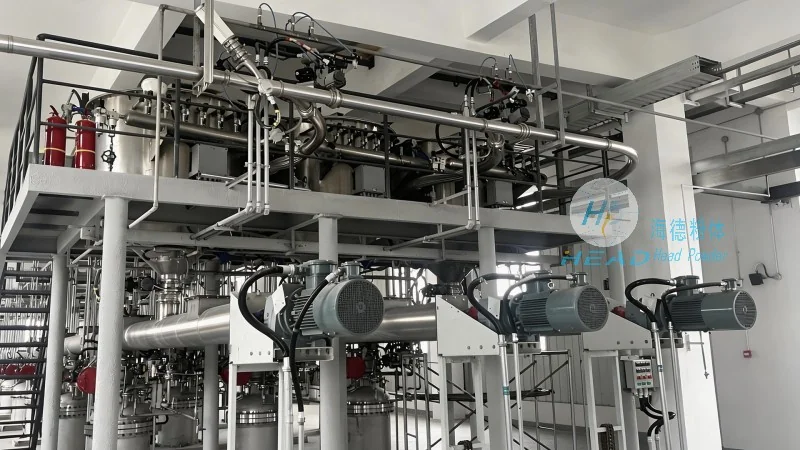
Customization and System Integration
One of the key advantages of working with HeadPowder is the ability to customize pneumatic conveying systems to meet specific operational requirements. The company offers a range of options, including positive pressure, negative pressure, and hybrid systems, allowing clients to choose the most suitable configuration for their application. Additionally, HeadPowder provides comprehensive system integration services, ensuring that the conveying system is seamlessly integrated with existing production lines and equipment. This approach minimizes downtime and maximizes operational efficiency, providing a cost-effective solution for material transport needs.
Quality Assurance and After-Sales Support
HeadPowder Engineering adheres to strict quality control standards to ensure that all products meet the highest industry benchmarks. From raw material selection to final assembly, each step of the manufacturing process is closely monitored to guarantee reliability and performance. The company also provides comprehensive after-sales support, including maintenance services, technical assistance, and system upgrades. This commitment to customer satisfaction ensures that clients receive long-term value and support throughout the lifecycle of their pneumatic conveying systems.




