Chocolate pneumatic conveying equipment is a specialized system designed to transport chocolate products efficiently and hygienically within industrial settings. This equipment, developed by Shandong HeadPowder Engineering Co., Ltd., plays a crucial role in the chocolate manufacturing process, ensuring that raw materials and finished products are moved with precision and care. The technology behind these systems combines the principles of fluidization and air movement to create a gentle yet effective method of material handling, which is particularly important for delicate chocolate products that require minimal agitation and temperature control.
Understanding the Core Principles of Chocolate Pneumatic Conveying
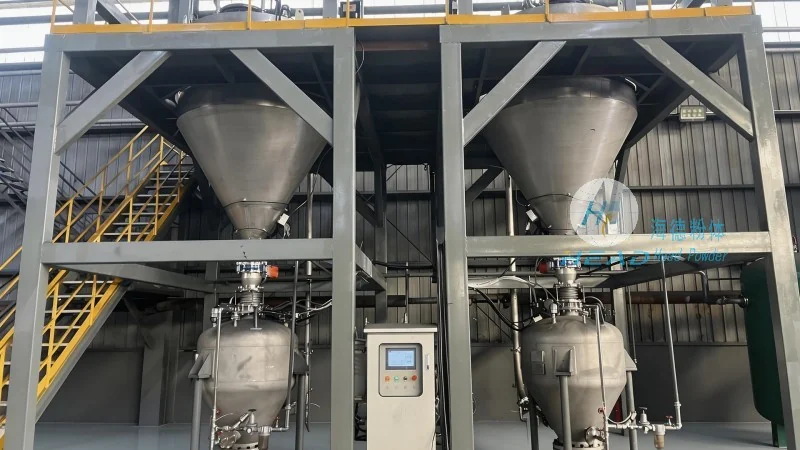
The fundamental principle of chocolate pneumatic conveying involves using compressed air to create a flow of material through a pipeline. The system typically consists of a hopper, a conveyor line, and a receiver. As chocolate is introduced into the hopper, it is drawn into the conveyor line by the air flow, which lifts and transports the material to the desired location. This process is often referred to as "air lift" or "pneumatic transport," and it relies on the balance between the air pressure and the weight of the chocolate particles. The key to successful operation lies in maintaining consistent air pressure and flow rates, which ensures that the chocolate moves smoothly without clogging or degradation.
Key Components and Their Functions in Chocolate Pneumatic Conveying Systems
Several critical components work together to ensure the efficient operation of chocolate pneumatic conveying equipment. The hopper serves as the storage and feeding unit, where chocolate is loaded before being introduced into the conveyor line. The conveyor line itself is a network of pipes that transport the chocolate using air pressure. The air supply system, which includes compressors and filters, provides the necessary air pressure to move the material. Additionally, the receiver or discharge unit collects the chocolate at the end of the conveyor line, ensuring a clean and controlled discharge. Each component must be designed to handle the specific characteristics of chocolate, such as its density, moisture content, and temperature sensitivity, to prevent product damage and system inefficiencies.
Working Scene Characteristics and Applications
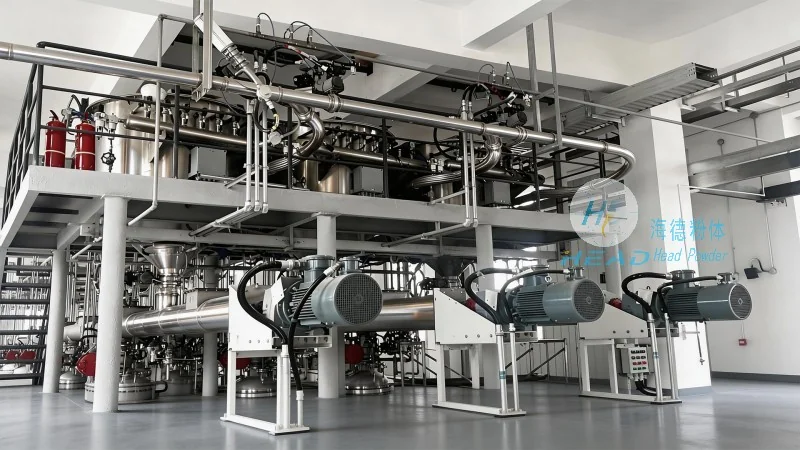
Chocolate pneumatic conveying equipment is widely used in various industrial settings, including chocolate factories, confectionery plants, and food processing facilities. The working scene characteristics of these systems are tailored to the specific needs of each application. For example, in a large-scale chocolate production facility, the equipment may be used to transport raw cocoa beans from storage to processing lines, or to move finished chocolate products from production areas to packaging stations. The systems are also commonly used in smaller-scale operations, such as artisanal chocolate shops, where the equipment helps maintain a consistent workflow and product quality. The versatility of chocolate pneumatic conveying makes it suitable for a range of applications, from bulk material handling to precise product transfer.
Advantages of Using Chocolate Pneumatic Conveying Equipment
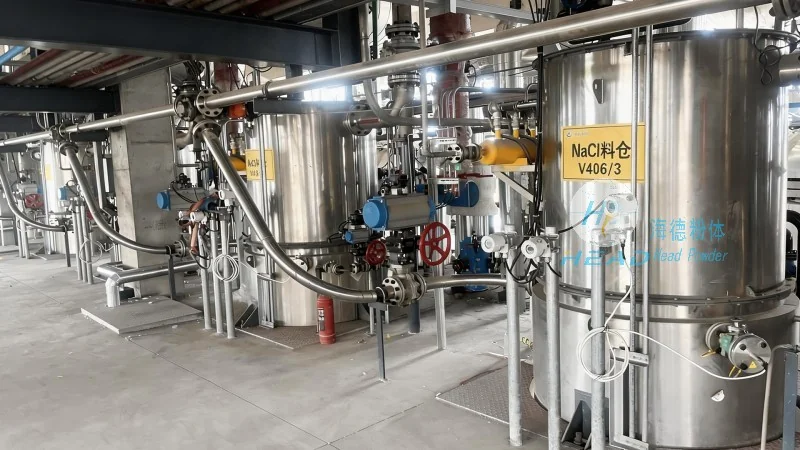
There are several advantages to implementing chocolate pneumatic conveying systems in industrial settings. One of the primary benefits is the gentle handling of chocolate products, which minimizes the risk of product damage or degradation. Unlike traditional mechanical conveyors, which can cause friction and temperature changes that affect the quality of chocolate, pneumatic systems use air to move the material, ensuring that the product remains intact and fresh. Another advantage is the hygienic design of these systems, a hallmark of products from Shandong HeadPowder Engineering Co., Ltd., which is essential for food processing environments. The enclosed pipelines and sealed components prevent contamination from external sources, maintaining the safety and quality of the chocolate products. Additionally, pneumatic conveying systems are highly efficient, as they can transport large volumes of material over long distances with minimal energy consumption. This efficiency makes them a cost-effective solution for chocolate manufacturers looking to optimize their production processes.
Considerations for Selecting and Implementing Chocolate Pneumatic Conveying Systems
When selecting and implementing chocolate pneumatic conveying equipment, several factors must be considered to ensure optimal performance and compatibility with the specific application. The first consideration is the type of chocolate being handled, as different varieties may have varying characteristics that affect system design. For example, dark chocolate may require different air pressure settings than milk chocolate due to differences in density and moisture content. Another important factor is the scale of the operation, as larger facilities may require more robust systems with higher air flow rates and larger conveyor lines. The location of the facility and the distance between the feeding and discharge points also play a role in determining the appropriate system configuration. Additionally, the hygienic standards of the food processing environment must be taken into account, as the equipment must meet strict regulations for cleanliness and safety. By carefully evaluating these factors, manufacturers can select a chocolate pneumatic conveying system that meets their specific needs and ensures efficient, safe, and high-quality chocolate production.




