HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of efficient powder conveying systems. This article explores the fundamental principles behind the conveying of powdered edible salt and highlights key application scenarios where such systems are utilized.
Understanding the Fundamentals of Powdered Edible Salt Conveying
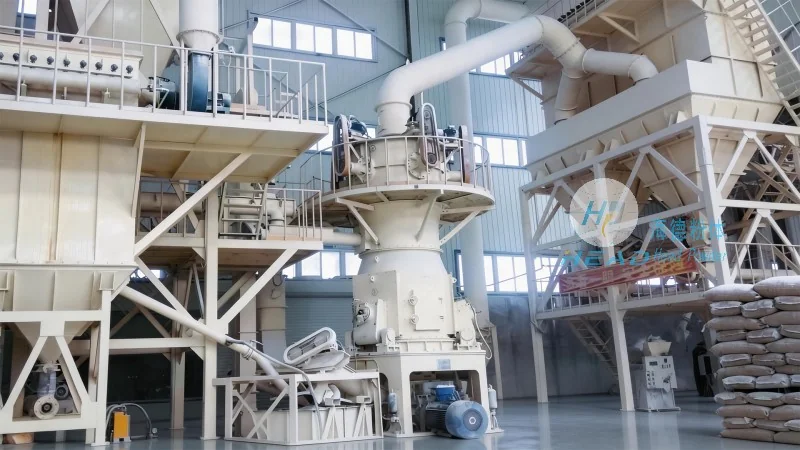
The process of conveying powdered edible salt involves the movement of fine granular material from one location to another, typically within industrial or processing environments. The core principle revolves around the use of mechanical or pneumatic systems to transport the salt while maintaining its integrity and preventing issues like caking or segregation. Key factors influencing the effectiveness of the conveying system include particle size, moisture content, and the overall flow characteristics of the salt. Engineers at Shandong HeadPowder Engineering Co., Ltd. consider these variables meticulously to design systems that ensure reliable and consistent transport. The company’s expertise lies in selecting appropriate equipment such as screw conveyors, pneumatic conveyors, or bucket elevators, each tailored to the specific properties of edible salt and the operational requirements of the facility.
Key Working Scenarios for Powdered Edible Salt Conveying Systems
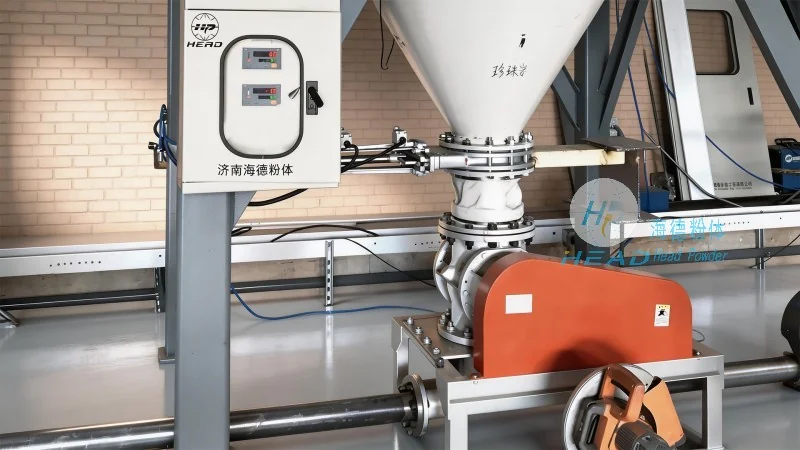
Industrial food processing plants often rely on sophisticated conveying systems to manage large volumes of edible salt efficiently. These systems are crucial in scenarios where salt needs to be transported from storage silos to processing lines, or from production areas to packaging units. For instance, in a large-scale salt production facility, a pneumatic conveyor might be employed to move salt from a storage hopper to a milling machine, ensuring a continuous flow without interruptions. Another common scenario involves the integration of conveying systems with automated packaging lines, where the salt is transferred from a bulk container to individual packaging machines with precision. The design of these systems must account for hygiene standards, as edible salt is a food product, requiring materials that are non-corrosive and easy to clean. Shandong HeadPowder Engineering Co., Ltd. has extensive experience in implementing such systems in food processing industries, ensuring compliance with food safety regulations while optimizing operational efficiency.
Technical Considerations and System Optimization
Effective powdered edible salt conveying requires careful consideration of several technical aspects. One critical factor is the prevention of material buildup or blockages in the conveying lines, which can occur due to the fine particle size and potential for agglomeration. HeadPowder engineers employ anti-caking additives or moisture control measures to mitigate these issues, ensuring smooth operation. Additionally, the system must be designed to handle variations in salt flow rates, which can fluctuate based on production schedules or demand. The use of variable speed drives and adjustable valves allows for flexible control over the conveying process. In terms of energy efficiency, modern systems incorporate energy-saving technologies such as regenerative blowers or optimized screw designs, reducing operational costs for the client. The company’s approach to system optimization also includes regular maintenance and performance monitoring to identify and address any potential issues proactively, thereby extending the lifespan of the equipment and minimizing downtime.
Case Studies and Real-World Applications
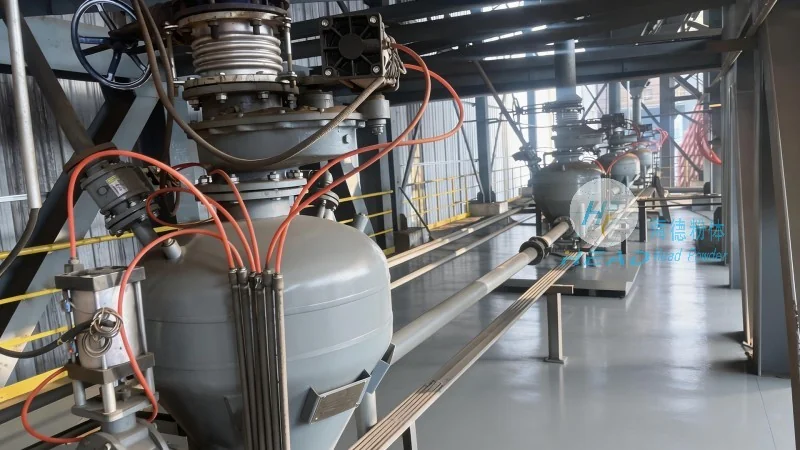
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented numerous powdered edible salt conveying systems across various industries. For example, a major food processing company in China relied on a custom-designed screw conveyor system to transport salt from a storage silo to their production line. The system was engineered to handle high volumes of salt while maintaining consistent flow rates, resulting in improved production throughput. Another case involved a salt packaging facility where a pneumatic conveying system was integrated with automated packaging machines to ensure precise dosing of salt into individual packets. The system’s reliability and accuracy helped the client achieve higher packaging speeds and reduce material waste. These real-world applications demonstrate the practical effectiveness of the conveying principles and the expertise of HeadPowder in delivering tailored solutions for specific industrial needs.




