Principles and Working Scene Characteristics of Feather Material Conveying
Release time:2026-09-19 08:01:31
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Feather material conveying systems are critical in industries where the handling of lightweight, delicate, or irregularly shaped materials is required. The fundamental principle behind these systems involves the use of specialized equipment designed to efficiently transport feathers while minimizing damage and ensuring consistent flow. This article explores the core principles of feather material conveying and highlights key working scene characteristics that define their application in various industrial settings.
Understanding the Core Principles of Feather Material Conveying
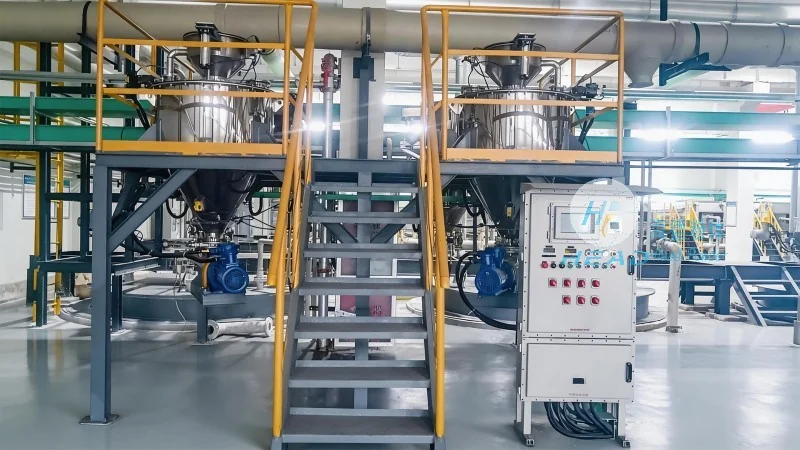
The primary principle of feather material conveying revolves around gentle yet effective movement of lightweight materials. Unlike traditional bulk material handling systems that rely on gravity or high-velocity air streams, feather conveying systems utilize low-pressure air or mechanical means to transport feathers without causing breakage or contamination. The design typically incorporates components such as airlocks, flexible hoses, and specialized conveying tubes that allow for smooth, continuous movement of the material. The key is to maintain a controlled airflow or mechanical force sufficient to move the feathers but gentle enough to preserve their integrity. This approach ensures feathers are transported from one location to another without being crushed, torn, or mixed with other materials, which is crucial in applications where the quality and purity of the feathers are paramount.
Key Working Scene Characteristics of Feather Material Conveying
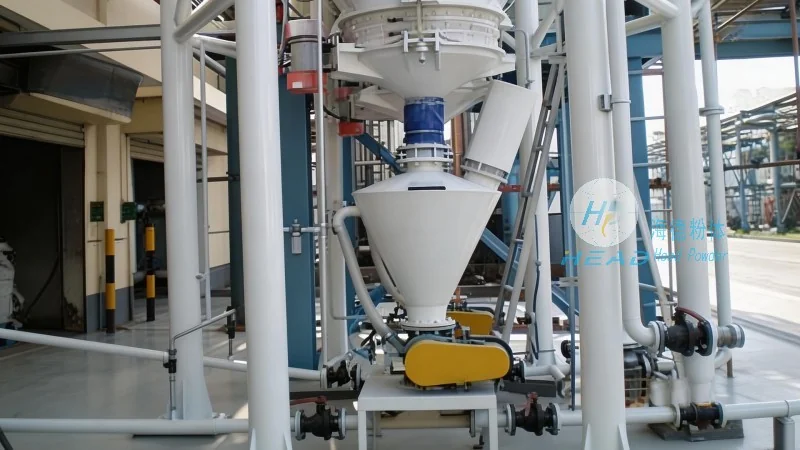
Feather material conveying systems are commonly employed in several distinct working scenes, each with unique requirements and operational characteristics. One primary application is in processing raw feathers from poultry farms to processing facilities. In this scenario, the system must handle large volumes of feathers that may be wet or contaminated, requiring robust yet gentle conveying methods. The working scene often involves large-scale, continuous operations where material transport efficiency directly impacts production throughput. Another common working scene is within the manufacturing of feather products, such as pillows, duvets, or decorative items. Here, the conveying system must deliver feathers to processing lines where they are sorted, cleaned, or blended with other materials. The working scene in this case emphasizes precision and cleanliness, as any impurities or damage to the feathers can affect final product quality. Additionally, feather material conveying is used in recycling and repurposing feathers from waste streams, where the system must handle feathers mixed with other organic materials. This working scene requires adaptability and the ability to separate feathers from other waste components efficiently.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
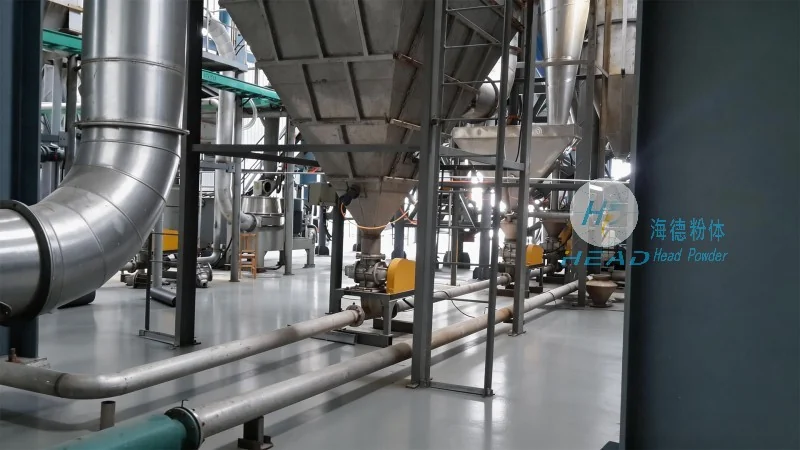
HeadPowder, a leading provider of material handling solutions, specializes in the design and manufacturing of feather material conveying systems. With a strong focus on innovation and customer-centric solutions, the company has established itself as a trusted partner in the industry. HeadPowder's products are engineered to meet specific application needs, ensuring reliability and efficiency in feather material transport. The company's headquarters is located in Shandong, China, where it leverages advanced technology and manufacturing capabilities to deliver high-quality equipment. By combining expertise in material science and mechanical engineering, HeadPowder offers tailored solutions that enhance operational performance and reduce downtime for clients. The company's commitment to quality and customer satisfaction has made it a preferred choice for businesses operating in feather processing and related industries.




