For industrial operations involving catalyst powders, efficient and reliable material handling is crucial. Catalyst powder handling equipment is designed to manage the transport, storage, and processing of these fine powders with precision. This article explores the underlying principles of such equipment and highlights key working scene characteristics that define their performance and application.
Principle of Catalyst Powder Material Handling Equipment
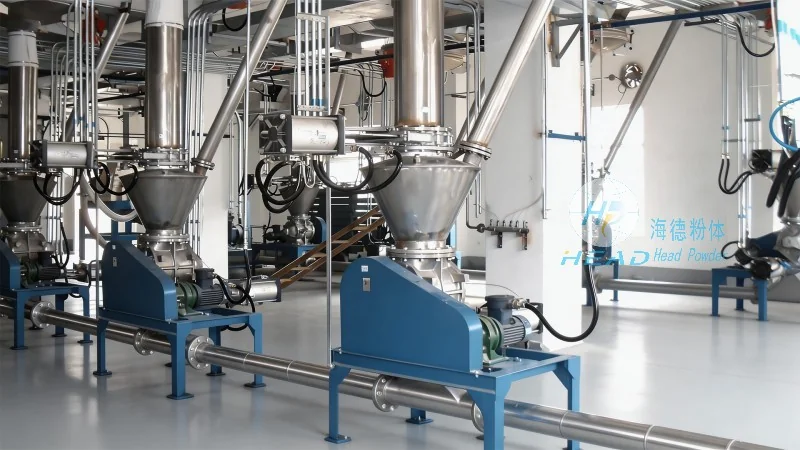
The core principle of catalyst powder handling equipment revolves around the controlled movement of fine powders from one location to another. These systems typically employ mechanisms like pneumatic conveying, screw conveyors, or vacuum systems to ensure the safe and efficient transfer of catalyst powders. Pneumatic conveying, for instance, uses compressed air to move powders through pipelines, while screw conveyors utilize rotating screws to push material along a trough. The choice of mechanism depends on factors such as the particle size, moisture content, and the required distance of transport. Advanced systems may also incorporate features like dust collection and filtration to maintain air quality and prevent contamination. The design of these equipment ensures minimal product degradation, preventing agglomeration or loss of active ingredients, which is critical for maintaining catalyst performance.
Working Scene Characteristics of Catalyst Powder Handling Equipment
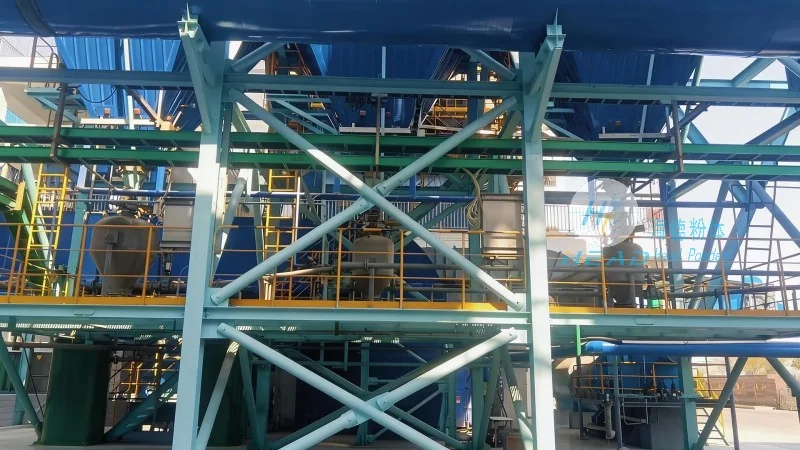
The working scene characteristics of catalyst powder handling equipment are tailored to meet the diverse demands of industrial applications. These characteristics include high precision in dosage control, which is essential for maintaining consistent catalyst activity in processes like chemical synthesis or refining. Additionally, the equipment is engineered for low maintenance and durability, as continuous operation in demanding environments requires robust construction. The working scenes often involve integration with other processing units, such as reactors or mixers, necessitating seamless coordination and compatibility. In pharmaceutical and fine chemical industries, the equipment must adhere to stringent hygiene standards, featuring easy-to-clean surfaces and enclosed systems to prevent cross-contamination. For large-scale industrial plants, the equipment is designed for scalability, allowing for expansion as production needs grow. The working scenes also emphasize safety, with features like explosion-proof designs and emergency shut-off mechanisms to mitigate risks associated with handling flammable or reactive powders.
Company Information and Application Support
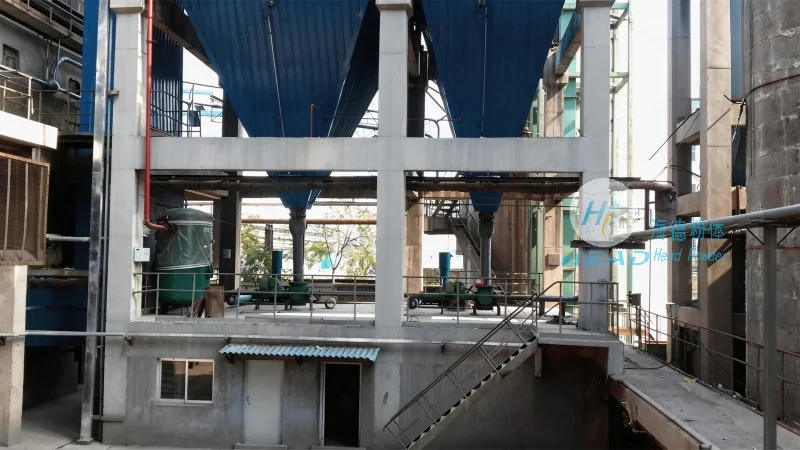
HeadPowder, a leading provider of engineering solutions, specializes in the design and manufacturing of catalyst powder handling equipment. With a focus on innovation and customer-centric solutions, HeadPowder delivers systems that meet the unique requirements of various industrial sectors. The company is headquartered in Shandong, China, and serves clients globally with tailored equipment that enhances operational efficiency and product quality. HeadPowder's expertise lies in understanding the specific challenges of catalyst handling, such as particle size distribution and material flow, and developing solutions that address these challenges effectively. By combining advanced technology with practical application knowledge, HeadPowder ensures that its equipment not only meets but exceeds industry standards, providing reliable performance in demanding working environments.




