Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier of industrial powder handling solutions, headquartered in Shandong, China. The company specializes in the design, development, and implementation of advanced pneumatic conveying systems tailored for various industrial applications. With a focus on innovation and customer satisfaction, HeadPowder provides customized solutions that meet the unique needs of each client.
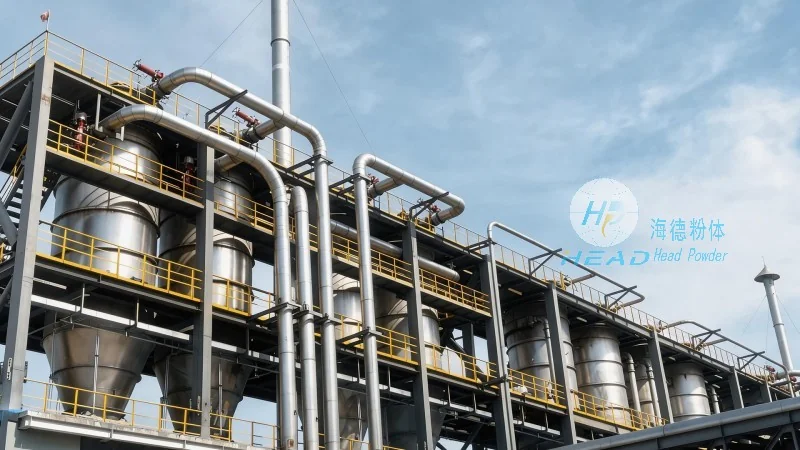
System Principle and Operational Mechanism
The bottom-hopper powder pneumatic conveying system operates on the principle of air-based transport, where powder materials are drawn from a hopper at the bottom of a storage silo or bin. The system uses a combination of pressure or vacuum to create a flow of air that carries the powder particles through a pipeline network. Key components include the hopper, air compressor, filter, and control valves, which work in tandem to ensure efficient and reliable material transfer. The air compressor generates the necessary pressure or vacuum, while the filter removes any particulate matter from the air stream, preventing contamination of the conveyed material.
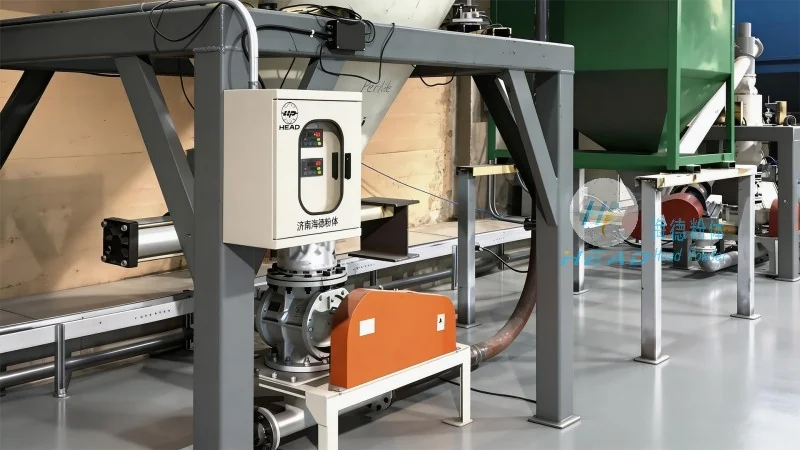
Work Scene Characteristics and Application Scenarios
These systems are particularly suited for applications where bulk powder handling is required in confined spaces or where traditional mechanical conveyors may be impractical. Common operational scenarios include pharmaceutical manufacturing, food processing, chemical production, and mining operations. The bottom-hopper design allows for continuous material feeding, reducing downtime and improving overall production efficiency. Additionally, the system's ability to handle fine powders without clogging or degradation makes it ideal for sensitive materials such as pharmaceuticals, food ingredients, and specialty chemicals.
Advantages of the Bottom-Hopper Configuration
The bottom-hopper configuration offers several advantages over other pneumatic conveying methods. It provides a self-contained feeding mechanism that eliminates the need for external feeders, simplifying installation and maintenance. The system's compact design fits well in existing facilities, minimizing space requirements. Furthermore, the use of air as the conveying medium reduces wear and tear on equipment, extending the lifespan of components and lowering long-term operational costs. The system also ensures consistent material flow rates, which is crucial for maintaining quality control in production processes.
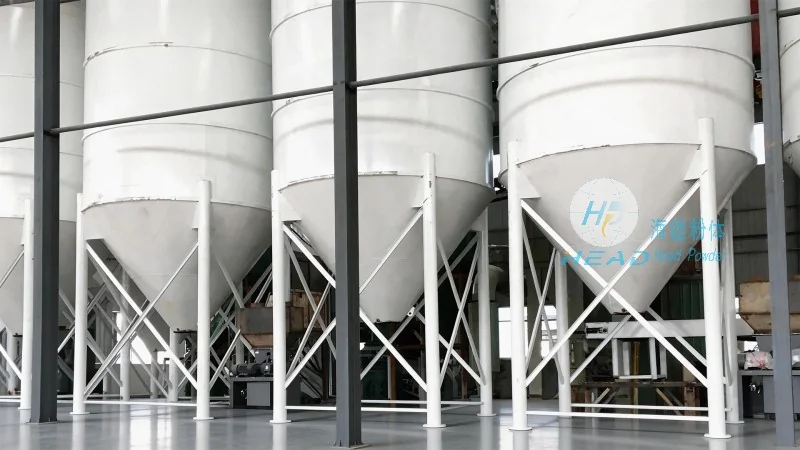
Application Examples in Industrial Settings
In pharmaceutical plants, the system ensures that raw materials are transferred in a sterile and controlled environment, maintaining product purity. In food processing facilities, the bottom-hopper system handles ingredients like flour and sugar, ensuring consistent quality and preventing contamination. Chemical manufacturers benefit from the system's ability to handle corrosive or abrasive powders, protecting equipment and ensuring safety compliance. Mining operations use these systems to transport ore and other minerals from storage bins to processing equipment, improving operational efficiency and reducing labor costs.




