Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and application of dust-free closed material pneumatic conveying equipment. This article explores the fundamental principles behind such systems and highlights the key characteristics of their operational scenarios, providing a comprehensive overview for professionals in various industries.
Understanding the Core Principles of Dust-Free Pneumatic Conveying Systems
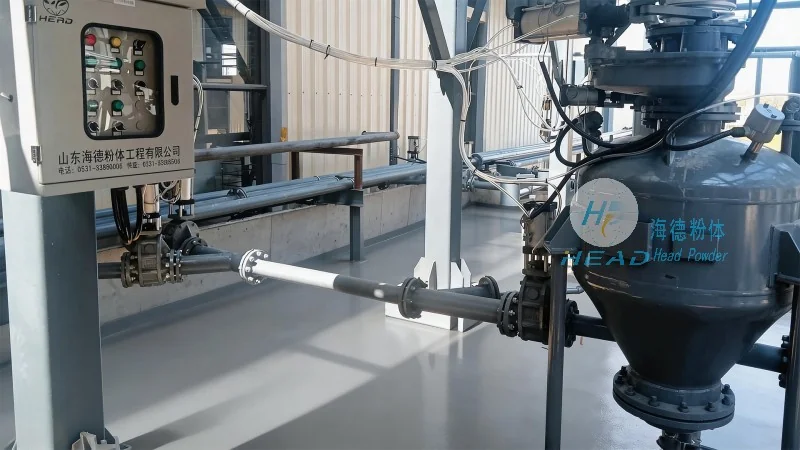
The principle of dust-free closed material pneumatic conveying involves transporting bulk materials through a sealed pipeline system using compressed air or other gas as the conveying medium. Unlike traditional open-air methods, this technology maintains a completely enclosed environment, preventing dust emissions and ensuring compliance with stringent environmental and safety regulations. The system typically operates under either positive pressure (where air is forced into the pipeline) or negative pressure (where air is drawn out), depending on the specific material properties and application requirements. The key components of a typical system include a material feeder, a conveying pipeline, a control unit, and a dust collection or separation unit. The material feeder ensures a consistent flow of material into the pipeline, while the control unit regulates the air pressure and flow rate to maintain optimal conveying efficiency. The sealed pipeline prevents any material from escaping and protects the surrounding environment from contamination. This closed-loop design is crucial for industries where material purity and environmental safety are paramount, such as pharmaceuticals, food processing, and fine chemicals.
Key Working Scene Characteristics and Applications
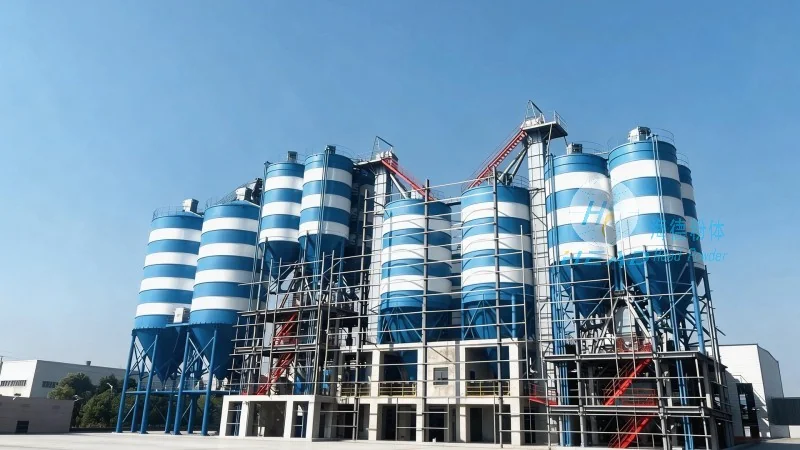
The working scene characteristics of dust-free closed material pneumatic conveying equipment are tailored to meet the diverse needs of modern industrial processes. These systems are widely used in scenarios where material handling requires high levels of cleanliness, efficiency, and safety. For instance, in pharmaceutical manufacturing, the equipment is essential for transporting active pharmaceutical ingredients (APIs) and other sensitive materials without compromising their quality or purity. The sealed environment prevents cross-contamination and ensures that the materials remain free from dust and particulate matter, which is critical for maintaining product integrity and regulatory compliance. In the food processing industry, similar applications are prevalent, where the equipment is used to convey grains, powders, and other food products in a hygienic manner. The closed system eliminates the risk of contamination from external sources, such as insects or airborne particles, and maintains the product's freshness and safety. Additionally, in the chemical industry, especially for handling hazardous or toxic powders, the dust-free design is vital for protecting both the environment and personnel. The equipment can handle a wide range of materials, including fine powders, granules, and even bulk solids, making it versatile for various operational scenarios. The working scene characteristics also include the ability to handle long-distance and high-capacity material transport, reducing the need for manual handling and improving overall operational efficiency. The systems are designed to be flexible, allowing for integration with existing production lines and adapting to different material flow rates and particle sizes. This adaptability makes them suitable for both small-scale and large-scale industrial applications, from research and development facilities to full-scale manufacturing plants.
Advantages and Considerations in Operational Scenarios
When evaluating the working scene characteristics of dust-free closed material pneumatic conveying equipment, several advantages and considerations come into play. The primary advantage is the elimination of dust emissions, which not only improves environmental sustainability but also enhances workplace safety by reducing the risk of respiratory issues and other health hazards associated with airborne particles. This is particularly important in industries where worker exposure to dust is a significant concern. Another key advantage is the high efficiency in material transport, as the sealed system minimizes material loss and ensures consistent flow rates. This leads to reduced operational costs and increased productivity. The equipment also offers flexibility in terms of material handling, as it can accommodate various particle sizes and flow rates, making it suitable for a wide range of applications. However, there are considerations to keep in mind, such as the initial investment cost, which may be higher compared to traditional open-air systems. Additionally, the maintenance requirements of the sealed components and the control systems need to be regularly monitored to ensure optimal performance. The system's energy consumption is another factor to consider, as the operation of compressed air or gas systems can be energy-intensive. Despite these considerations, the long-term benefits of improved safety, environmental compliance, and operational efficiency often outweigh the initial costs and maintenance requirements. The working scene characteristics also highlight the importance of proper system design and integration, as the effectiveness of the equipment depends on how well it is tailored to the specific material and operational needs. Proper installation, regular maintenance, and adherence to operational guidelines are essential to maximize the equipment's performance and lifespan.
Conclusion and Industry Impact
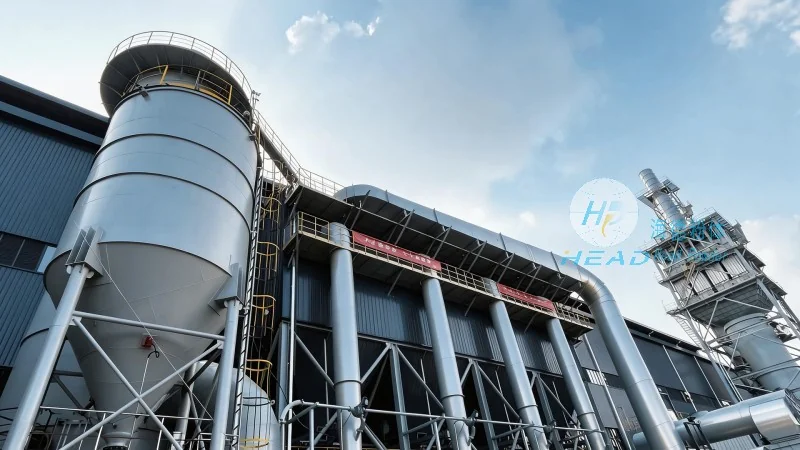
In conclusion, the dust-free closed material pneumatic conveying equipment developed by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in material handling technology. By adhering to the core principles of enclosed, efficient, and safe material transport, these systems address the evolving needs of modern industries, particularly in sectors where cleanliness, safety, and regulatory compliance are critical. The working scene characteristics demonstrate the versatility and adaptability of the equipment, making it a valuable asset for various operational scenarios. As industries continue to prioritize sustainability and operational efficiency, the demand for such advanced material handling solutions is expected to grow. The company's commitment to innovation and quality ensures that its products remain at the forefront of the industry, providing reliable and effective solutions for diverse material handling challenges. Through continuous improvement and customer-focused design, Shandong HeadPowder Engineering Co., Ltd. continues to contribute to the advancement of material handling technology, supporting the growth and success of its clients in various sectors.




