HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. Based in Shandong, China, the company has established itself as a trusted partner for industries seeking efficient and reliable material transport solutions. This article explores the core principles and operational characteristics of automatic continuous material pneumatic conveying equipment, highlighting its applications and benefits across various industrial sectors.
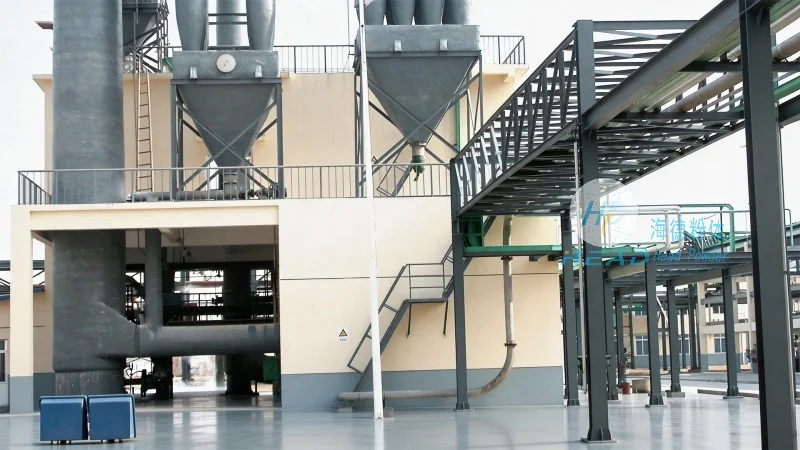
Overview of Automatic Continuous Material Pneumatic Conveying Equipment
Automatic continuous material pneumatic conveying equipment represents a sophisticated system designed to transport bulk materials in a continuous, automated manner. Unlike traditional manual or intermittent conveying methods, this technology utilizes compressed air or other gas streams to move materials through a network of pipes, ensuring seamless and unbroken material flow. The system is engineered to handle a wide range of materials, including powders, granules, and fine particles, making it versatile for diverse industrial applications.
The Working Principle of Pneumatic Conveying Systems
The fundamental principle behind pneumatic conveying is the use of air pressure to create a flow of material within a closed pipeline. In an automatic continuous system, the process begins with the material being fed into a hopper or feeder. From there, the material is introduced into the conveying line, where it is entrained by a high-velocity air stream. This air stream carries the material particles through the pipeline, maintaining a consistent flow rate and preventing material degradation or segregation. The system typically includes components such as a blower, filter, and control valves, which work in tandem to regulate air pressure, material flow, and system performance. The continuous operation ensures that material is transported without interruptions, enhancing productivity and reducing downtime in industrial processes.
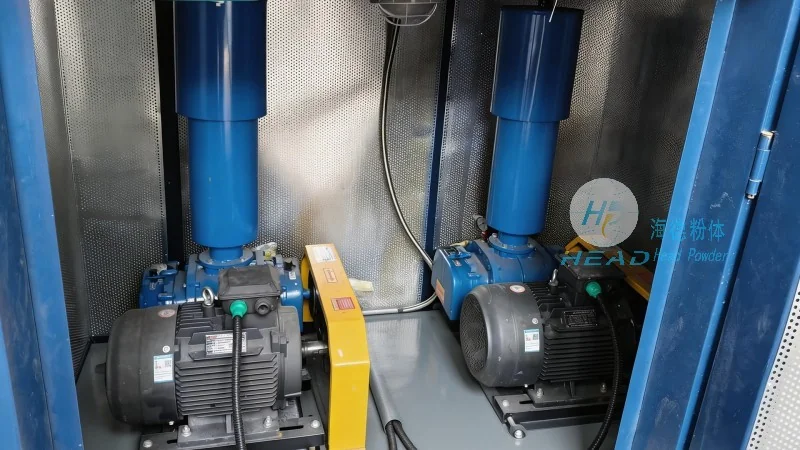
Key Working Scene Characteristics
The operational characteristics of automatic continuous material pneumatic conveying equipment are tailored to meet the demands of modern industrial environments. These systems are designed for high efficiency, with the ability to handle large volumes of material over extended periods. The continuous nature of the process minimizes the need for manual intervention, reducing labor costs and improving safety in the workplace. Additionally, the equipment is built to accommodate varying material properties, such as different particle sizes, densities, and moisture levels, ensuring adaptability across different applications. The system's compact design allows for easy integration into existing production lines, making it a practical solution for space-constrained facilities. Furthermore, the automated control features enable precise monitoring and adjustment of conveying parameters, ensuring optimal performance and material quality.
Applications and Industry Integration
Automatic continuous material pneumatic conveying equipment finds widespread application in various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical sector, the system is used to transport sensitive powders, ensuring sterile and contamination-free handling. The food industry benefits from the hygienic design of the equipment, which complies with strict regulatory standards for food safety. Chemical manufacturers utilize the system for transporting reactive or hazardous materials, where the enclosed pipeline prevents exposure and ensures safety. In mining operations, the equipment is employed to transport raw materials from storage to processing units, improving operational efficiency and reducing the risk of material spillage. The versatility of the system makes it an essential component in modern industrial operations, contributing to streamlined production and enhanced productivity.
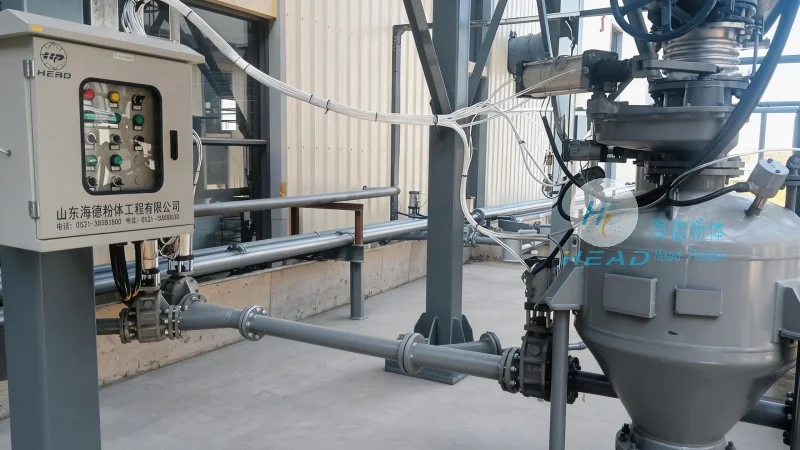
Advantages and Performance Metrics
The adoption of automatic continuous material pneumatic conveying equipment offers several key advantages over traditional conveying methods. Firstly, the continuous operation leads to higher throughput and reduced downtime, resulting in increased productivity. The system's ability to handle a wide range of materials without the need for frequent adjustments makes it cost-effective and efficient. Additionally, the enclosed pipeline design minimizes material loss and environmental contamination, aligning with sustainability goals. The automated control features provide real-time monitoring of system performance, allowing for quick adjustments to maintain optimal operation. Performance metrics such as conveying capacity, pressure drop, and energy consumption are carefully engineered to meet industry standards, ensuring reliable and consistent performance. The long-term durability of the equipment, coupled with low maintenance requirements, further enhances its economic viability for industrial applications.
Conclusion
Automatic continuous material pneumatic conveying equipment, as exemplified by the solutions offered by Shandong HeadPowder Engineering Co., Ltd., represents a cutting-edge technology in material handling. By integrating advanced principles of pneumatic transport with automated control systems, this equipment provides industries with a reliable, efficient, and versatile solution for bulk material transport. The system's adaptability to diverse material types and operational environments, combined with its ability to enhance productivity and safety, makes it an indispensable asset in modern industrial operations. As industries continue to seek innovative solutions for material handling challenges, the role of such advanced pneumatic conveying systems will only grow, driving further advancements in efficiency and sustainability.




