The phosphate fertilizer industry relies on efficient material handling solutions to ensure smooth production processes. Among the various methods available, pneumatic conveying systems have emerged as a preferred choice for transporting phosphate powder due to their versatility and effectiveness. This analysis delves into the design, functionality, and benefits of a phosphate powder pneumatic conveying system, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in providing tailored solutions for industrial applications.
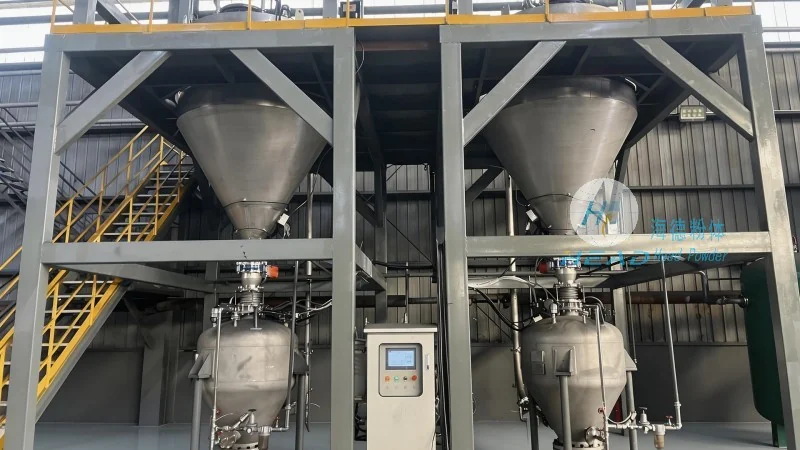
Company Introduction: HeadPowder
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the development and implementation of advanced material handling systems. With years of experience in the field, the company has built a reputation for delivering high-quality, reliable solutions that meet the specific needs of clients in the phosphate and fertilizer sectors. The company’s commitment to innovation and customer satisfaction is reflected in its comprehensive approach to system design, from initial consultation to post-installation support.
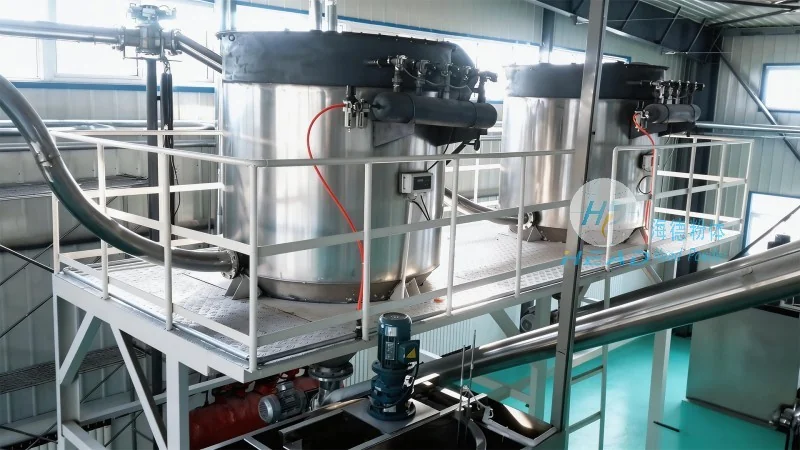
System Components and Design
A typical phosphate powder pneumatic conveying system consists of several key components that work in harmony to achieve efficient material transport. The system begins with a feed hopper or silo, which stores the phosphate powder and regulates the flow rate. This is followed by a feeder, such as a rotary valve or screw feeder, that controls the discharge of material into the conveying line. The core of the system is the conveying pipeline, which can be made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of phosphate powder. The pipeline is connected to a series of fittings, including elbows, tees, and bends, that direct the flow of powder and air. At the heart of the system is the air source, which provides the necessary pressure and volume of air to move the powder through the pipeline. This is typically a blower or compressor, equipped with controls to adjust the air flow and pressure as needed. The system also includes a control panel that monitors and regulates the operation of all components, ensuring safe and efficient operation.
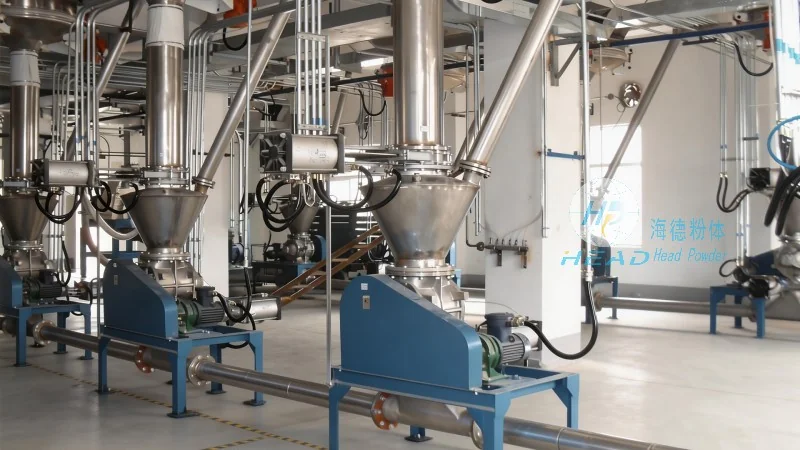
Technical Advantages and Features
One of the key advantages of pneumatic conveying systems is their ability to handle fine and abrasive materials like phosphate powder without causing excessive wear or blockages. The system uses a combination of positive and negative pressure to transport the material, allowing for both low and high-pressure applications. This flexibility makes it suitable for various distances and layouts, from short-distance transfers to long-distance pipelines. Additionally, the system is designed to minimize dust emissions, with features such as dust collection and filtration to comply with environmental regulations. The use of stainless steel components further enhances durability and resistance to corrosion, ensuring long-term performance and low maintenance costs.
Application Scenarios
Phosphate powder pneumatic conveying systems are widely used in the production of phosphate fertilizers, where they play a critical role in moving raw materials from storage to processing units. The systems are also employed in other industries, such as chemical manufacturing and food processing, where similar powder handling requirements exist. The adaptability of the system allows it to be customized to fit the specific requirements of each application, including varying material properties, flow rates, and distances. This makes it an ideal solution for both new installations and retrofitting existing facilities.
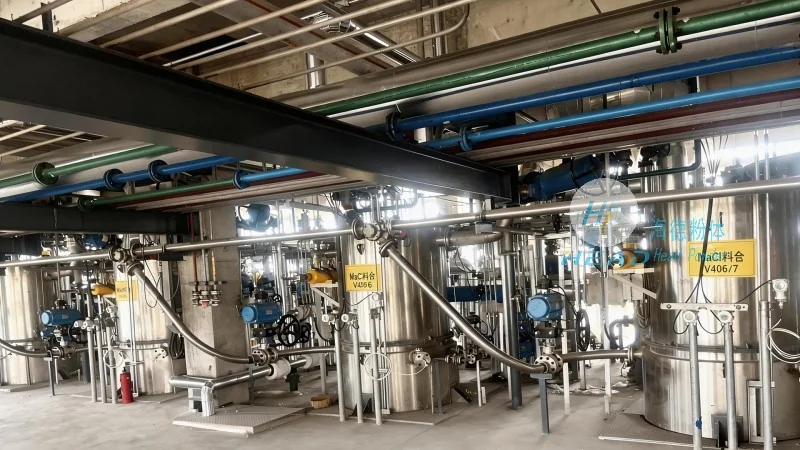
Company Strengths and Services
Shandong HeadPowder Engineering Co., Ltd. offers comprehensive services to ensure the successful implementation of phosphate powder pneumatic conveying systems. The company’s team of engineers and technicians works closely with clients to understand their unique challenges and develop tailored solutions. From system design and engineering to manufacturing and installation, HeadPowder provides end-to-end support to ensure that the system meets all operational and regulatory requirements. The company also offers maintenance and support services to ensure the long-term reliability and performance of the system. With a focus on quality and customer satisfaction, HeadPowder has become a trusted partner for businesses in the phosphate and fertilizer industry.




