Rare earth powder pneumatic conveying systems are critical in industrial applications, particularly for the efficient and safe transport of rare earth materials. Understanding the components that make up such systems is essential for optimizing performance and ensuring reliability in material handling processes. This article explores the key elements that constitute a typical rare earth powder pneumatic conveying system, highlighting the role of each component in the overall operation.
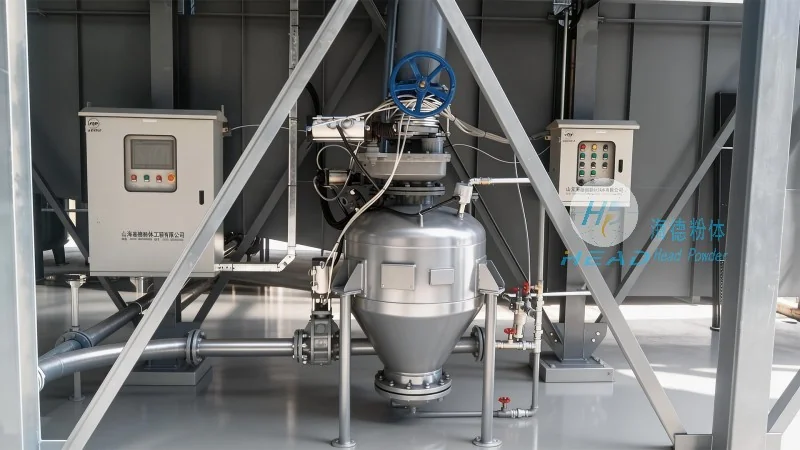
Key Components of Rare Earth Powder Pneumatic Conveying Systems
The core components of a rare earth powder pneumatic conveying system are designed to work in concert to facilitate the movement of fine powders like rare earth compounds. These components include the air supply system, conveying lines, material feeders, separation and filtration units, and control mechanisms. Each of these elements plays a vital role in maintaining the integrity of the powder and ensuring efficient transport.
The Air Supply System
The air supply system is the heart of any pneumatic conveying setup. It typically consists of a blower or compressor that generates the necessary airflow to move the powder particles through the system. For rare earth powders, which are often fine and can be sensitive to air flow, the air supply system must be capable of delivering consistent pressure and volume. This ensures that the powder is entrained effectively and transported without degradation or loss. The system may also include air filters and regulators to maintain air quality and pressure stability, which are crucial for preventing contamination and system inefficiencies.
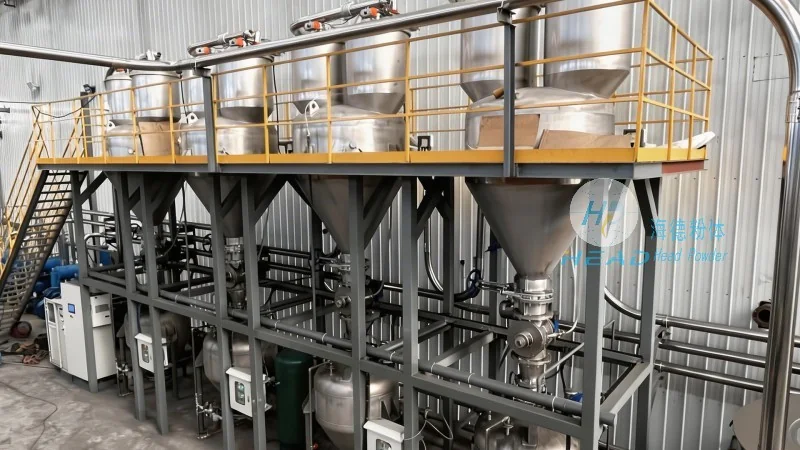
Conveying Lines and Pipework
Conveying lines, usually made of materials like stainless steel or plastic, form the pathway through which the rare earth powder is transported. The choice of material for the pipework is critical, as rare earth powders can be abrasive and may contain corrosive components. Stainless steel is commonly used due to its durability and resistance to corrosion, while plastic pipes are sometimes employed for non-corrosive applications or to minimize friction. The design of the pipework, including bends, elbows, and straight sections, is optimized to minimize pressure drop and maintain consistent flow rates. Properly sized and configured lines are essential to prevent blockages and ensure smooth material transport.
Material Feeders and Inlet Devices
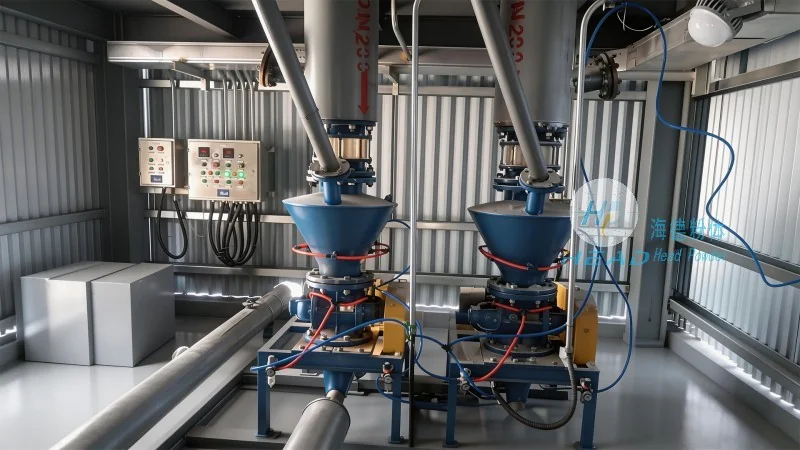
Material feeders are responsible for introducing the rare earth powder into the conveying system at a controlled rate. This component is vital to maintain a steady flow of material and prevent overloading or underloading of the system. Common types of feeders include rotary valves, screw feeders, and vibratory feeders. For rare earth powders, which can be cohesive or have variable flow properties, the selection of an appropriate feeder is critical. The feeder must be able to handle the specific characteristics of the powder, such as its density, moisture content, and particle size distribution. Proper feeding ensures that the powder is introduced smoothly into the air stream, avoiding issues like bridging or clogging at the inlet.
Separation and Filtration Units
As the rare earth powder travels through the system, it may need to be separated from the air stream at the end of the conveying process. Separation units, such as cyclones or bag filters, are used to collect the powder and return it to the process or storage. These units are designed to capture fine particles efficiently while allowing clean air to be discharged. For rare earth powders, which may have health or environmental implications if released into the atmosphere, the filtration system must meet stringent standards. The separation and filtration components are essential for maintaining product quality, preventing environmental contamination, and ensuring compliance with regulatory requirements.
Control and Monitoring Systems
Modern rare earth powder pneumatic conveying systems often incorporate advanced control and monitoring systems to optimize performance and ensure safety. These systems may include pressure sensors, flow meters, and programmable logic controllers (PLCs) that monitor key parameters such as air pressure, flow rate, and material level. The control system allows for real-time adjustments to the operation, ensuring that the system operates within optimal parameters. This not only improves efficiency but also helps in detecting and addressing issues before they lead to system failures or material loss. The integration of automation and monitoring technologies enhances the reliability and longevity of the conveying system.
Role of Shandong HeadPowder Engineering Co., Ltd.
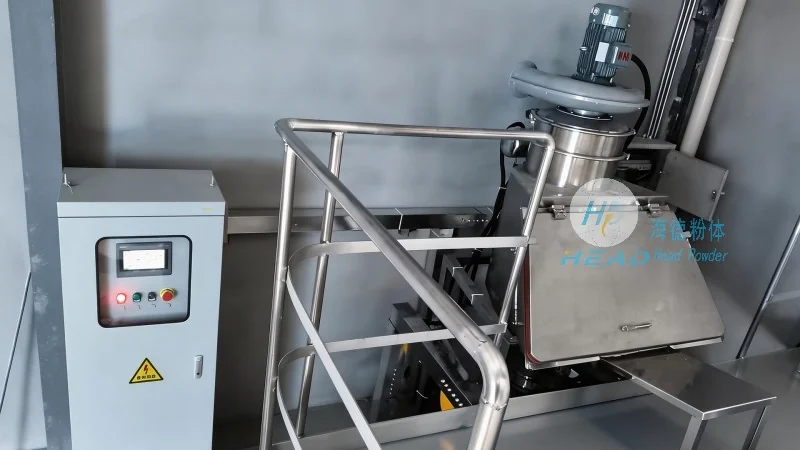
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and integration of pneumatic conveying systems for various industrial applications, including those involving rare earth powders. With a focus on precision engineering and material handling expertise, headpowder provides comprehensive solutions tailored to the unique requirements of rare earth powder transport. The company’s expertise lies in understanding the specific challenges associated with handling fine, abrasive, and potentially hazardous powders, and designing systems that address these challenges effectively. By leveraging advanced materials, engineering principles, and industry best practices, headpowder ensures that its pneumatic conveying systems deliver reliable performance, high efficiency, and long service life. The company’s commitment to quality and customer satisfaction is reflected in its ability to provide customized solutions that meet the exact needs of clients in the rare earth industry.
Conclusion
In summary, a rare earth powder pneumatic conveying system comprises several critical components, each playing a specific role in the efficient and safe transport of the material. From the air supply system to the separation and filtration units, every element is designed to work together to achieve optimal performance. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd. is crucial in developing and implementing these systems, ensuring that they meet the stringent requirements of the rare earth industry. By understanding the components and their functions, industries can enhance their material handling processes, improve operational efficiency, and ensure compliance with safety and environmental standards.




