Gravity dust removal and pneumatic conveying systems represent a critical technology in industrial material handling, particularly for the efficient transport of fine powders and dust particles. These systems are designed to combine dust collection with the pneumatic transport of materials, offering a compact and effective solution for various industrial applications. The equipment, often referred to as a gravity dust removal pneumatic conveying system, is a specialized device that integrates dust filtration and material transport in a single unit, enhancing operational efficiency and reducing the need for separate equipment.
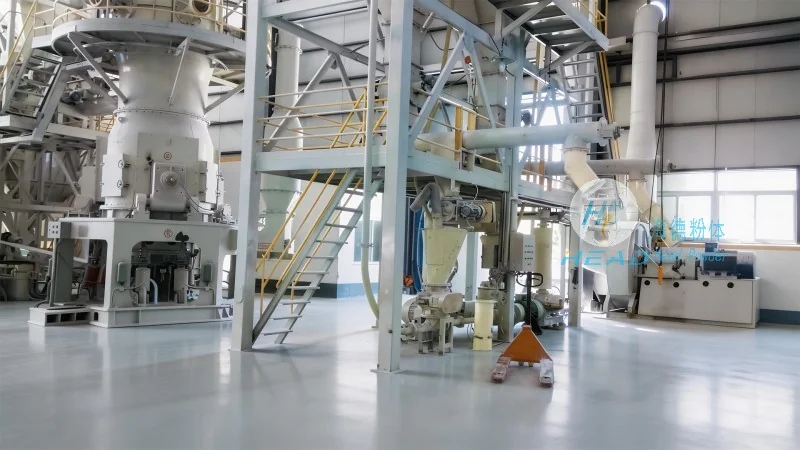
Understanding the Gravity Dust Removal Pneumatic Conveying System
At the core of this system is the ability to capture airborne dust particles while simultaneously conveying the material to its destination. The system typically operates by using a combination of gravity and air pressure to move the material through a pipeline. The design incorporates dust filters, often with high-efficiency particulate air (HEPA) or similar filtration media, to ensure that the emitted air is clean and compliant with environmental regulations. This dual functionality makes the system particularly valuable in industries such as pharmaceuticals, food processing, and chemical manufacturing, where both material handling and air quality are paramount.
Key Components and Design Principles
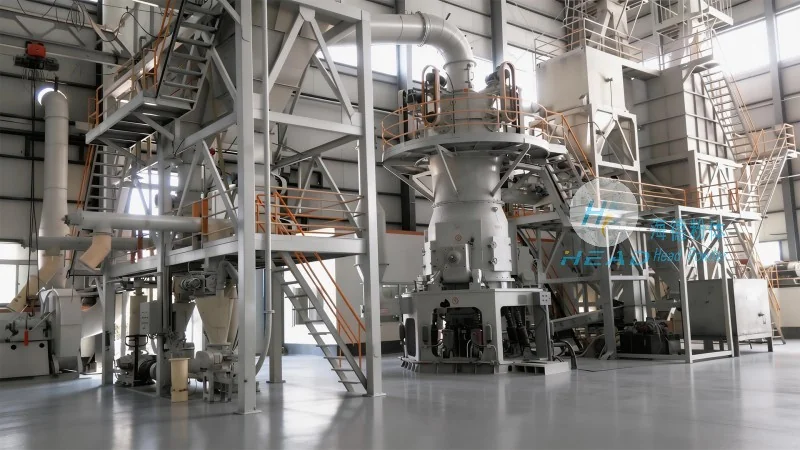
The gravity dust removal pneumatic conveying system is composed of several key components, each playing a vital role in its operation. The primary components include a dust collection hopper, a conveying pipeline, a fan or blower to generate airflow, and a filter system. The design principle revolves around the use of gravitational forces to assist in the movement of material, reducing the energy consumption compared to traditional pneumatic conveying systems that rely solely on air pressure. The system is engineered to handle a wide range of particle sizes and material densities, making it versatile for different industrial needs.
How the System Works: A Step-by-Step Explanation
When material is introduced into the dust collection hopper, it falls under gravity into the conveying pipeline. Simultaneously, the fan or blower creates a low-pressure zone in the pipeline, drawing the material along with the air flow. The air and material mixture travels through the pipeline to the destination point, where the material is discharged. The filter system, positioned at the inlet or outlet of the system, captures the dust particles from the air stream, ensuring that the emitted air is clean. This process is continuous, allowing for a steady flow of material while maintaining air quality standards.
Advantages of the Gravity Dust Removal Pneumatic Conveying System
One of the significant advantages of this system is its ability to reduce energy consumption compared to conventional pneumatic conveying systems. By utilizing gravity to assist in material movement, the system requires less air pressure, leading to lower operational costs. Additionally, the integrated dust removal feature eliminates the need for separate dust collection equipment, saving space and reducing maintenance efforts. The system also offers high material handling capacity, making it suitable for large-scale industrial operations. Furthermore, the compact design allows for easy installation in existing facilities, minimizing disruption to ongoing production.
Applications and Industries
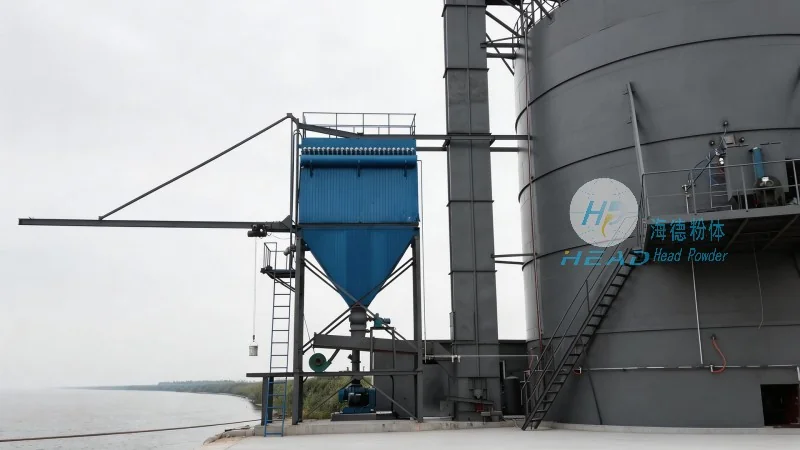
The gravity dust removal pneumatic conveying system is widely used across various industries due to its versatility and efficiency. In the pharmaceutical industry, it is used to transport fine powders while maintaining sterile and dust-free conditions. In food processing, it ensures that the material is handled hygienically and without contamination. The chemical industry also benefits from this system, as it can handle a variety of chemical powders while preventing dust emissions. Other applications include the cement and construction industries, where it is used for transporting bulk materials with minimal dust generation.
Conclusion and Company Overview
Gravity dust removal pneumatic conveying systems are an essential technology for modern industrial material handling, offering a cost-effective and efficient solution for transporting fine powders while maintaining air quality. The design principles, which combine gravity and air pressure, make these systems versatile and adaptable to various industrial needs. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in manufacturing and supplying high-quality gravity dust removal pneumatic conveying systems. With a focus on innovation and customer satisfaction, the company ensures that its products meet the highest standards of performance and reliability. Based in Shandong, China, HeadPowder Engineering Co., Ltd. leverages its expertise to deliver tailored solutions that address the specific needs of industrial clients, contributing to improved operational efficiency and environmental compliance.




