For industries dealing with food-grade salt, efficient and reliable powder handling is crucial. A food grade salt powder conveying system is a specialized setup designed to transport salt powder from storage to processing or packaging areas while maintaining hygiene and safety standards. This system is essential for ensuring consistent product quality and operational efficiency in food processing facilities.
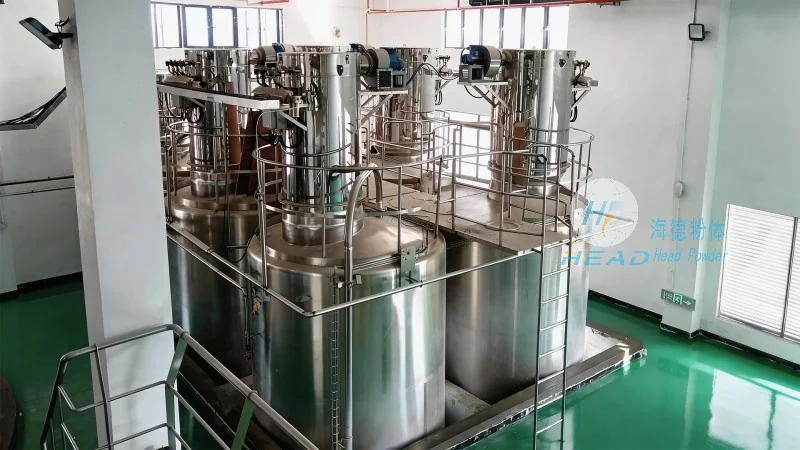
Key Components of the Conveying System
The core components of a food grade salt powder conveying system typically include hoppers, feeders, conveyors, and control systems. Hoppers are used to store the salt powder, providing a controlled feed to the feeder. The feeder regulates the flow of powder into the conveyor, ensuring a consistent and controlled discharge rate. Conveyors, such as pneumatic or mechanical types, transport the salt powder through the system. Control systems monitor and adjust the operation of these components to maintain optimal performance.
Design Principles for Efficient Operation
Designing a food grade salt powder conveying system involves several key principles to ensure efficiency and reliability. First, the system must be constructed from materials that are compatible with food-grade applications, such as stainless steel, to prevent contamination and ensure durability. Second, the system should be designed to minimize dust generation and maintain a clean environment, as salt dust can affect product quality and worker health. Third, the system must be equipped with proper sealing and cleaning mechanisms to prevent cross-contamination and maintain hygiene standards. Additionally, the system should be designed for easy maintenance and cleaning, which is critical for food processing environments where sanitation is paramount.
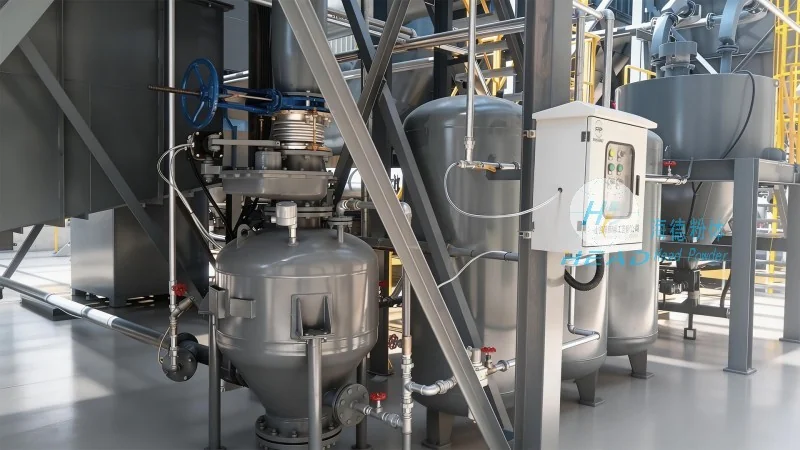
How the System Works: A Step-by-Step Overview
The operation of a food grade salt powder conveying system generally follows a sequence of steps. First, the salt powder is stored in the hopper. The feeder then regulates the flow of powder from the hopper into the conveyor. The conveyor transports the powder to the processing or packaging area. Control systems monitor the flow rate and pressure, ensuring the system operates smoothly. If any issues arise, such as blockages or pressure changes, the control system can trigger alarms or adjustments to prevent system failure.
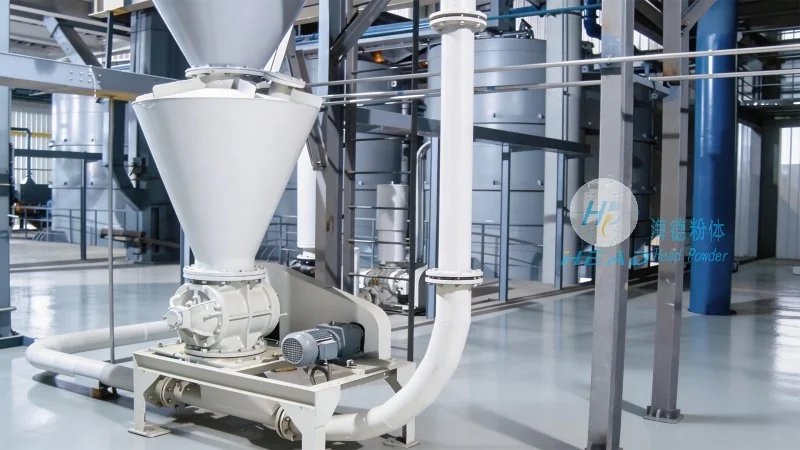
Benefits of Using a Food Grade Salt Powder Conveying System
Implementing a food grade salt powder conveying system offers several benefits for food processing facilities. Firstly, it improves operational efficiency by automating the powder handling process, reducing labor costs and increasing throughput. Secondly, it enhances product quality by maintaining consistent flow rates and preventing contamination. Thirdly, it improves safety by reducing manual handling of salt powder, minimizing the risk of dust exposure and accidents. Finally, it ensures compliance with food safety regulations, which is essential for maintaining market access and customer trust.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of specialized powder handling equipment, including food grade salt powder conveying systems. With years of experience in the industry, the company has developed a reputation for producing high-quality, reliable, and efficient systems that meet the stringent requirements of food processing applications. The company's facilities are located in Shandong, China, where it employs skilled engineers and technicians to design, manufacture, and test its products. Shandong HeadPowder Engineering Co., Ltd. is committed to providing innovative solutions that enhance the performance and safety of food processing operations worldwide.




